
Your Choice Of The Most Difficult Ordinary Model-engineering Operation?

Your Choice Of The Most Difficult Ordinary Model-engineering Operation?

Home › Forums › The Tea Room › Your Choice Of The Most Difficult Ordinary Model-engineering Operation?

Viewing 20 posts - 26 through 45 (of 45 total)
  • Author
    Posts
  • #829347
    Diogenes
    Participant
      @diogenes

      Skew gears are an interesting subject- please do share your experiences, er when you experience them..

      #829391
      Nigel Graham 2
      Participant
        @nigelgraham2

        Thankyou Julie, for the encouragement.

        I am part way through re-commissioning a small, ancient Denbigh H4 Horizontal Mill, and gear-cutting is one of my possible uses for it.

        I do have a dividing-head and rotary-tables; and in the last resort of course it’s not difficult to make a divider based on borrowing change-wheels from one of my lathes.

        Its table-feed is missing (or was never fitted) but the worm-wheel under the table is there, and I might be able to make a replacement worm, from mild-steel (I’ve never going to wear it out!). I think I managed to find how to calculate the pitch though have to assume the pressure-angle. If I have the change-wheels for the peculiar number, I think the Harrison L5 lathe with its 1/4″ lead should cope with it, with care.

        A full worm and wheel is another matter though.


        As for the hobby taking over the house, I think my model-engineering is the householder and I, the lodger! Even going to and from my computer in the corner of the front room involves avoiding falling over a 7.1/4″g loco awaiting repairs.

        #829394
        Dave Halford
        Participant
          @davehalford22513
          #829399
          old mart
          Participant
            @oldmart

            I found that silver soldering brass hinges onto brass tubes which had a wall thickness of 0.010″ with oxy acetylene using the smallest available nozzle size. The tubes were about 2″ diameter and needed great care not to burn a hole in the tube wall.

            #829414
            SillyOldDuffer
            Moderator
              @sillyoldduffer

              Design.  Anything complicated that’s outside one’s experience, can’t be copied, and has to satisfy a need is difficult.   Especially if it has to be delivered to time and budget.

              Dave


              #829429
              Nigel Graham 2
              Participant
                @nigelgraham2

                Dave H –

                Thankyou.

                That’s no more than 0.006″, but I think I had a gap larger than that.

                The difficulty part is drilling a hole slightly oversize hole but not too much.


                Dave (SOD) –

                Tell me about it! It’s hard enough from a few old and rather inconsistent photos and dimensions from contemporary trade advertisements!

                #829446
                bernard towers
                Participant
                  @bernardtowers37738

                  Old Mart if you use excess oxygen it reduces the temperature of the flame, that might help. By the way you know if you have excess oxygen as the flame gets noisy.

                  #829465
                  Julie Ann
                  Participant
                    @julieann
                    #829466
                    Julie Ann
                    Participant
                      @julieann
                      #829481
                      jaCK Hobson
                      Participant
                        @jackhobson50760

                        Keeping calm after making the mistake… then fixing it without scrapping the part.

                        #829482
                        jaCK Hobson
                        Participant
                          @jackhobson50760

                          Set-up, or the subset: work-holding.

                          #829483
                          jaCK Hobson
                          Participant
                            @jackhobson50760

                            Many jobs are easy when done right… but easy to do wrong.

                            #829484
                            mike T
                            Participant
                              @miket56243

                              Doing up a left hand thread, nut and bolt. My spanners are pre-programmed to turn the wrong way.

                              Mike

                              #829488
                              Charles Lamont
                              Participant
                                @charleslamont71117
                                #829498
                                old mart
                                Participant
                                  @oldmart

                                  Bernerd, the excess acetylene reducing the flame temperature was exactly what helped with the thin wall brass tube, I am unlikely to do anything like that again, it was about 45 years ago.

                                  #829499
                                  Speedy Builder5
                                  Participant
                                    @speedybuilder5

                                    Fat Fingers  and shakey hands!

                                    Bob

                                    #829500
                                    howardb
                                    Participant
                                      @howardb
                                      #829518
                                      Nigel Graham 2
                                      Participant
                                        @nigelgraham2

                                        Julie –

                                        Well, yes, “in theory”!

                                        I measured the wheel as best I could without a proper gear-tooth micrometer, and determined its most likely form from the chapter on worm-gear in Ivan Law’s book. He gives a table of pitches, but still leaves you to try to calculate the blank diameter and depth of cut.

                                        The circular pitch is 0.2618, giving 3.8197 TPI.

                                        A lot of juggling of vulgar-fractions, the five-times-table and 127 gave me approximations I narrowed to [0.25 X (127 / 100) X (70 / 85) ] = 0.2615″ pitch!

                                        3.8241 TPI.

                                        Near enough, I suppose, over barely 4 or 5 turns. I don’t think there are any tenths of thous in my workshop anyway…. Still, this is to replace manually operating a feed-screw with a short handle, at very low speed, so not much torque and load.


                                        I’ve only to ascertain I have those change-wheels: I am pretty sure I do.


                                        The lathe should handle that although the manual does warn that trying to cut threads coarser than the leadscrew requires considerable care. It will amble round at about 60-70 rpm, and nice shallow cuts should be all right. Remembering I cannot use the half-nut release and thread dial indicator for an irrational-number pitch.

                                        I have built a Hemingway Kits ‘Worden’ T&C Grinder so have no excuse for not forming the finishing-tool to the correct angle, or very closely so.


                                        Ivan Law does give a method for calculating peculiar ratios to very high accuracy by a sort of extended long-division series, but I cannot make head nor tail of it! I simply use a calculator or spreadsheet to make successive approximations with the change-wheels I have, to find the best match.

                                        #829671
                                        Julie Ann
                                        Participant
                                          @julieann
                                          #829683
                                          Nigel Graham 2
                                          Participant
                                            @nigelgraham2

                                            Well, I’ve sorted both problems…

                                            Hopefully.

                                            I have made a new pipe assembly, but used a slightly unconventional approach. The two union nipples are of the flat-face type.

                                            The pipe is for a boiler pressure-gauge moved to a lower position for visibility, on a bracket on the bunker to one side of the boiler. This is part of modifications to aid driving the loco, a Ken Swan 1/3 version of the Kerr-Stuart ‘Wren’, on a ground-level track. (I made my feelings very well known when other club members suggested hacking big ‘oles in the cab roof, having been one of the original builders!)

                                            I ascertained first that the two 1/8″ BSP union nuts could be accommodated loosely, behind the 3-jaw chuck’s jaws.

                                            Rather than turning the two connectors complete, I pilot-drilled them about 1/16″ or so through, then drilled the stop-ended hole for the pipe, turned the body and flange outside diameters, parted off.

                                            I had estimated the pipe’s length from the formed first attempt, with a generous allowance for the siphon, but left it straight so far. Putting it in the lathe I used a file to reduce its o.d. at each end very slightly, to slide-fit the nipples.

                                            Then cleaned all the parts thoroughly and this time worked the 455-grade silver-solder paste into each fitting before inserting the tube…. ensuring the two nuts were on and facing the right way before fitting the second!

                                            ‘Tippex’ all over the nipples. I read the label to ensure it is the solvent not aqueous type, before actually taking it to the Co-op counter.

                                            The cartridge-gas plumber’s blowlamp I use gives plenty of heat.

                                            Cleaned and pickled the assembly – this time it looks sound but I ought still give it a hydraulic test before fitting it to the loco. There is some other work on that first anyway.

                                            Put the assembly in the lathe, faced the parted ends, drilled for the connection spigot on the gauge and banjo connection. I made the banjo from solid.

                                            Only now formed the pipe to a close match to the first attempt: I won’t be able to finish that until I can get back to the loco itself. I use a small pliers-action, 3-diameter pipe bender for such work.

                                            ….. So fingers crossed!


                                            ………


                                            The other tale of two troubles was how to turn a worm – encouraged on this thread(!) by Julie.

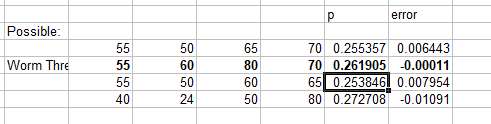
                                            I calculated the gearing for my Harrison L5 lathe supposedly giving a pitch within a few thou of right. Then a stock-take this afternoon revealed I don’t have 3 of those 4 change-wheels as I had thought, so back to the PC, wind up ‘Excel’ and start again.

                                            This time, I found a sensible combination even closer, using the wheels I do have!

                                            worm p = 0.2618″. leadscrew 0.25″

                                            0.25 X 55/60 X 80/70 = 0.2619″.

                                            Can’t really argue with that.

                                            This snippet gives part of the operation. The spreadsheet is not as elegant as it might be, but it works. The working is actually on another part of the page, and I copy the values to this little table which derives the error as [0.2618-(formula result)].

                                            Screenshot 2025-12-22 182539

                                            (I learnt to drive ‘Excel’, ‘Word’ and MS-Win-assorted at work, where I became quite familiar with making arithmetical spreadsheets complete with graphs, to a modest level of maths. There is nothing magic with the method here though, just plugging estimated tooth-counts from the list into the ‘Excel-ese’ version of the standard change-wheel formula, until hitting the best selection. )


                                          Viewing 20 posts - 26 through 45 (of 45 total)
                                          • Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.

                                          Latest Replies

                                          Home › Forums › The Tea Room › Topics

                                          Viewing 25 topics - 1 through 25 (of 25 total)
                                          Viewing 25 topics - 1 through 25 (of 25 total)

                                          View full reply list.