
Liney RV-2 Rescue

Liney RV-2 Rescue

Home › Forums › Stationary engines › Liney RV-2 Rescue

Viewing 9 posts - 1 through 9 (of 9 total)
  • Author
    Posts
  • #868134
    JasonB
    Moderator
      @jasonb

      I got an email a few weeks ago from an internet friend asking if I wanted a part built engine that he had going spare. Now I use the word “Friend” in the broadest terms, as I don’t think a real friend would have dared to give me an engine with so many interesting additional machining features that the original builder had included, but it certainly turned out to be the gift that kept on giving in that respect.😂

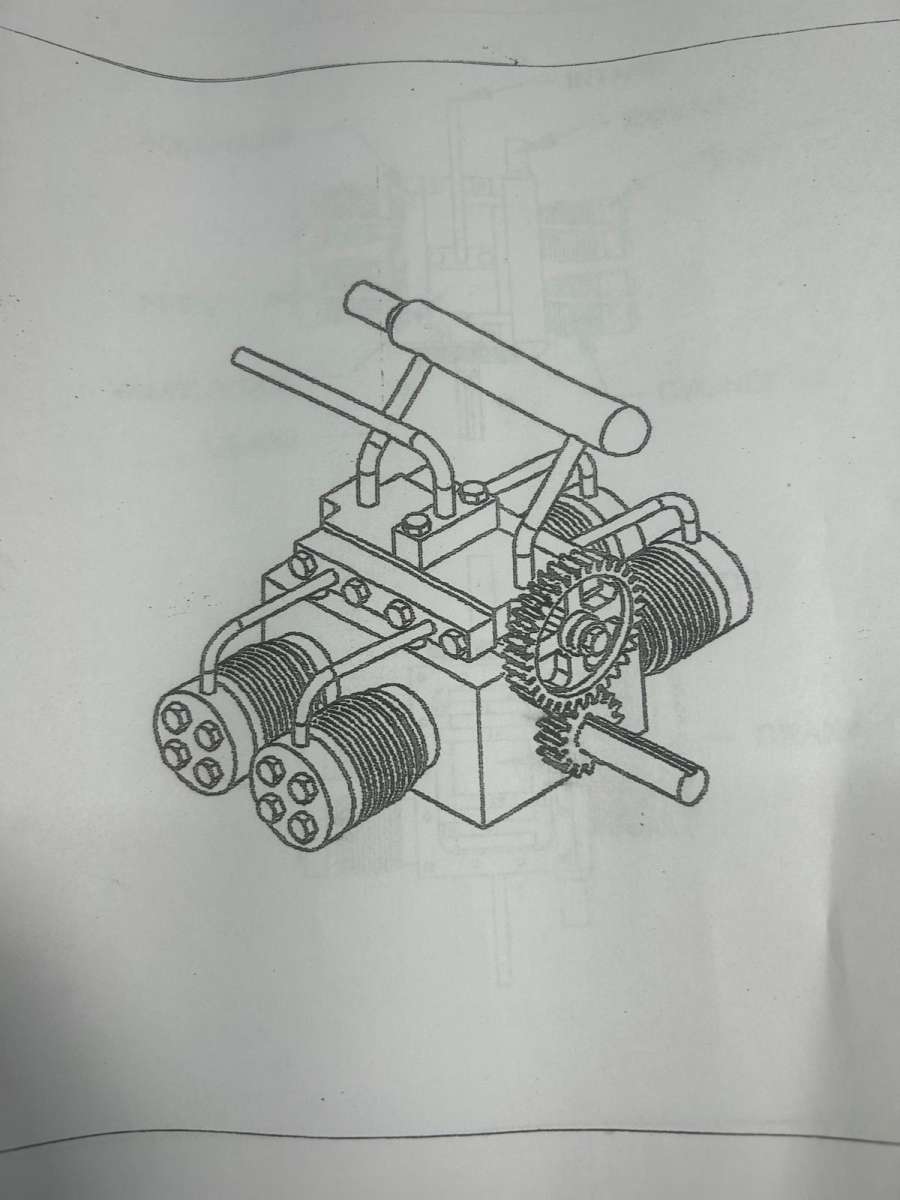
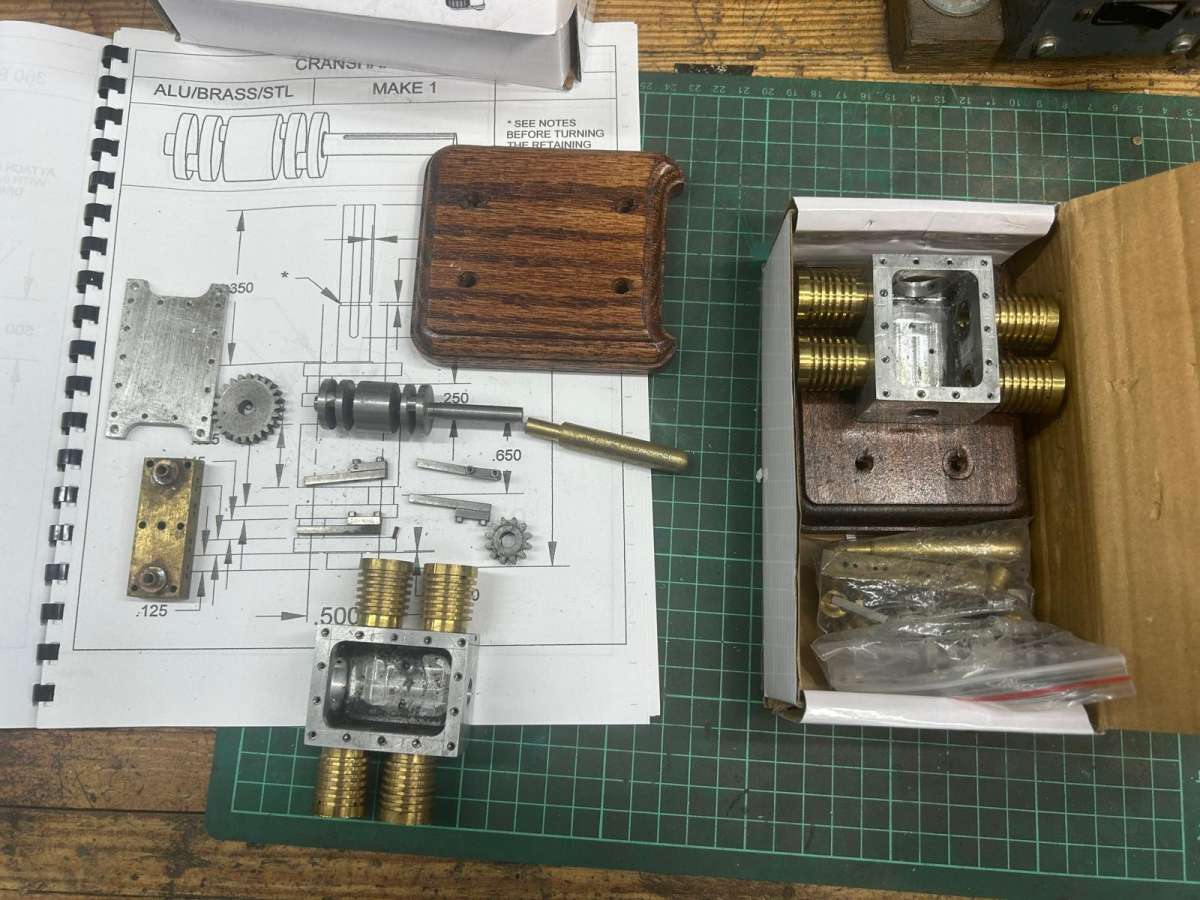
      His email included a couple of images of the drawings which did not have the engine name or who designed it as well as some images of what he had. The story is that a friend of his bought them from a guy in America who had started to build ten engines and as they were cheap he got two for my friend, I subsequently found out why they were so cheap – almost expensive scrap.

      WhatsApp Image 2026-09-08 at 16.22.18

      WhatsApp Image 2026-09-08 at 16.22.19 (2)

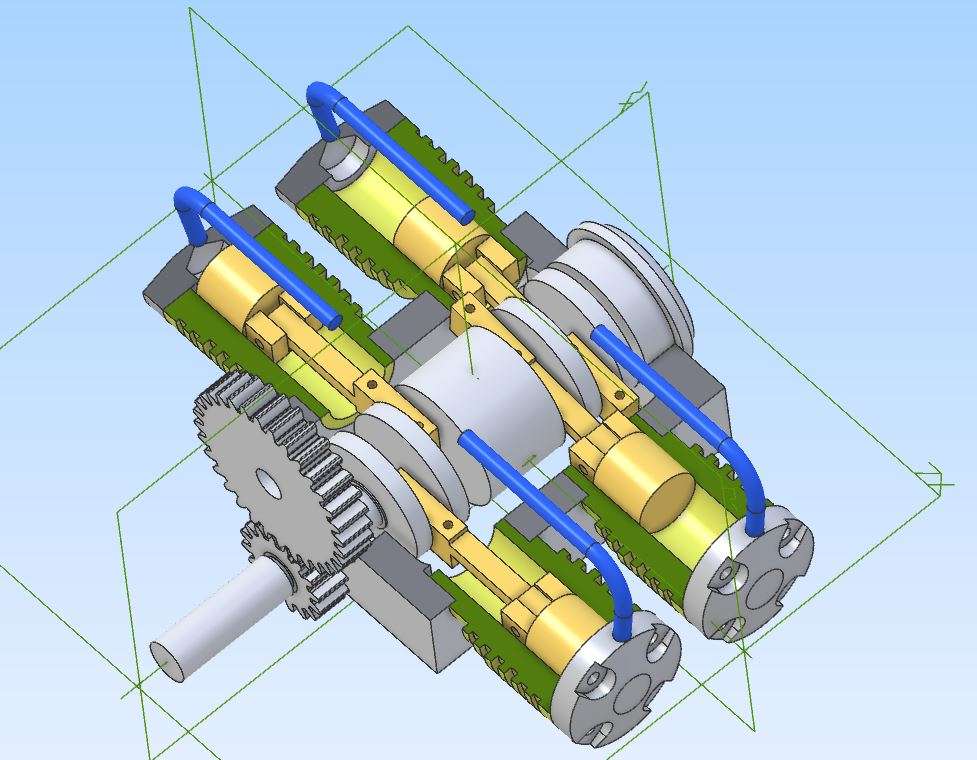
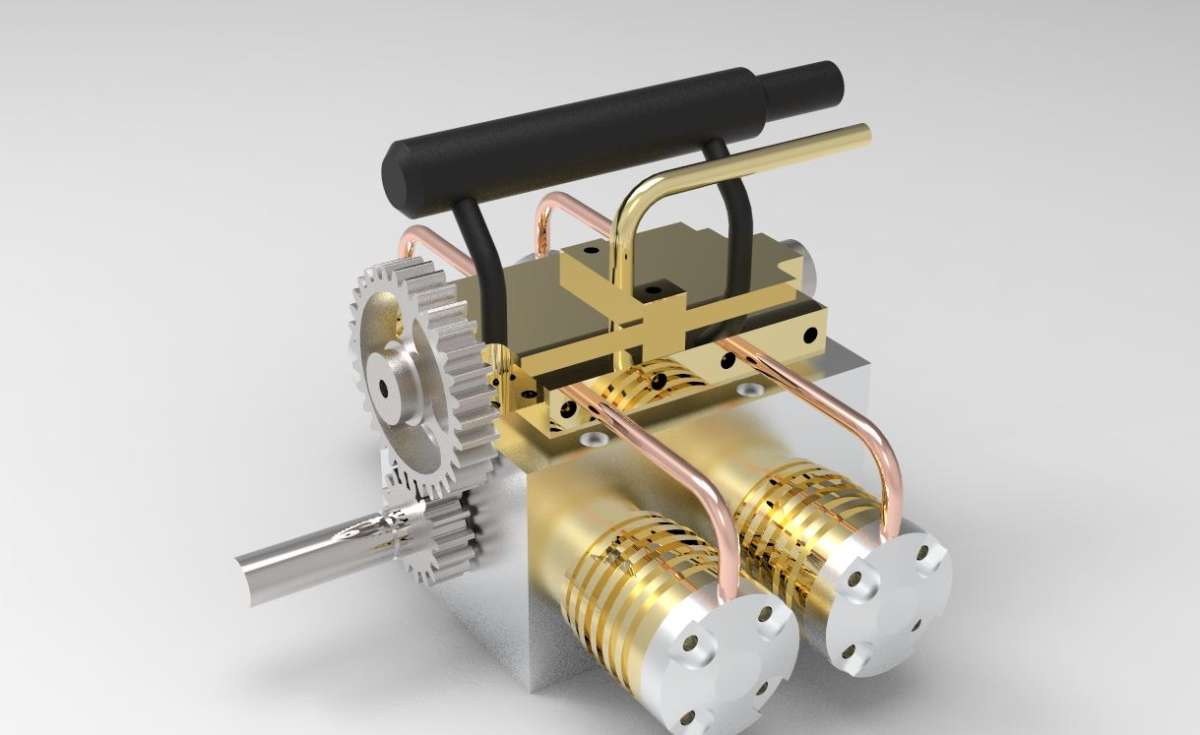
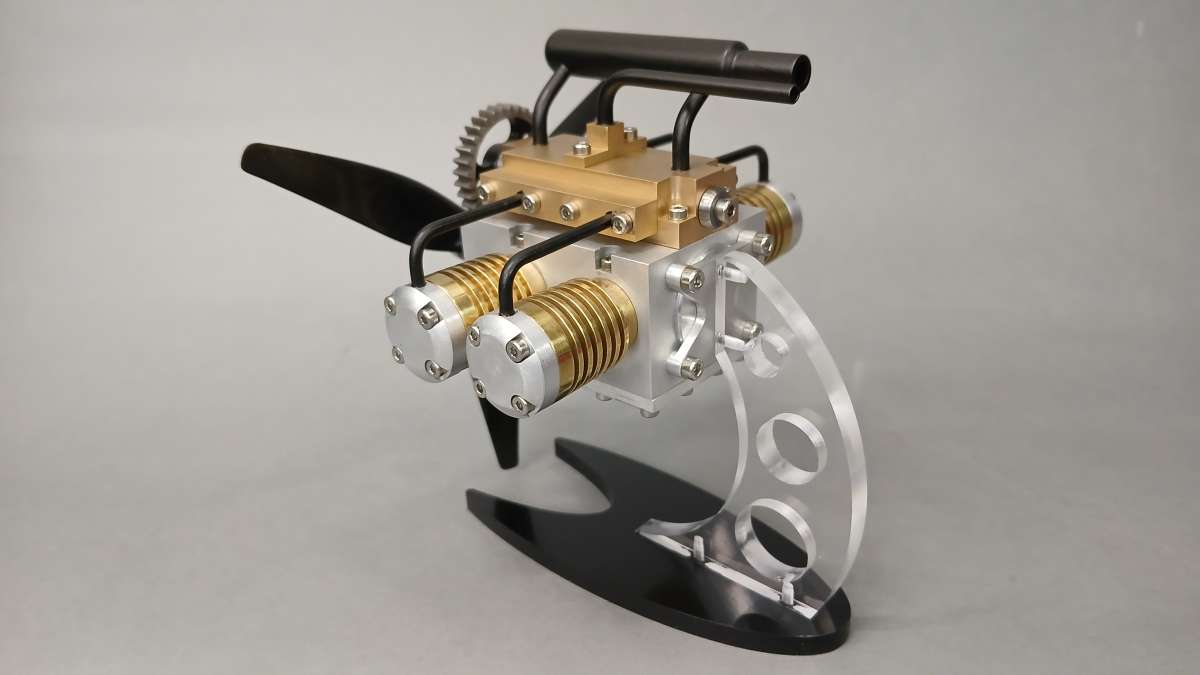
      The style of engine reminded me of the Liney “Halo” and after some googling and asking on an American forum it was confirmed that the engine was the Liney RV-2. A flat four boxer air (or steam) engine of 3/8″ bore and 1/2″ stroke. As soon as the drawings arrived, I redrew them in Alibre to see if all was OK, I just made one change to the pipe positions that come out the central manifold so that they were not offset from the cylinder ctr lines. Apart from that it all looked like it should work. Although imperial the drawings were in decimals and not fractions with many sizes being in multiples of 25, 50 and 100 thou which I have seen a couple of times on other American drawings and quite easy to work with.

      Boxy 2

      Boxy 4

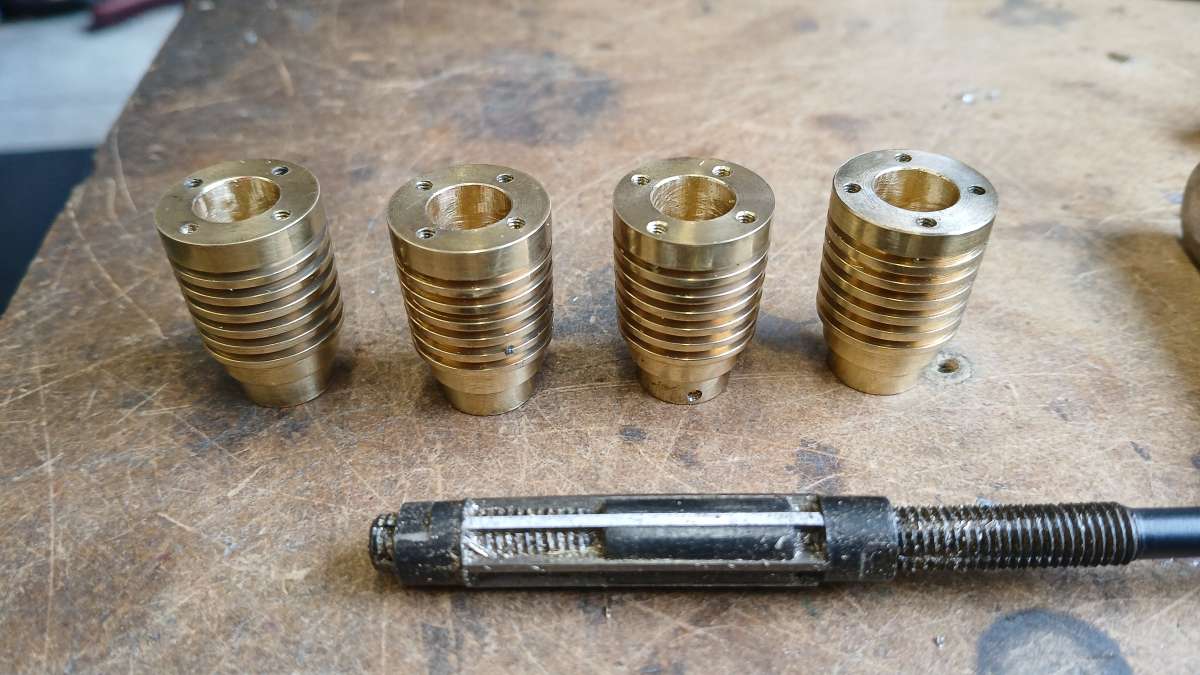
      The voyage of discovery started when I took the engine parts down to the workshop. Starting with the cylinders which looked quite nicely machined on the outside it soon turned out that their spigots to locate them in teh crankcase were a bit small and varied bt I can take care of that on final assembly. A bigger problem was the bores which again varied by a thou or two but worse was that they were all tapered and a piece of 3/8″ silever steel would only enter so far into each but by different amounts. Luckily I had an expanding reamer to suit that range of sizes so worked my way through all 4 cylinders, slowly increasing the bore until all four were cutting full length. The bore ended up approx 9.75mm.

      20260915_141554

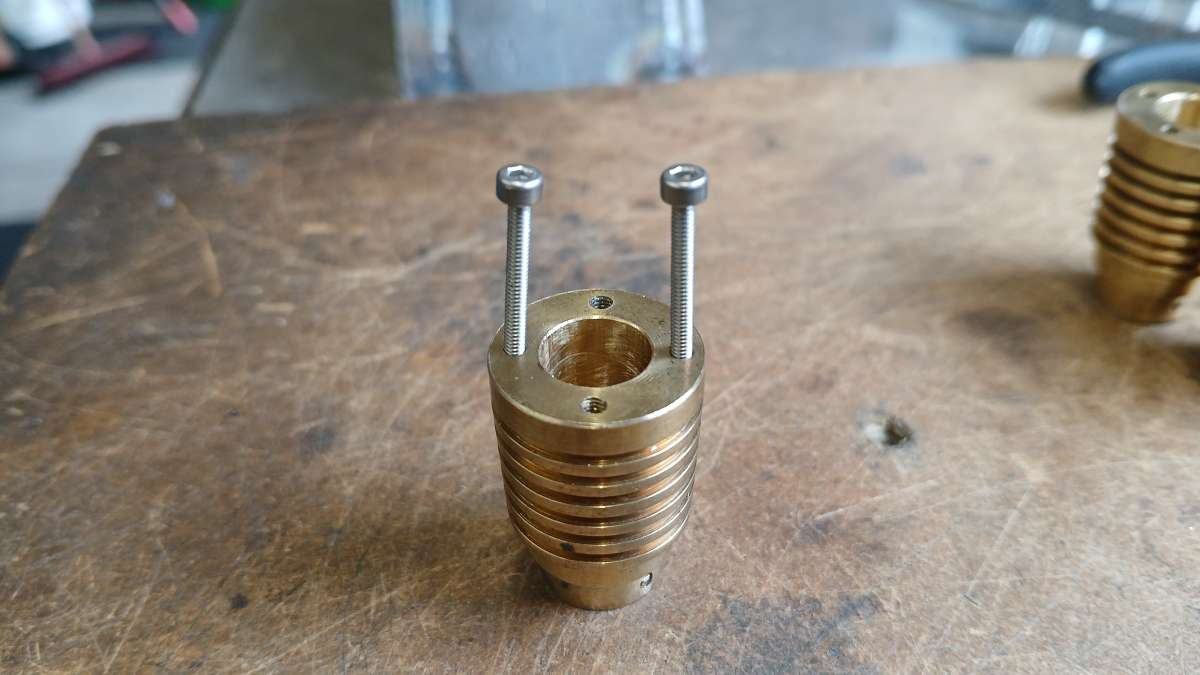
      The drawings spec UNC threads throughout the engine mostly #2-56 and #0-80 but I prefer metrix so thought I would be able to rethread the holes for the cylinder head screws M2.5, it was only when I tried a screw in teh existing threads that I discovered many were crooked.

      20260915_141644

      To cure that I decided to drill and tap new holes placed between the old ones and take the opportunity to go down a size to M2

      20260915_143850

      Offering up the sump plate to the crankcase I first thought that the sump was too narrow but after  a qick going over with the digi callipers it turned out that the crankcase was 2 1/16″ wide not the 2″ called for on the drawings. So after re-tapping all the sump screw holes to metric, it was screwed to the crankcase and the case taken down to width, just skimming the sump at the same time. I then did all the other external faces as the previous builder had polished it up with a buffing wheel, judging by the muck still in the case and it was all a bit rounded over for my liking as well as being too shiny.

      20260916_141542

      I also got rid of the foot mounting lugs on the sump as I wanted to use the optional rear mount shown in the drawings

      20260916_144759

      I thought I was done with the crankcase but there were some more surprises to come!


      #868342
      JasonB
      Moderator
        @jasonb

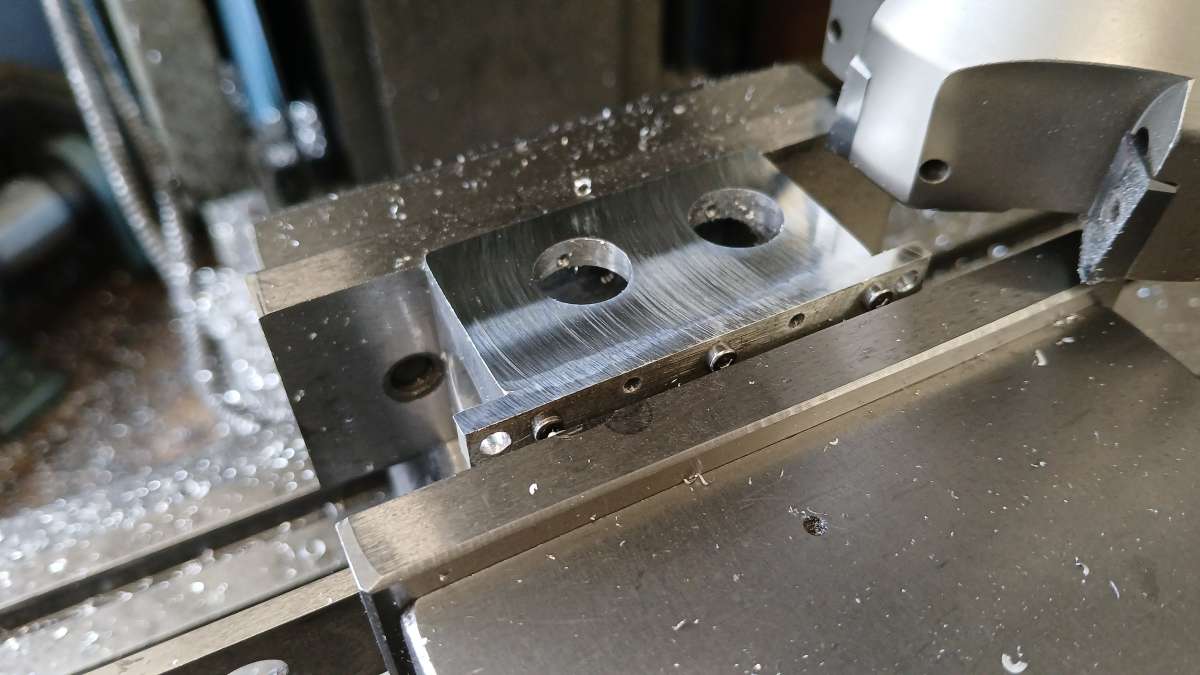
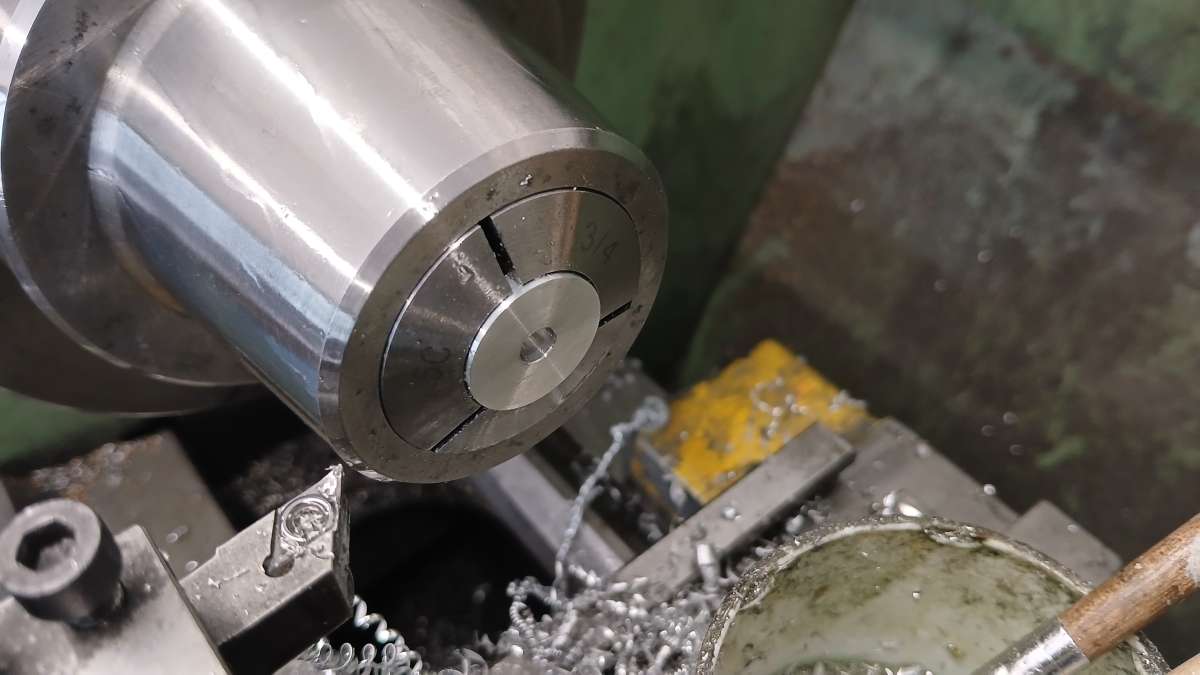
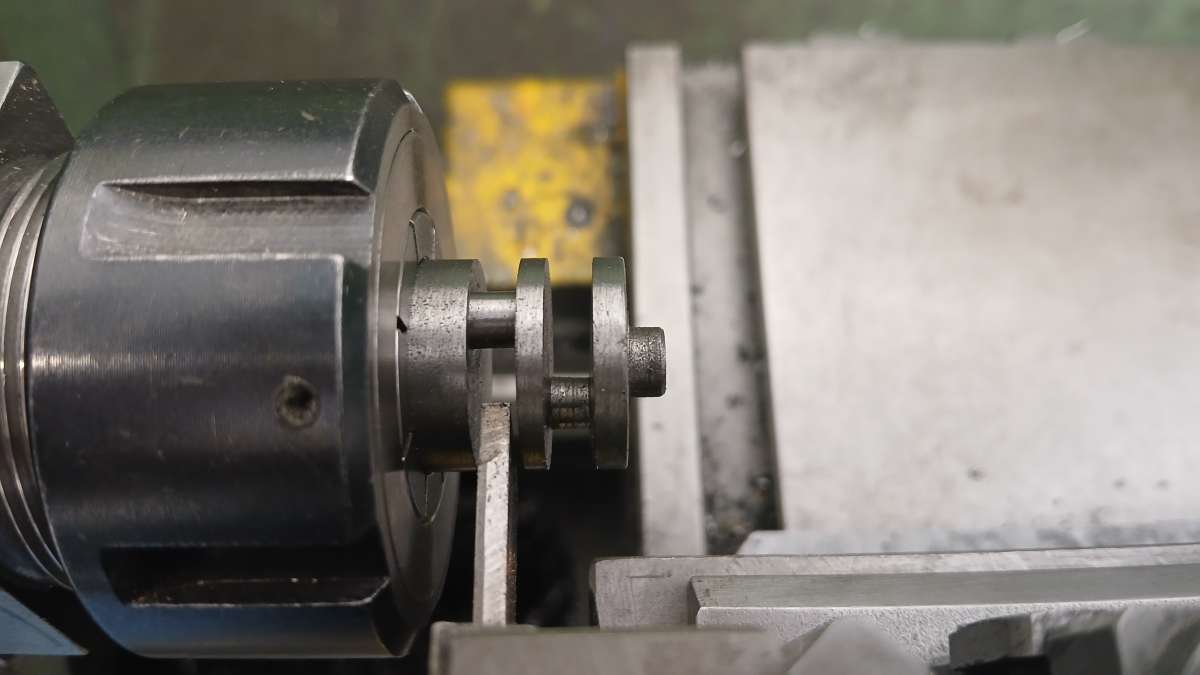
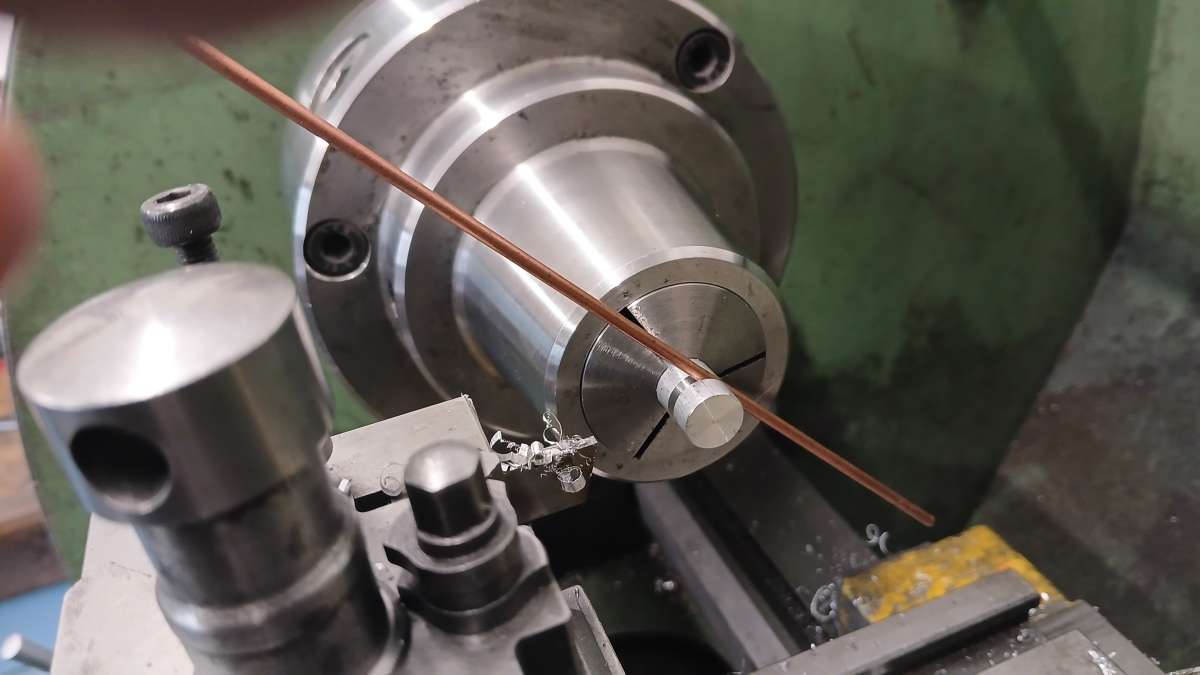
        There were no cylinder heads in the box of parts so I made some new ones, opting for aluminium instead of the specified brass. The backstop in a 5C collet made getting them all to the same thickness easy. I reduced the recess in the top of the head down from 3/8″ to 5mm a sI could see no reason for it to be full diameter which just increases dead space. I also rounded over the top corner.

        20260918_144753

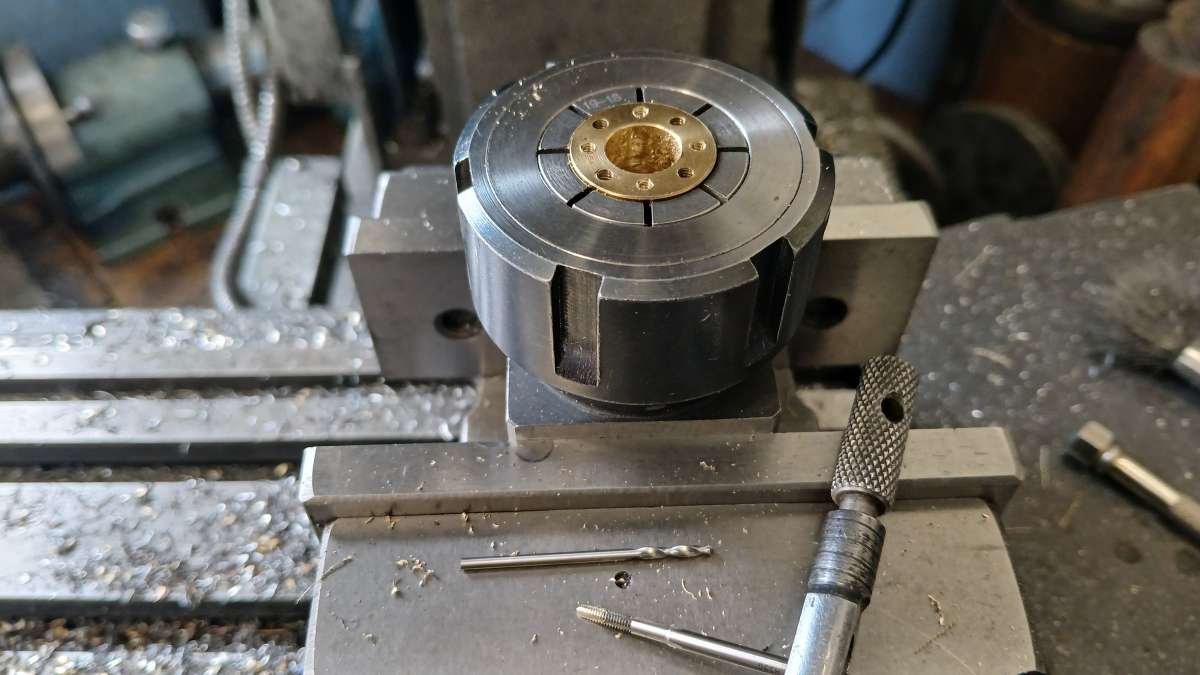
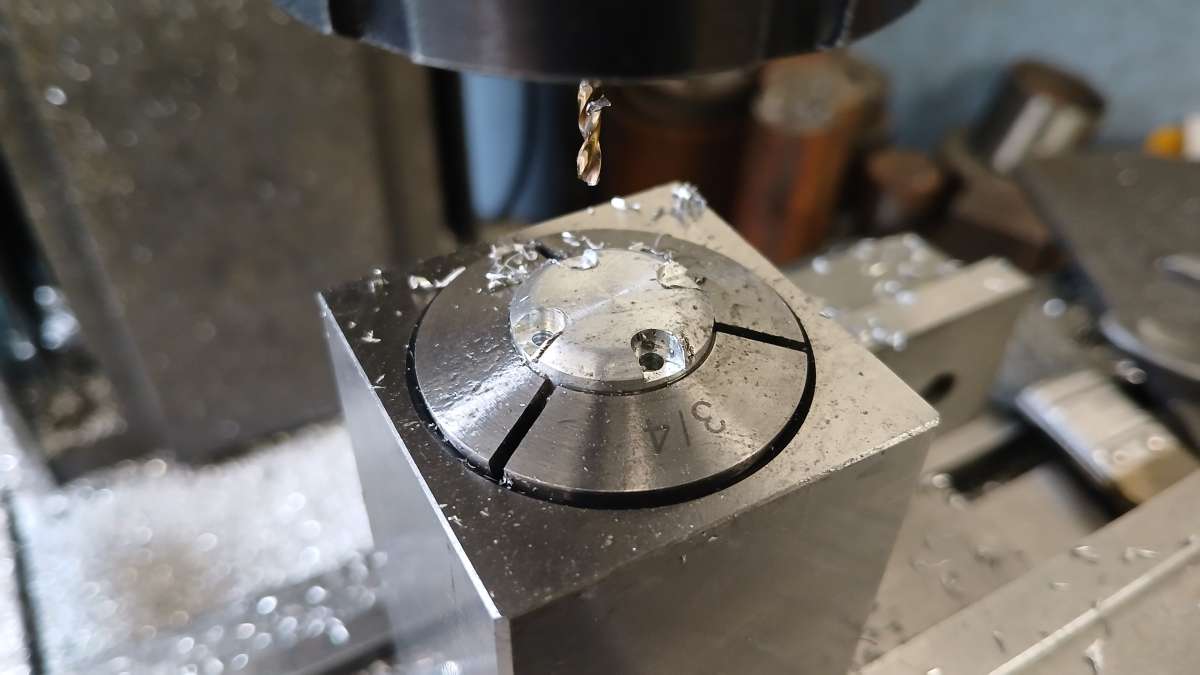
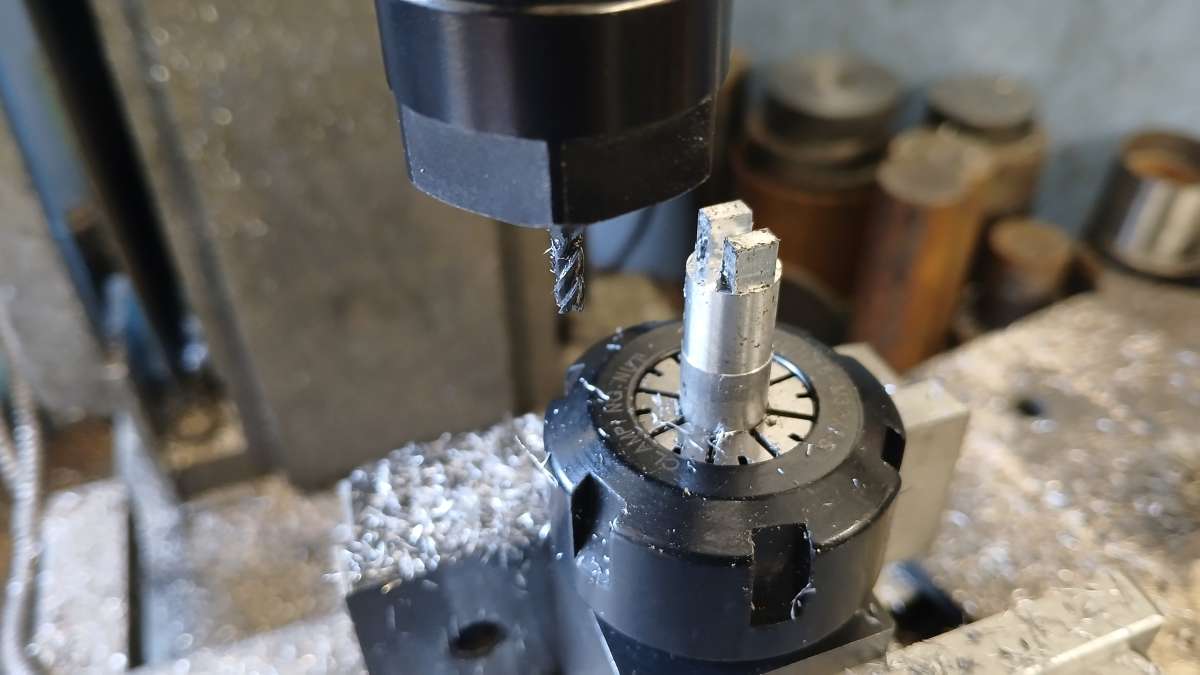
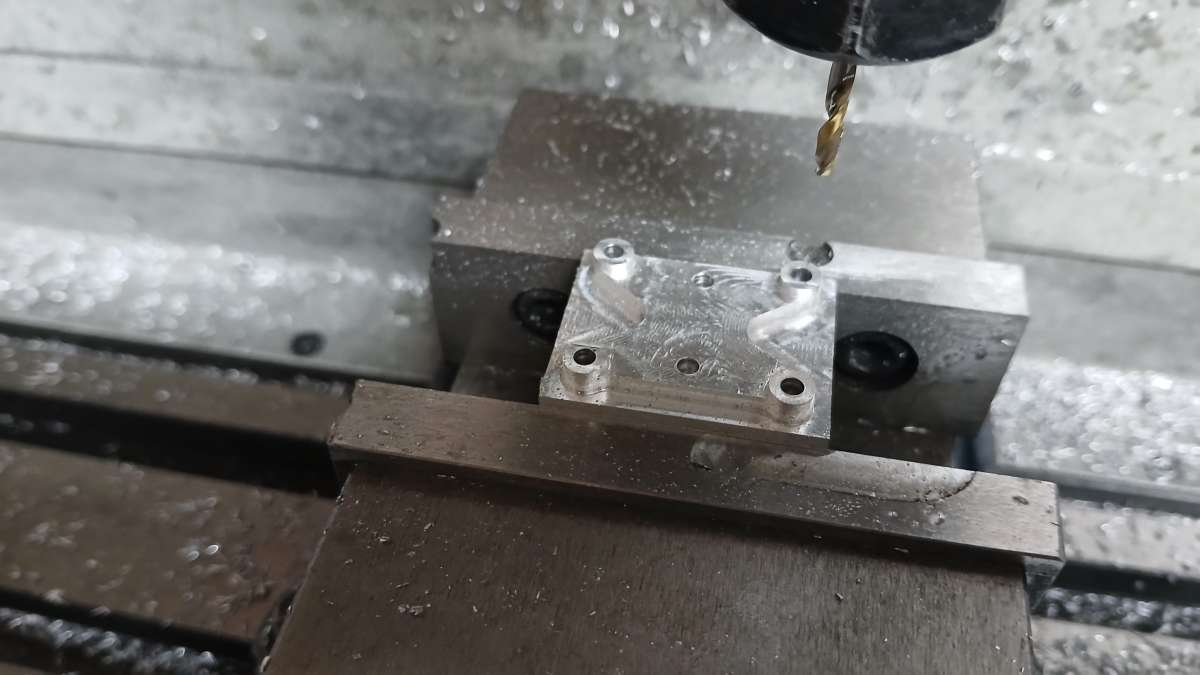
        Over to the mill with the 5C collet in a block slots were milled in from the edge to act as counterbores for the cap head screws and clearance holes drilled.

        20260919_085447

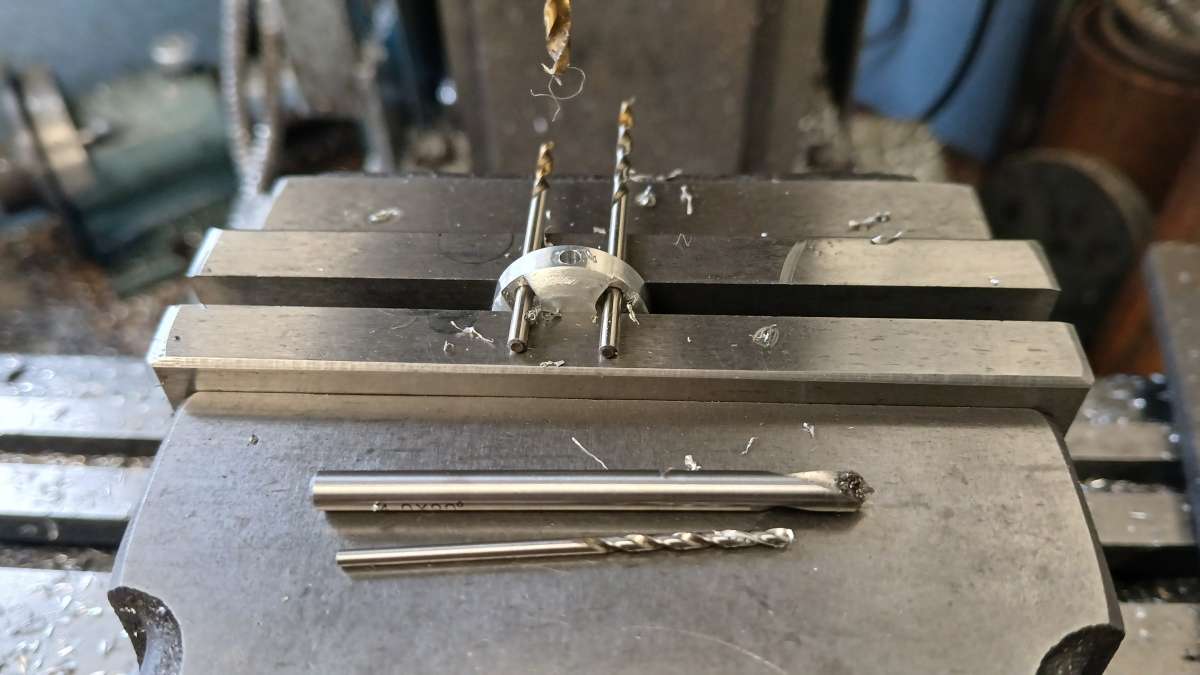
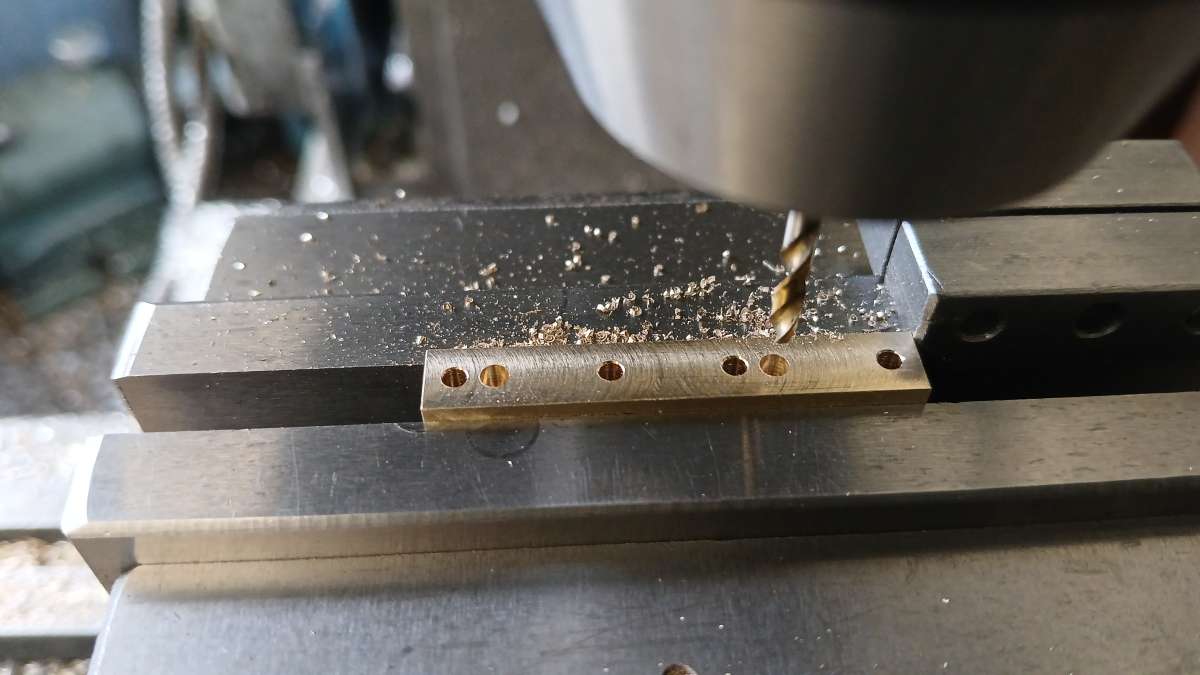
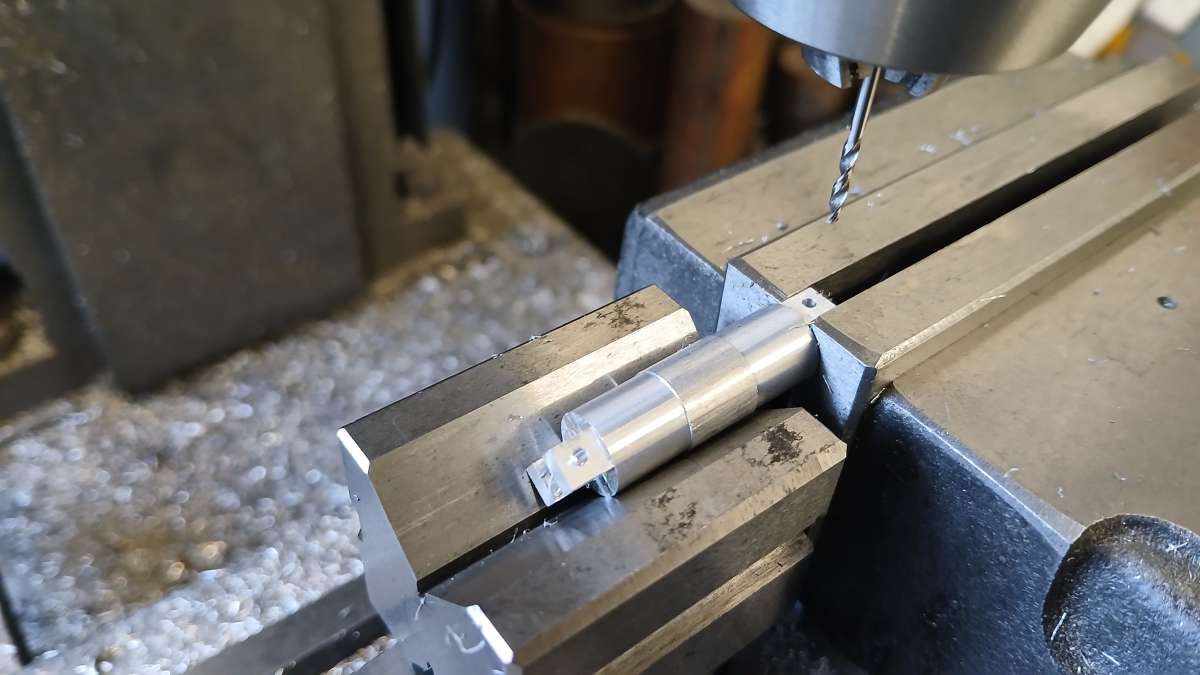
        Using a couple of drill bit shanks to align the heads the air passages were drilled and counterbored for the pipes

        20260919_094218

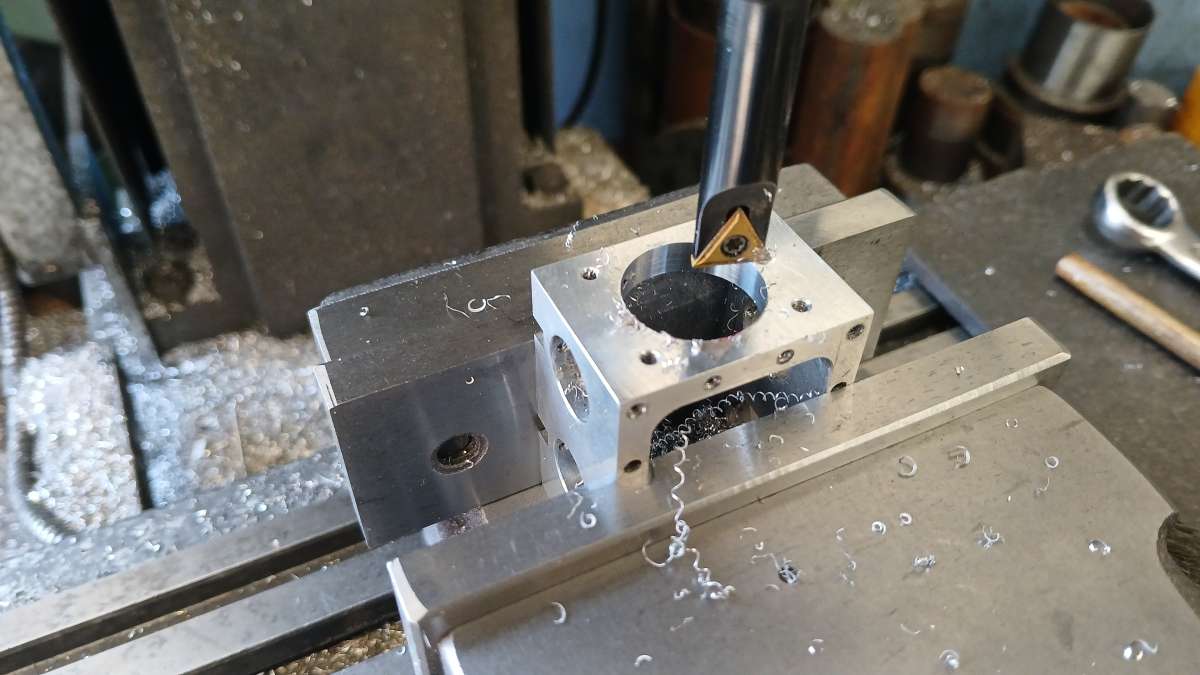
        There is a lengthways block of brass that fixes to the top of the crankcase and houses the rotary valve, the hole for which had wandered badly out of position so a new one had to be made. I used 1/2″ thick material rather than the suggested 3/8″ and left it over thickness so that I could mesh the gears correctly when I got to that stage.

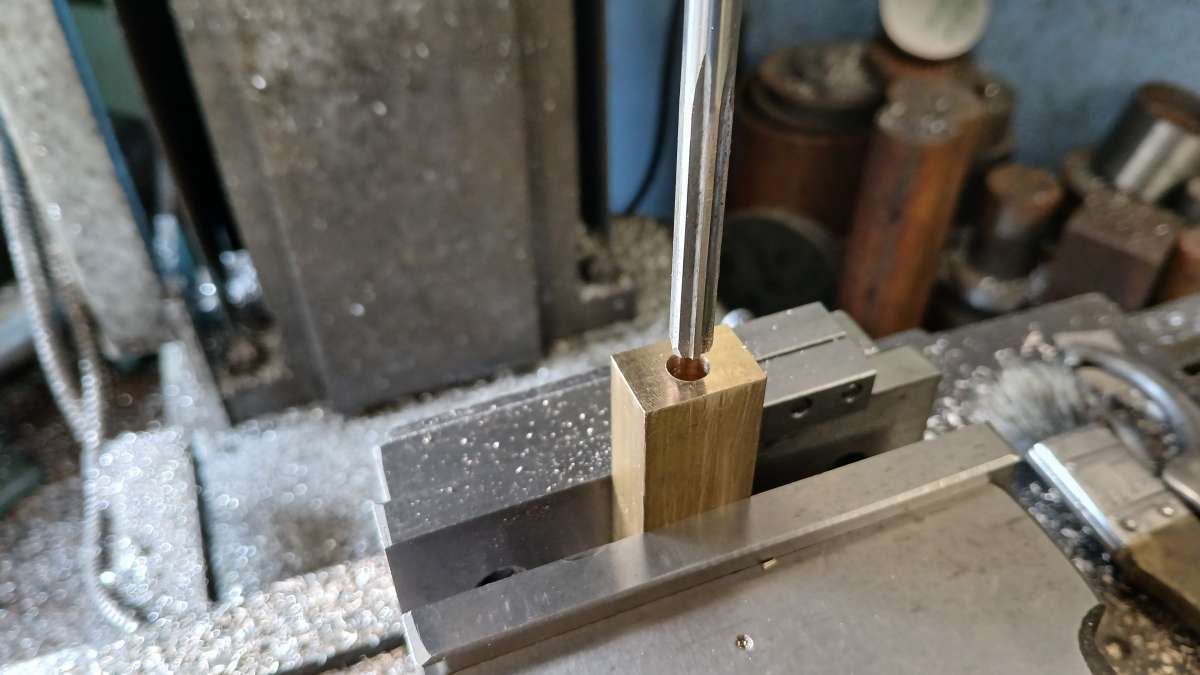
        I drilled 6.1mm to approx mid way from each end and then ran a 1/4″ machine reamer right through the full 2″ length

        20260919_122708

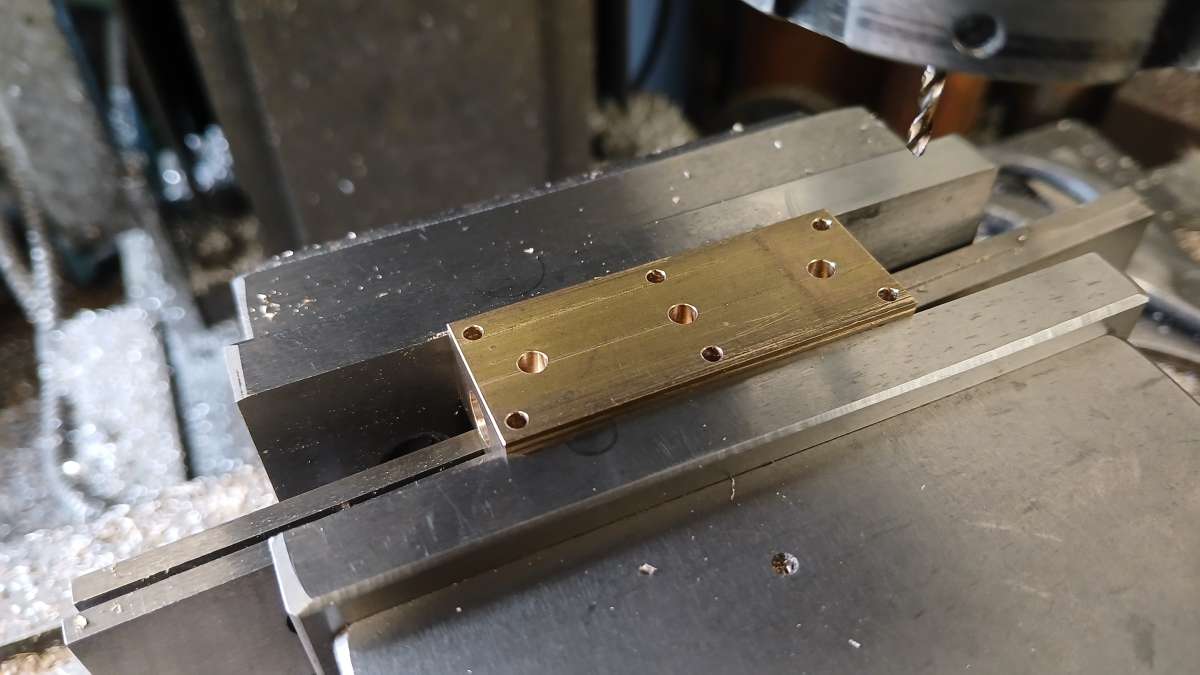
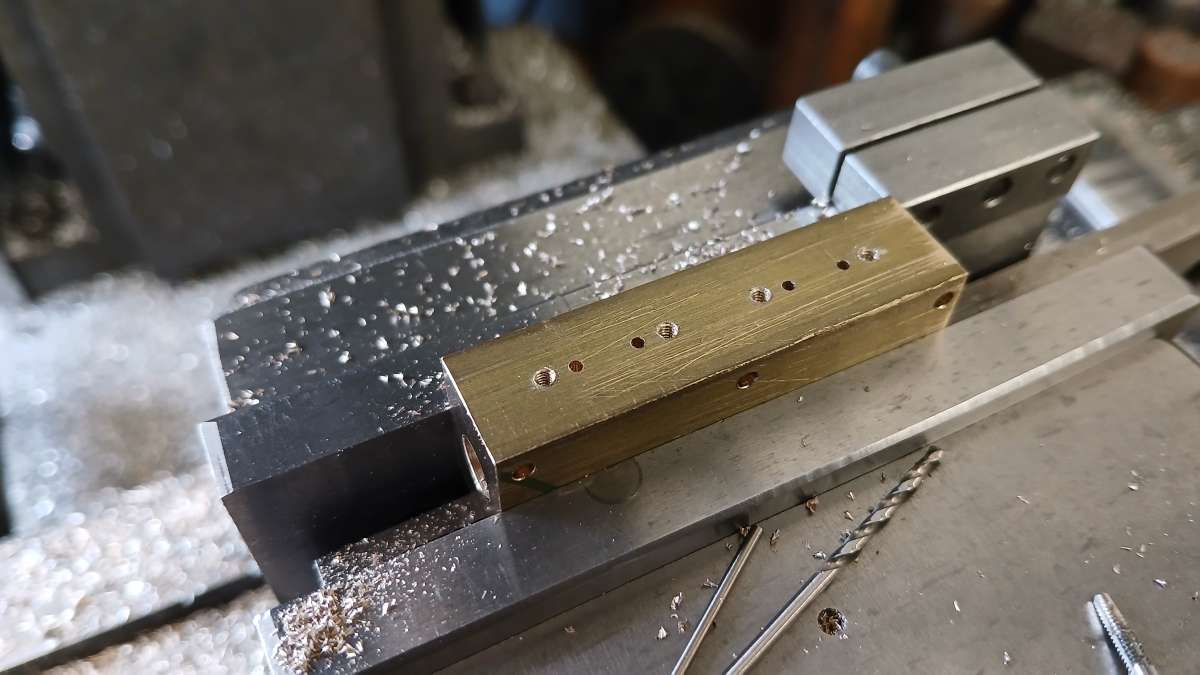
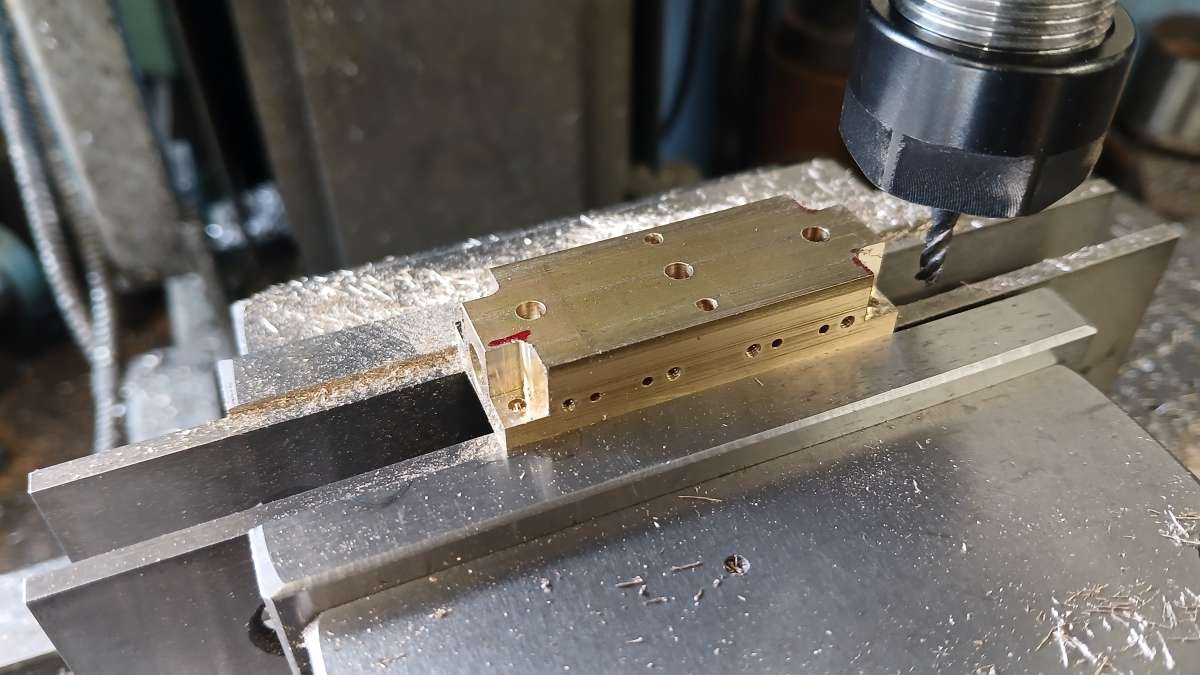
        Then added the various holes foar air, exhaust and mountings

        20260919_135801

        20260919_142110

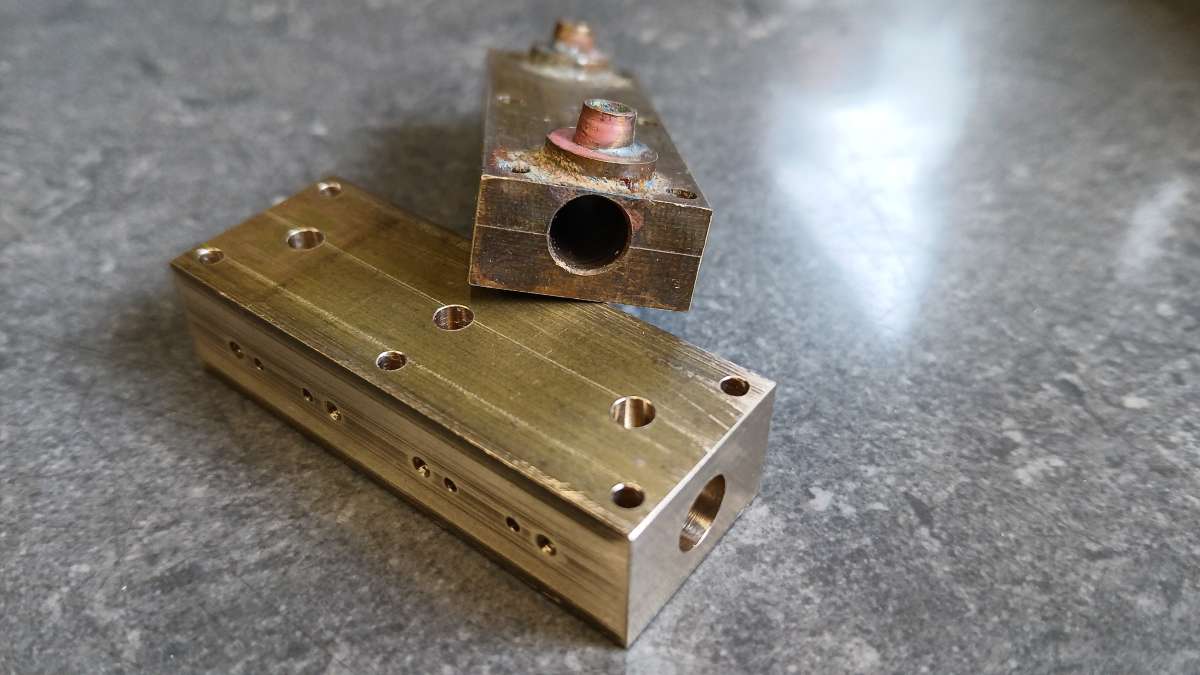
        Here you can see how the hole had wandered on the original which would have thrown the gear mesh out ( more of that later) and had also required those ugly bushes to be soldered to thetop as there was not enough thickness above the hole to take the exhaust pipes.

        20260919_144019

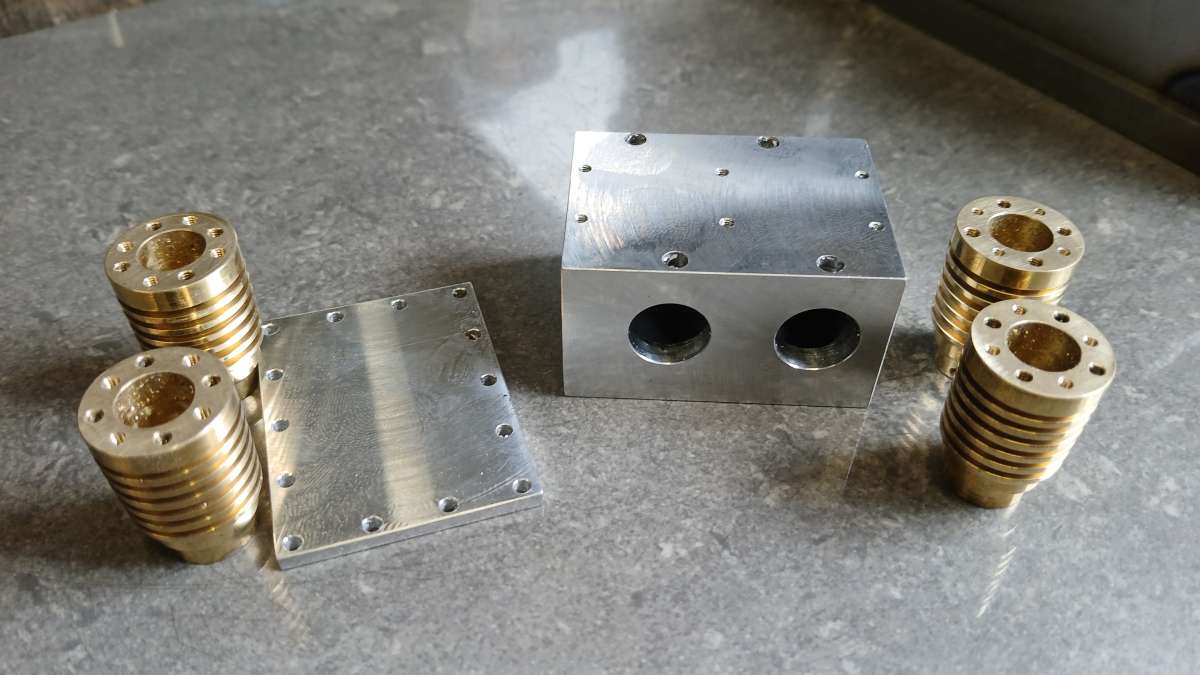
        The manifolds which run down each side of the valve block were fairly straight forward, I moved the positions of the air pipes so that they lined up with the ctr of each cylinder rather than being off to one side as per the original hole layout.

        20260920_090940

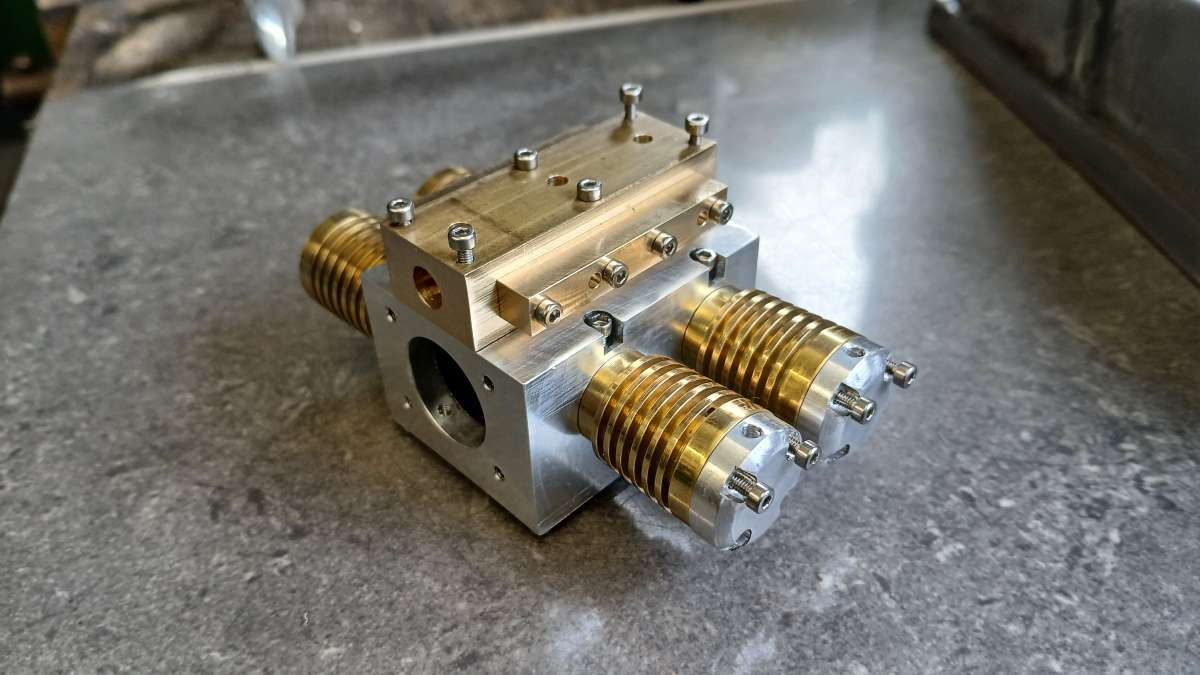
        Starting to look a bit like an engine now.

        20260920_102729


        #868396
        renardiere7
        Participant
          @renardiere7

          Looks great!

          #868502
          JasonB
          Moderator
            @jasonb

            Thanks.

            The same could not be said of the crankshaft. All the running surfaces were incredibly rough and would soon have eaten their way through anything running against them. Three of the four crankpins were oversize and one just about onsize depending where you took the measurements as all were tapered. It also looked like the parting tool had wandered sideways as the cut got deeper. But I took on the challenge.

            I cleaned up the long shaft and stub shaft so that the flanged ball races would fit and thought I would offer up the shaft into the crankcase to check the various lengths, guess what the hole in the crankcase was too small.

            You can see some of the poor machining in this pic where it should drop into the hole

            crank fit

            That was soon sorted with the boring head, luckily I had not made the aluminium plug/bearing housing that goes in the hole yet.

            20260925_135317

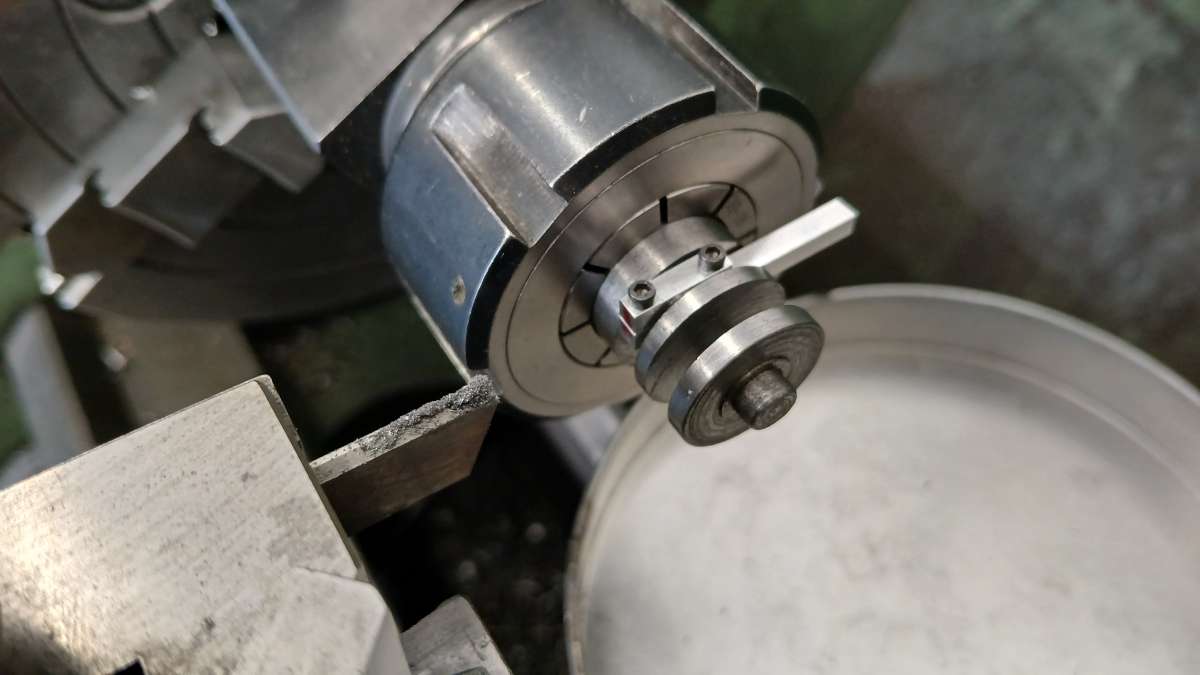
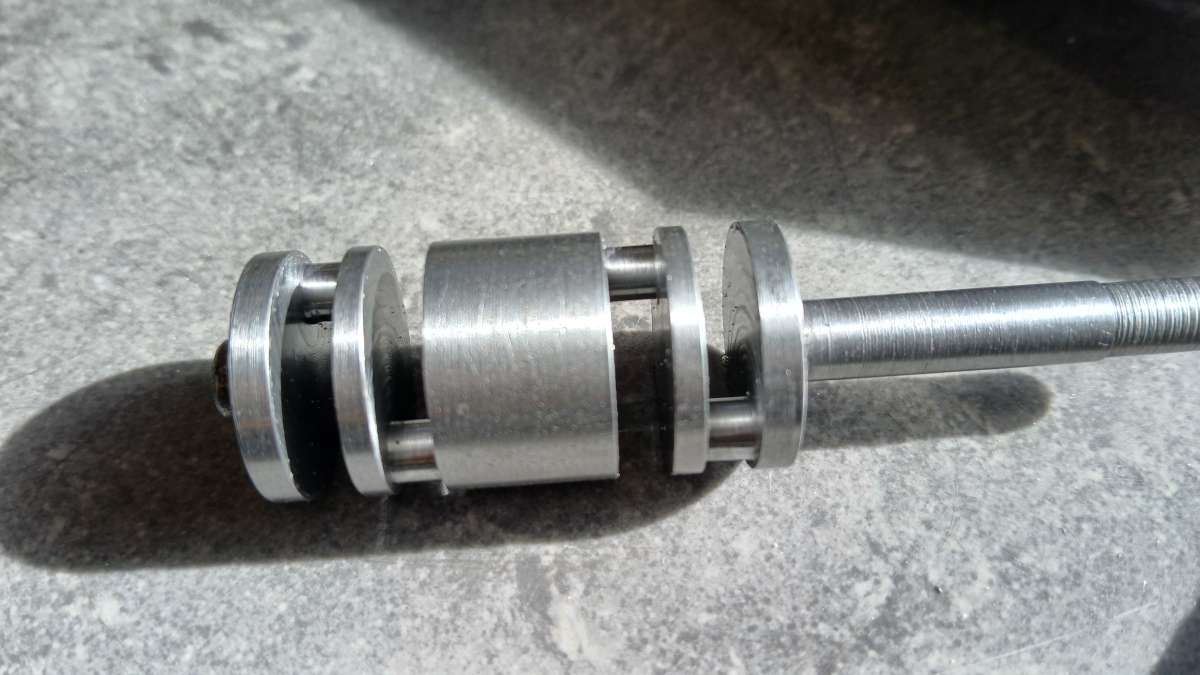
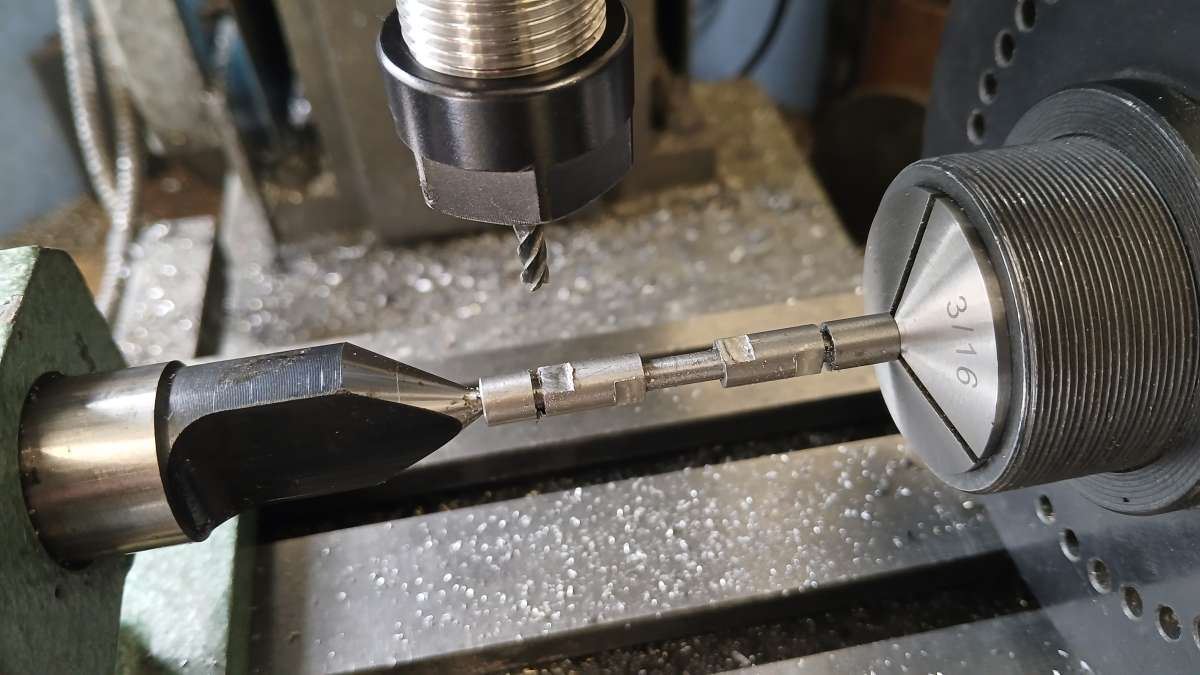
            As the gap between webs was only supposed to be 0.140″ it was not easy to clock the crank pins into position so I made the job a bit easier by holding a square ER collet block in the 4 jaw and set that with the correct offset. It was then just a case of rotating the crankshaft to position each pin. I used an HSS parting tool as I needed its full flat end width, a GTN-2 insert with it’s radiused corners would not have worked. The pin on the left has been finished the other is as it came to me.

            20260925_145702

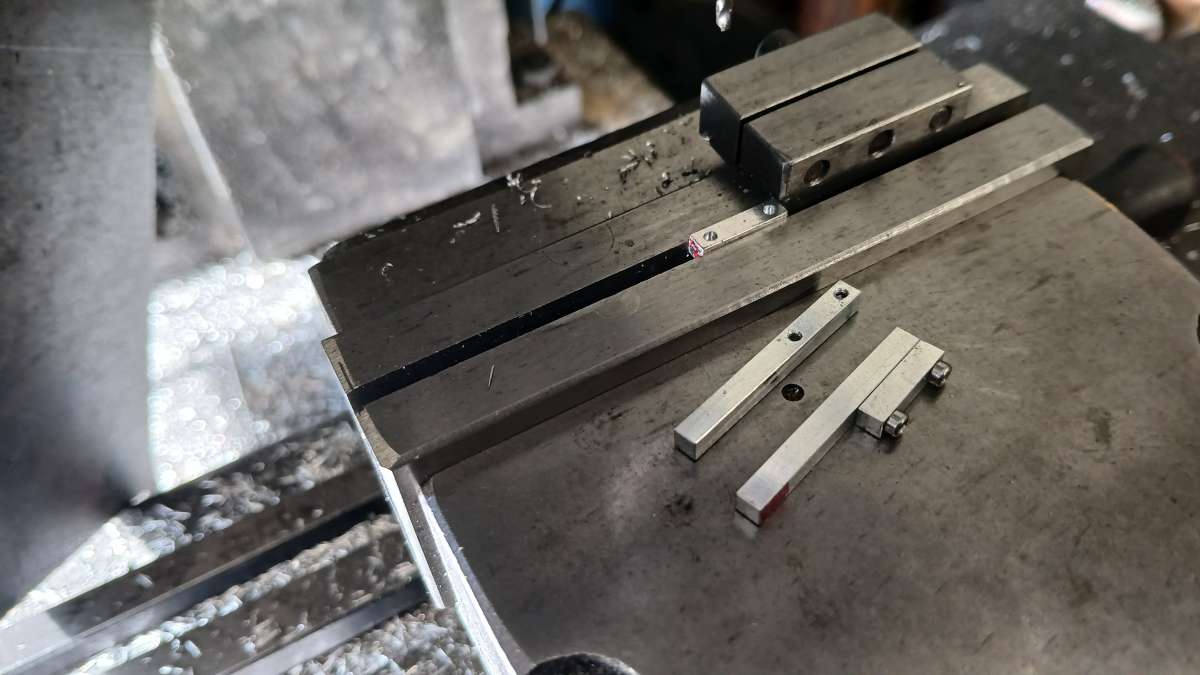
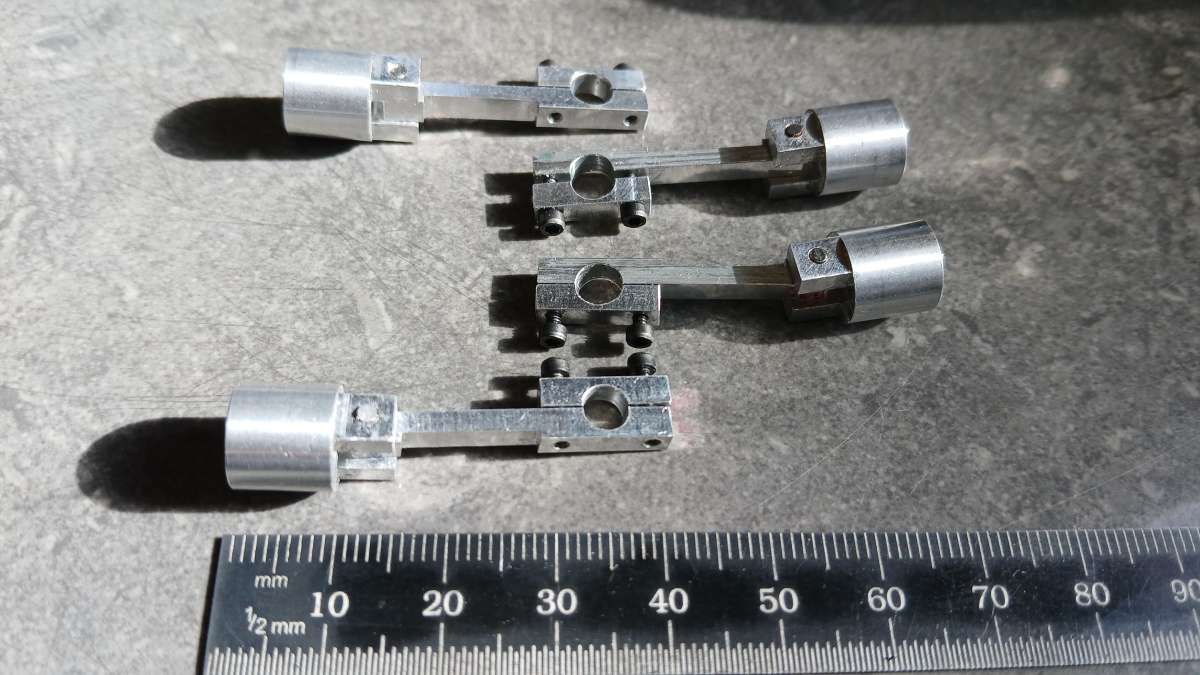
            As I could only get in to measure the diameter with the digi callipers I left the crankshaft in the lathe and went over to the mill to make the conrods so the pins could be checked against their reamed holes. The was a set of part built rods in with all the parts but as they had been made from steel (possible 1/8″ sq key steel) is did not fancy running steel on steel. Some offcuts of 2014 aluminium were found and machined to 1/8″ square section and then milled to length before drilling and tapping for M1.6 fixings.

            20260926_101237

            Once assembled, three were drilled and reamed 3/16 and use dto check the pins. The undersize pin cleaned up to a running fit on a 4.4mm drilled hole. They were machined so the assembled rod would rotate with light finger pressure but not drop with it’s own weight. Then a quick “shoeshine” with a thin strip of well worn 240g Emery cloth against the rotating pin just polished the surface and allowed the rod to drop. The metal dish below it to save loosing anything in teh swarf tray as the big end caps are only 1/2″ long.

            20260926_122548

            With that and the bearing carrier done I did need to reduce the overall length slightly so the shaft would spin freely between the flanged bearings without any noticeable end play. There is still an e-clip groove and keyway to be added to the long end.

            20260926_142901

            I could not resist adding all the conrods and giving the crankshaft a spin. The shafts were a bit too close to the top of the crankcase for comfort so I decide to take an additional 25thou cut to make sure nothing was hitting. More of that story revealed itself later 😲😭

            #868697
            JasonB
            Moderator
              @jasonb

              Next I decided to make the rotary valve, this is specified as silver steel but I though stainless would be better and it was actually a slightly closer fit in the reamed hole. First job was to reduce the end to fit the gear, I had already spotted that the hole in the gear was larger than the specified 3/16″ and by the looks of it the previous builder got as far as drilling about 15/64 and realised his mistake and did not go as far as reaming 1/4 which would just have slid along the 1/4″ shaft.

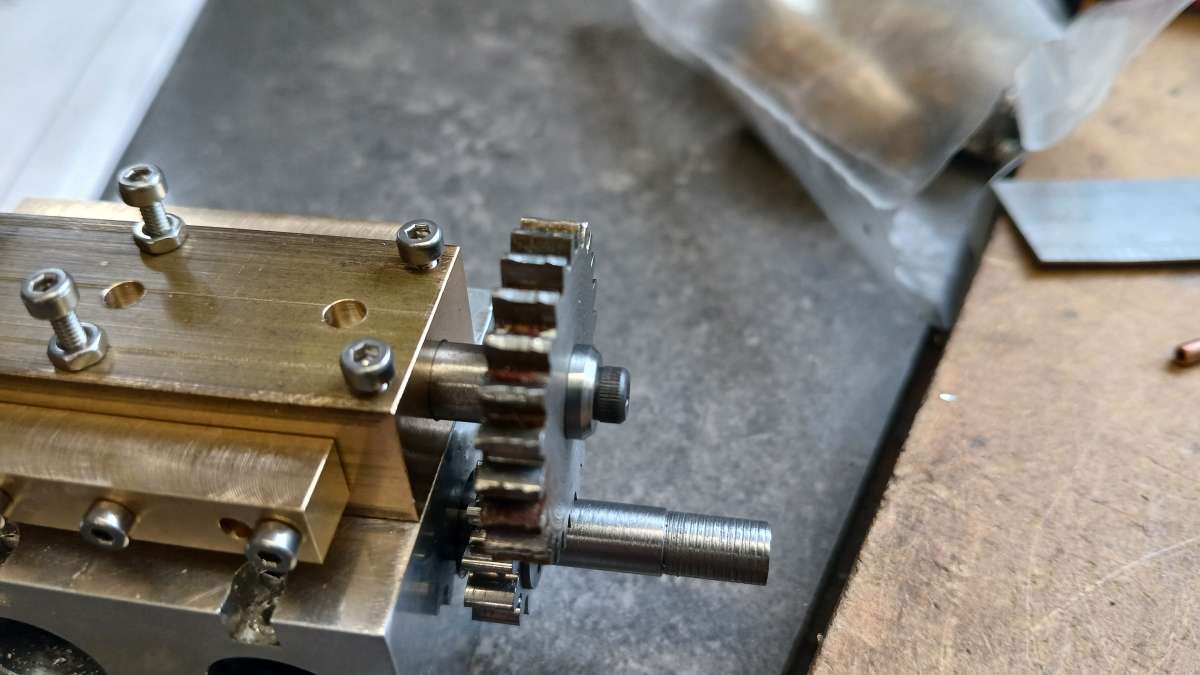
              With the gear on it’s slightly reduced spigot and retained by the “washer” detailed in the drawngs I offered it up to the part assembled engine. Now as I had left some metal on the bottom of the valve block things should have gone together with a lot of backlash in the gears but as you can see they would not mesh as the ctr distance was too small.

              20260927_142003

              It was at this stage I realise dthe crankshaft hole had been placed far too near the top of the crankcase and that would also have explained why I felt the conrods were getting too close to the inside top surface. My options were to either make a new crankcase or something else. In the end I opted for something else in the way of some new gears, this was partly decided by the poor finish on the larger gear, if you look at the crests of the teeth in the photo above you can see how uneven they are along their length so may not have run well even with the correct PCD

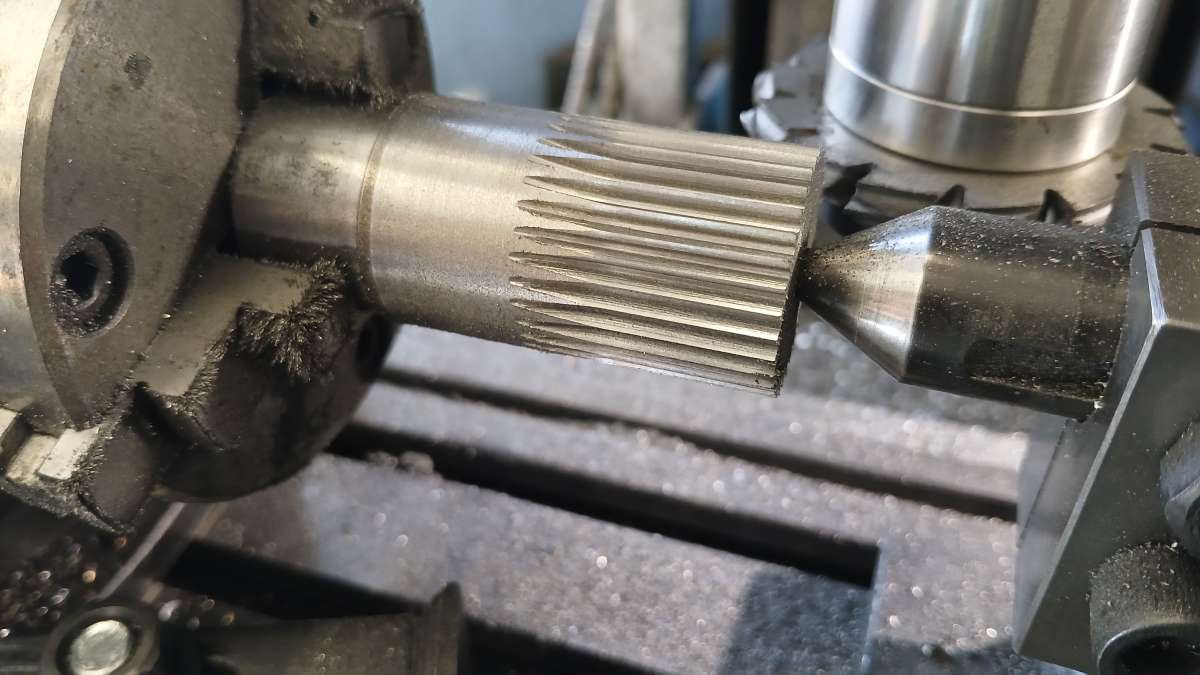
              By reducing the gears from the original 30DP down to 32DP I could get them in with just a little to come off the bottom of the valve block as originally intended. The large one was cut from cast iron bar and I cut the stick long enough for two.

              20261001_142505

              The same for the smaller one which was cut from steel

              20261001_150042

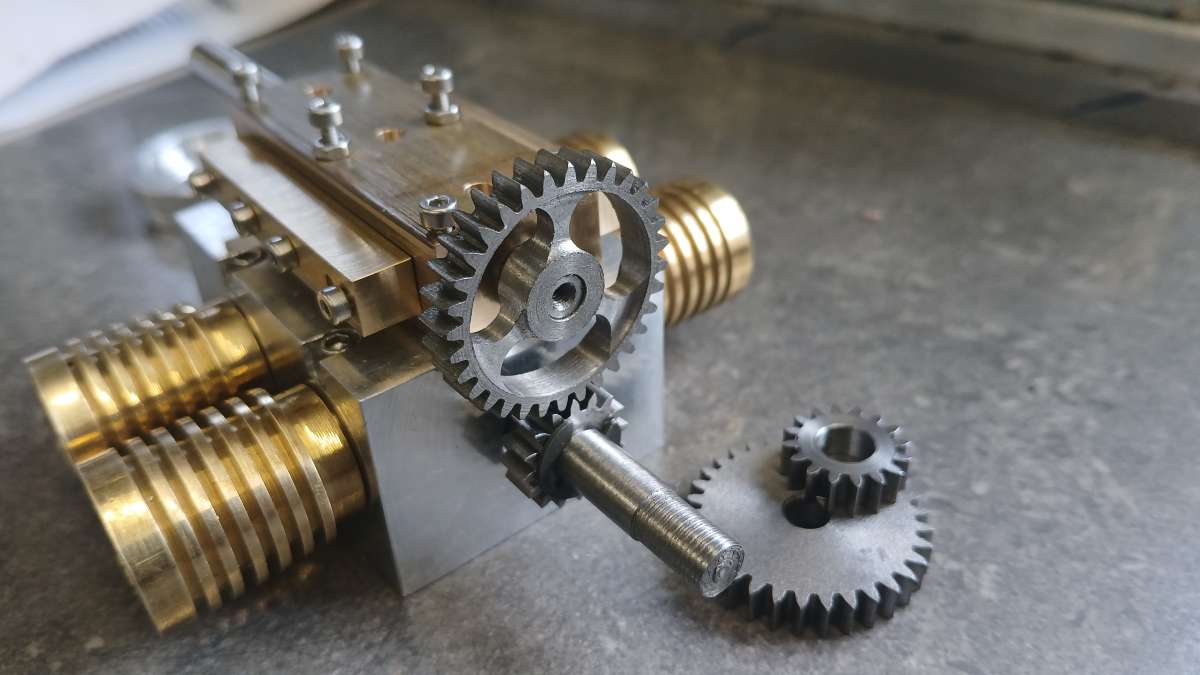
              A few minutes on the rotary table had the large gear looking a bit more interesting. The central hole was the correct 3/16″ this time.

              20261002_145038

              And they went together, still the material to come of the valve block which is why the gap is large

              20261002_145257

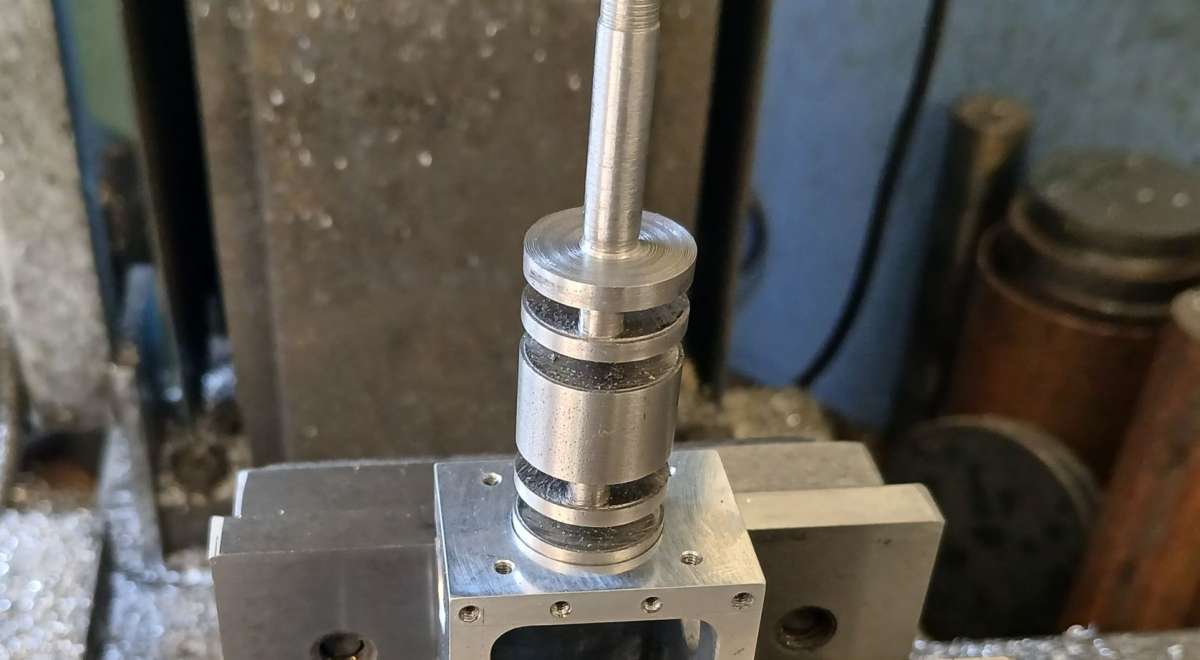
              I could now get on with the valve, just a case of cutting the groove nearest the end, moving the bar out of the chuck a bit more and doing the next groove.

              20261003_092903

              I used the 5C spin indexer to position the cuts at 90deg as I can get in closer than a chuck on the rotary table allows. The flats are what open the various drillings and passages to allow the air in or out.

              20261003_134849

              With the valve block milled to final height the pockets could be milled in each corner to clear the screw heads.

              20261003_143011

              #868966
              JasonB
              Moderator
                @jasonb

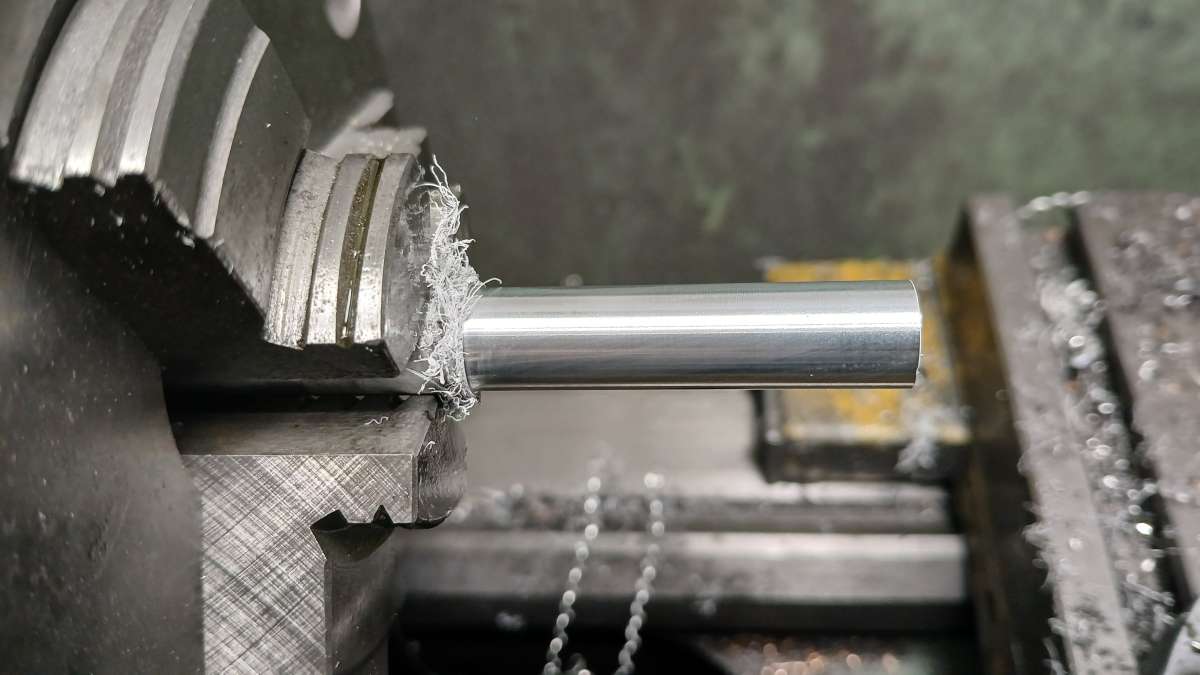
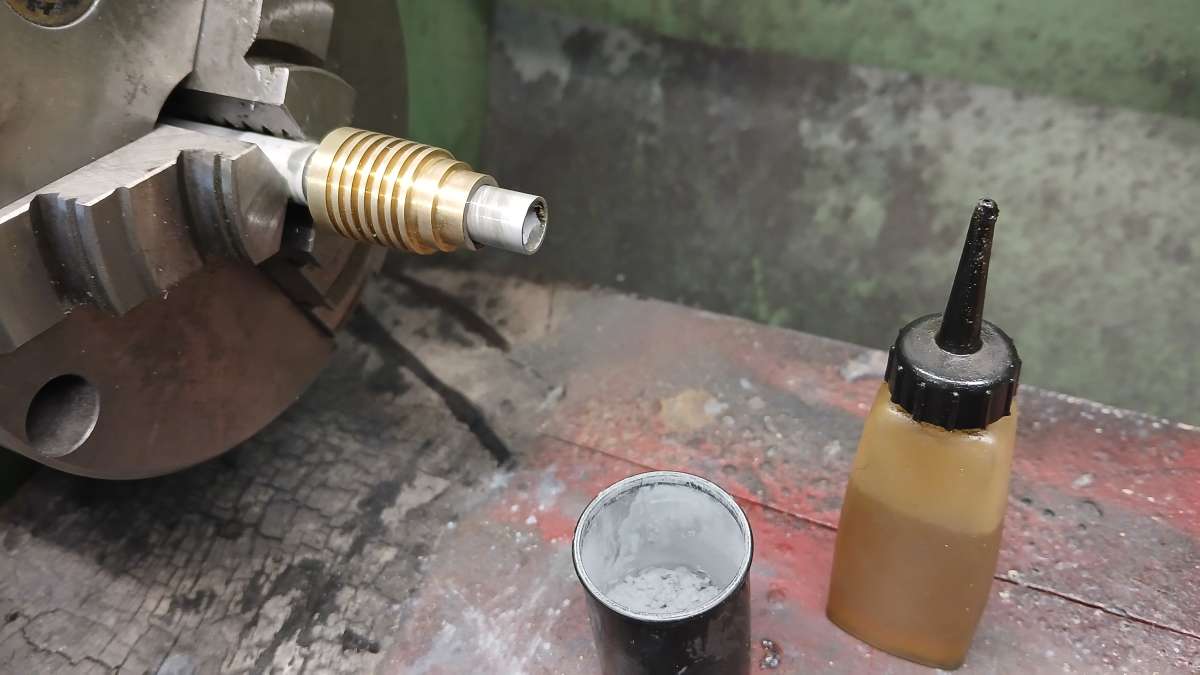
                Before making the pistons, I thought it best to lap the cylinders so an odd bit of 10mm dia aluminium tube was turned down to a close fit inside the now all the same size cylinders. That is the paint layer at the chuck end not swarf.

                20261004_081723

                Some 1000grit silicon carbide powder mixed with a little oil made a suitable paste to give each cylinder a quick lap.

                20261004_083002

                It was then just a case of turning some 10mm aluminium down to size for the pistons using the cylinder as a gauge to get the correct fit. These little pistons have a forked end machined at the bottom to take the conrod.

                20261004_085933

                Which is then cross drilled for a 1/16″ gudgeon pin

                20261004_092757

                I found that 1/16″ iron rivits were a good fit as the shank just below the head increased in diameter so with the addition of a tiny drop of Loctite they could be pushed firmly home and the excess sawn off with a piecing saw.

                20261004_141143

                It was hard to resist a quick trial assembly to check if things went round and round or in and out as they should.

                About now the last of the gifts from this set of parts that kept on giving made itself known. Turns out that matey boy who started the build got his crank pins in the wrong positions so instead of having two pistons on the power stroke and the other two on the exhaust stroke all four moved in unison😬😬😬😬

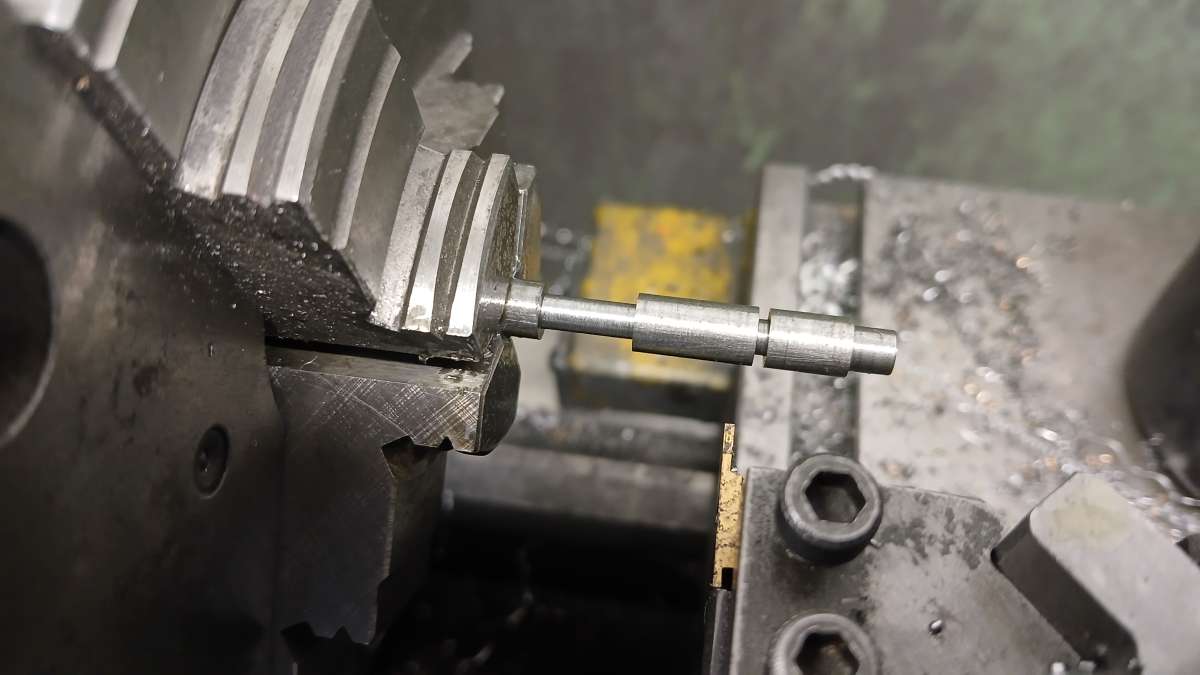
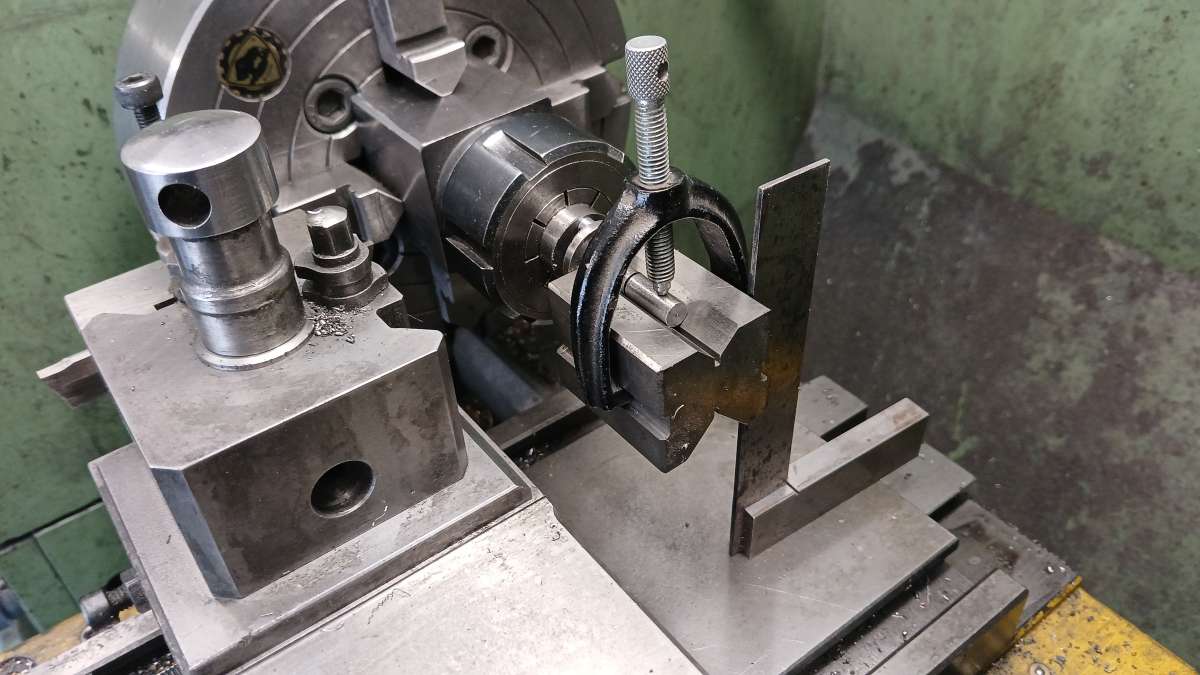
                There was no other way around it other than to make a new crankshaft, I guess I should have checked the old one more closely before doing the remedial work on it but where is the fun in that. Having the crank webs as full circles makes it quite easy to hold and it is just a case of turning one pin, sliding the material out a bit more and turning the next.

                Luckily I had left the ER collet block in the 4 Jaw so there was not much to set up. After doing one pin I used a square to set the collet block’s edge vertical and then clamped a vee block to the shaft checking that it too was vertical. Then simply rotate the shaft and it’s vee block 180 degrees and it was ready to cut the next pin.

                20261005_121504

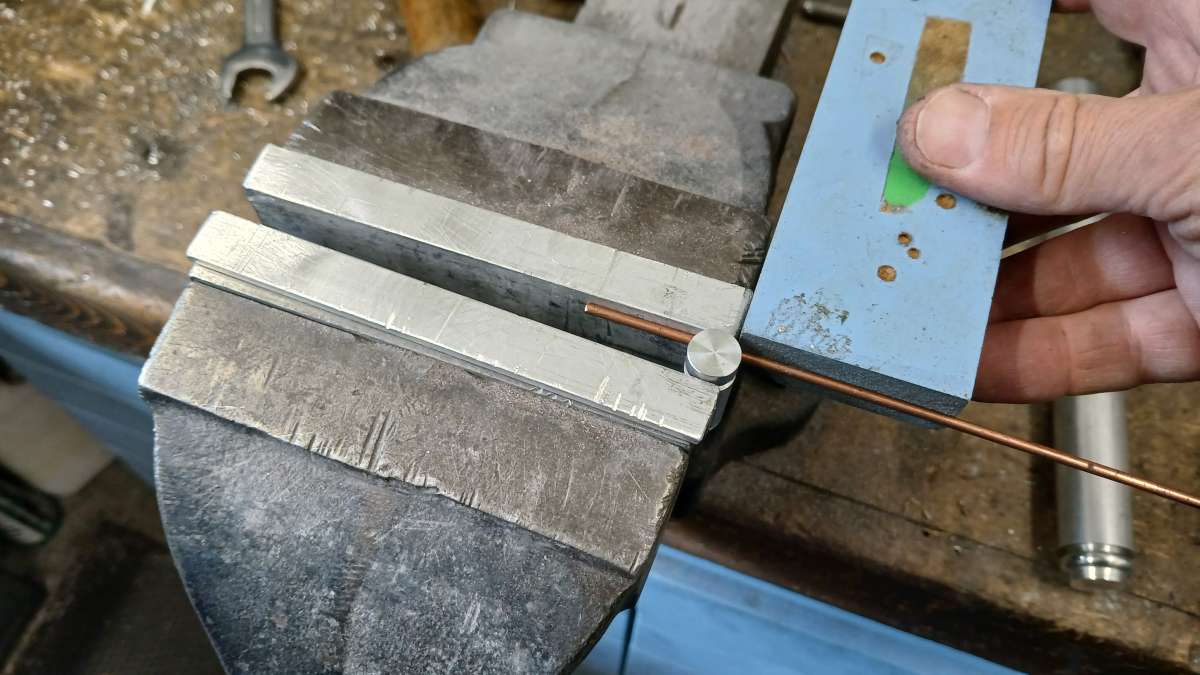
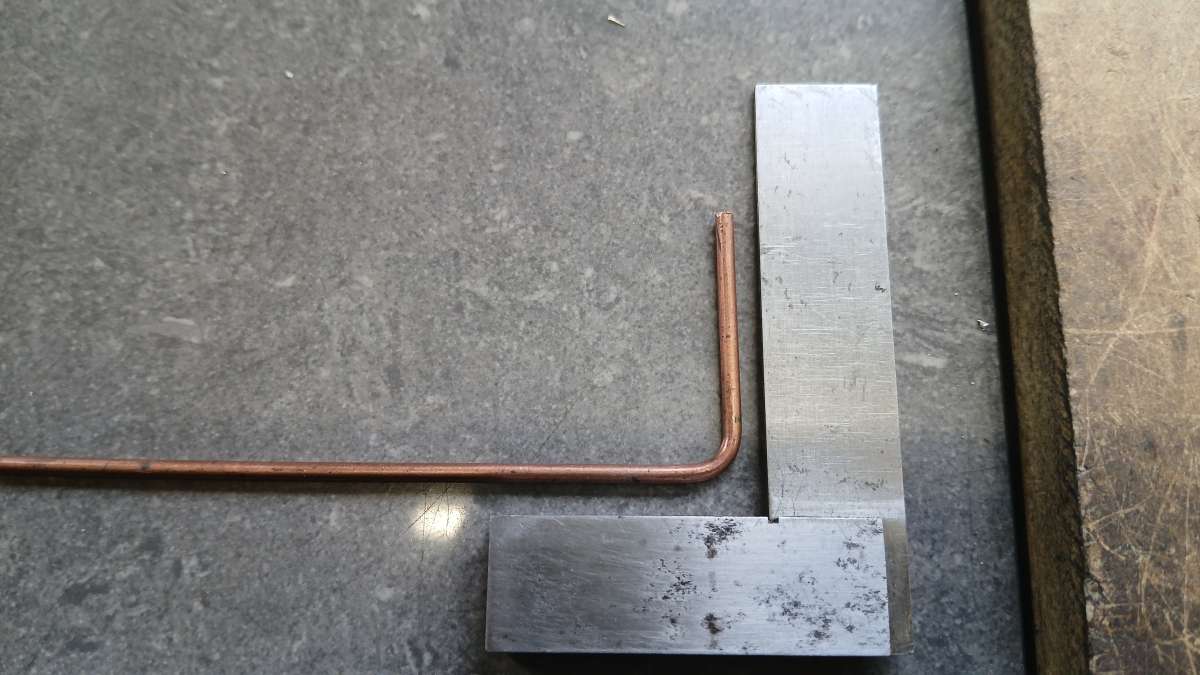
                As you know I’m not one for tool making so no fancy pipe benders for me. Just a groove cut in the end of a bit of bar the width and depth of the tube to be bent.

                20260927_085128

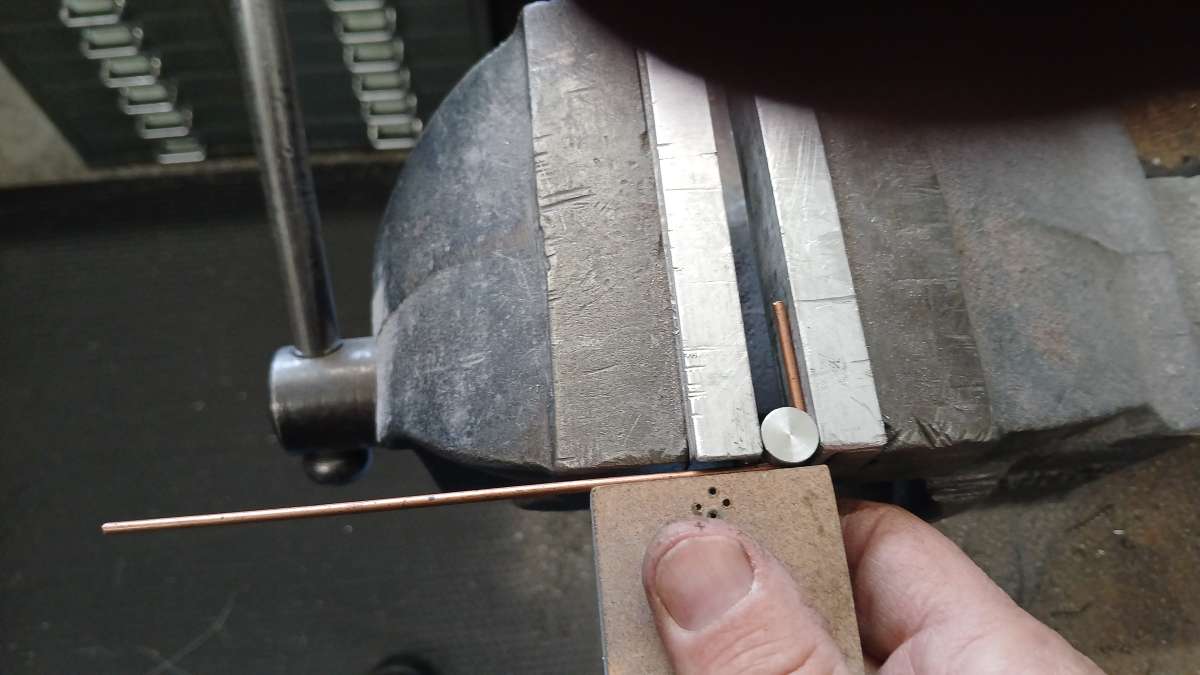
                Then hold the two in a vice towards one end and push the pipe round with a bit of something flat, MDF in this case

                20260927_085450

                20260927_085757_001

                Rinse and repeat for the other pipes needed

                20260927_085840

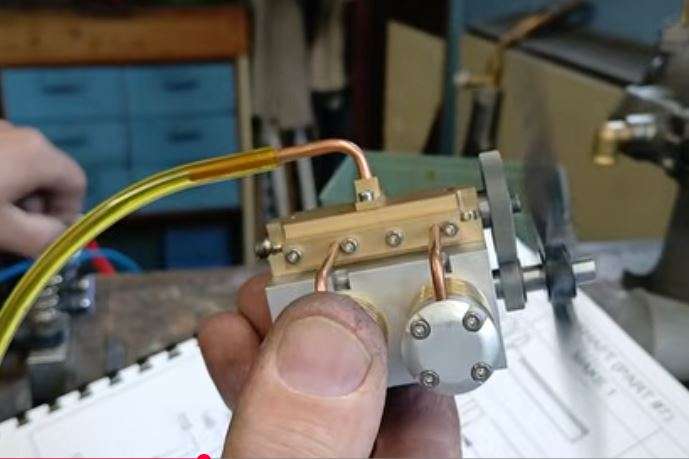
                That gave me enough parts to see if the thing ran or whether there were any more hidden features that I had not spotted. I did not run it too fast as the prop os only pushed on for now.

                #868989
                JasonB
                Moderator
                  @jasonb

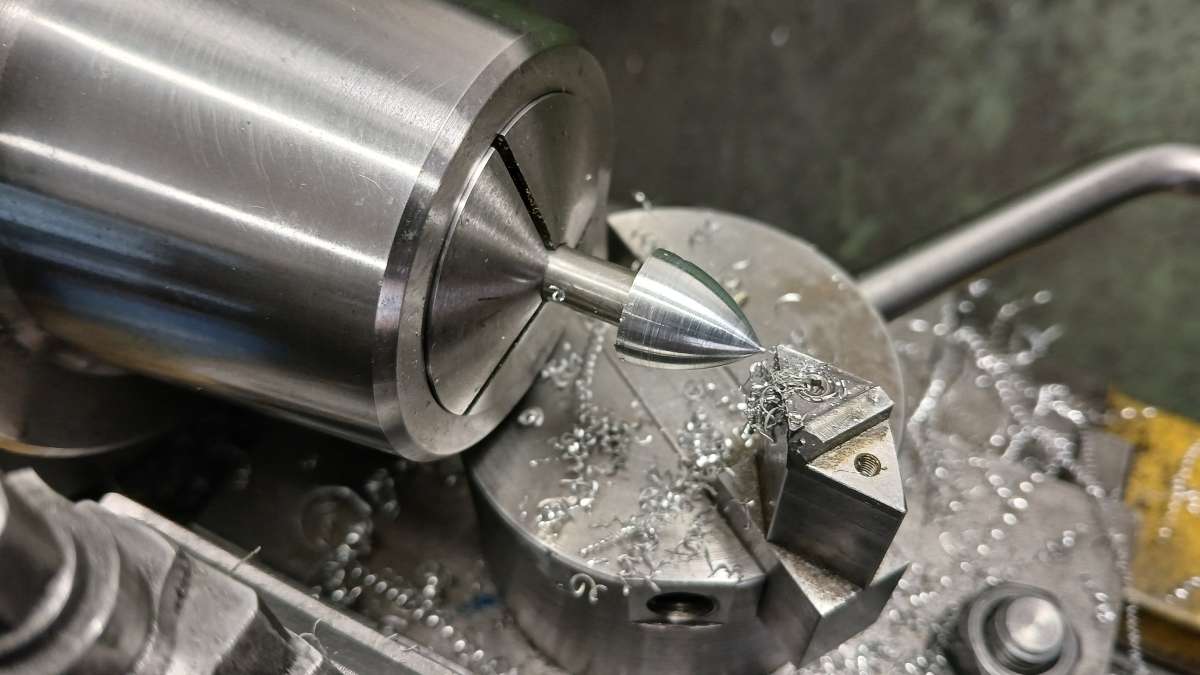
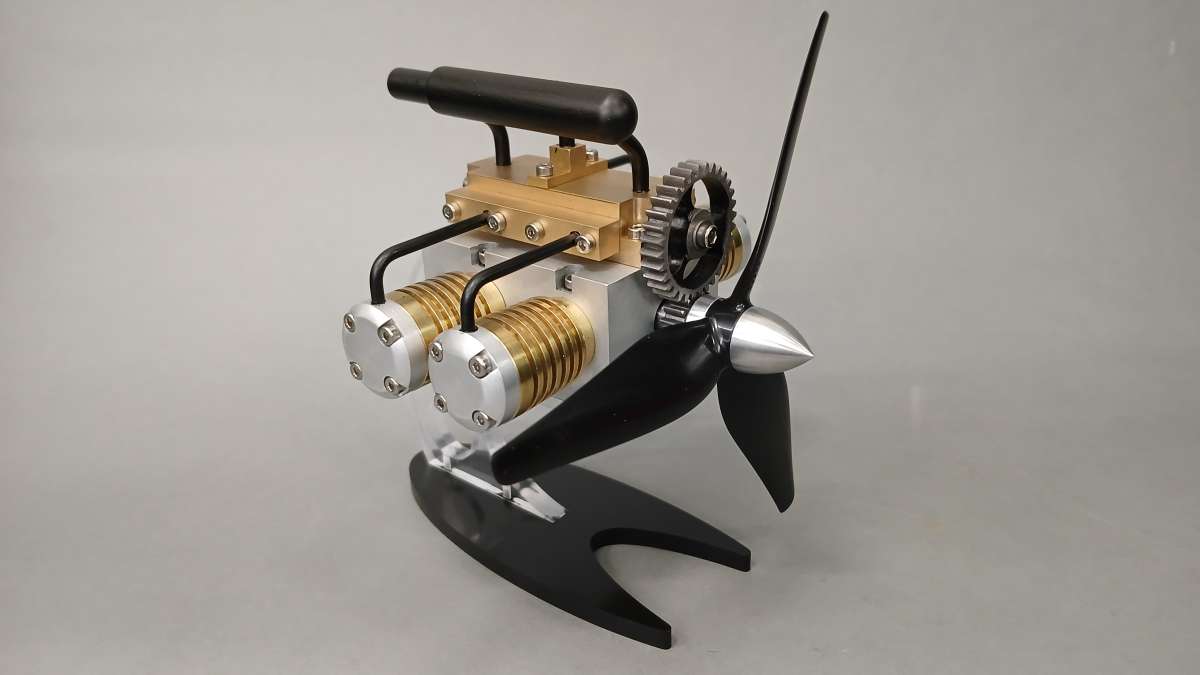
                  With a running engine the last few bits could now be done to make it look nice. First was a prop spinner that was shaped using my ball turner. I also had to add a small spacer between the prop and crank gear to ensure that the blades cleared the head of the screw that retains the larger valve gear.

                  20261006_122012

                  You can also see in this still from the video that I have added spacers to keep the gears clear of the cranckcase and valve block, there was nothing in the original design to stop the gears rubbing on things.

                  modifications

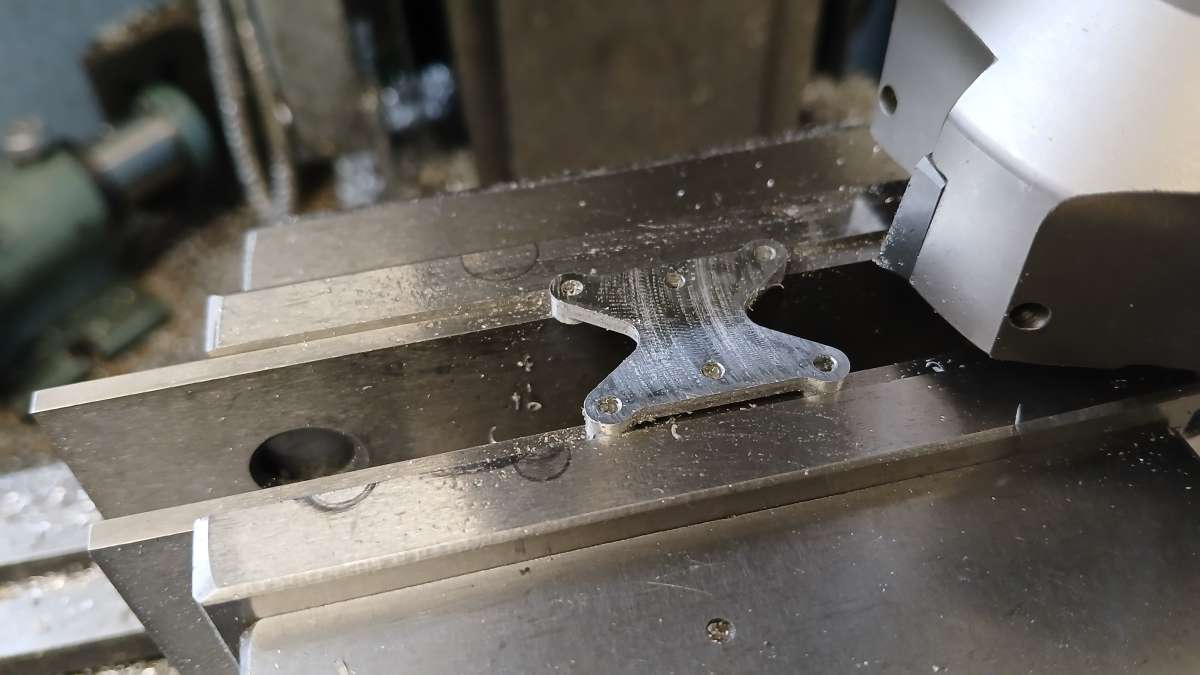
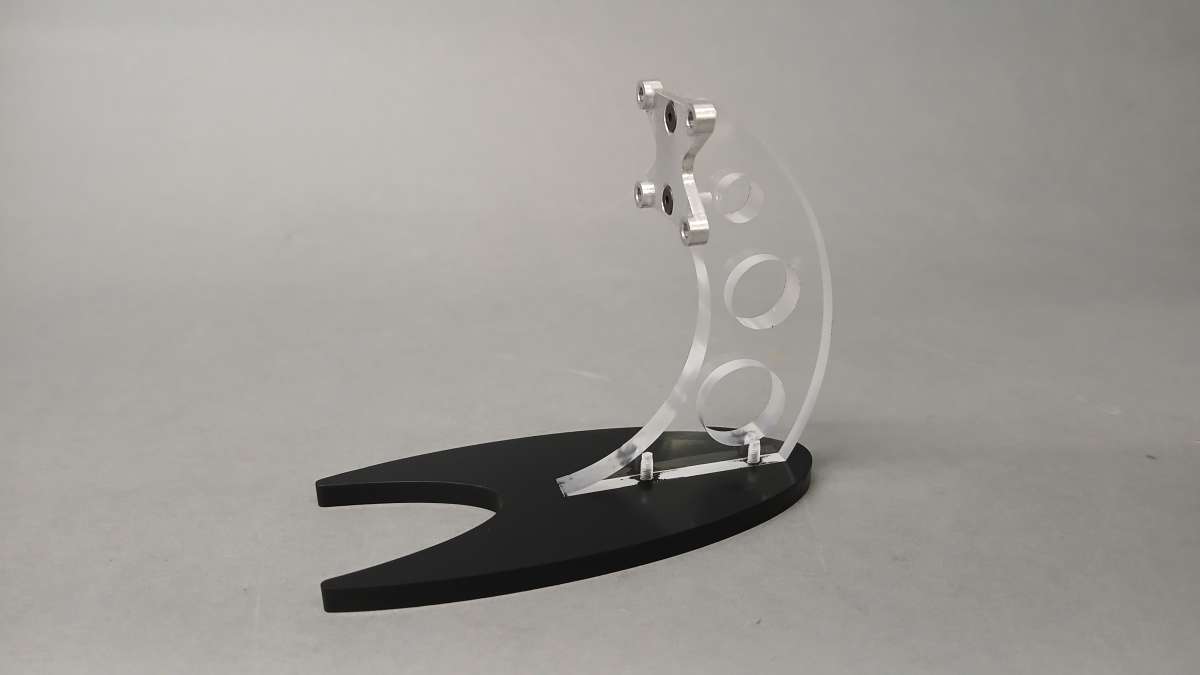
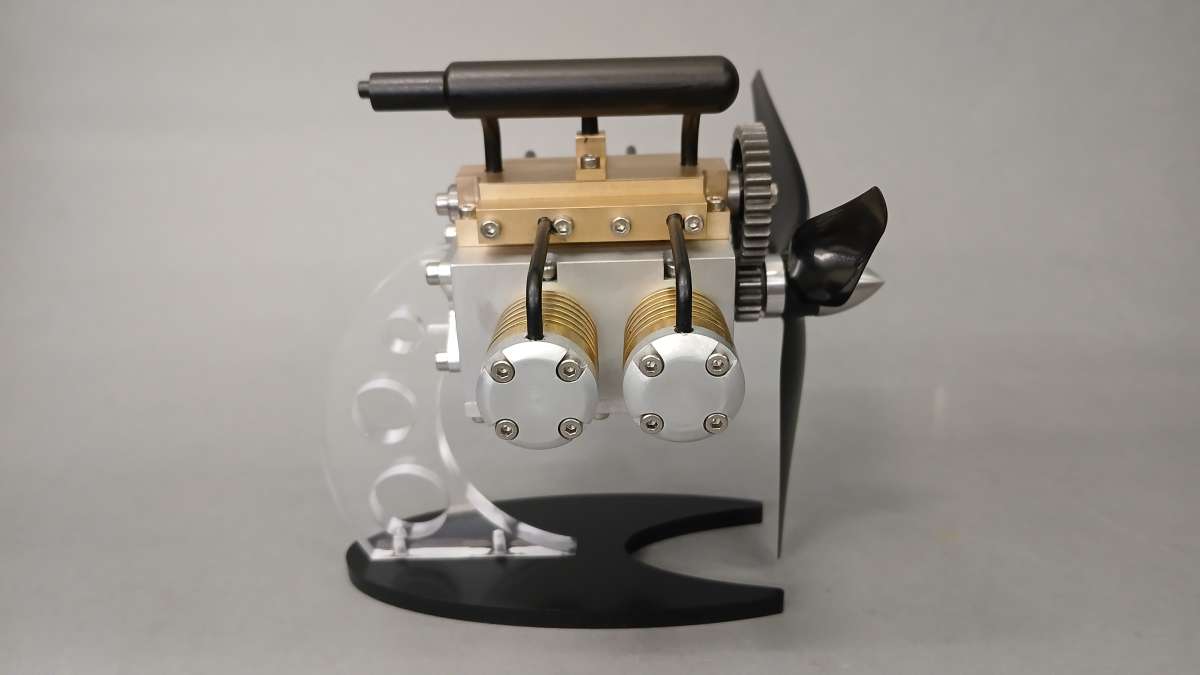
                  The drawings show hole positions in the crankcase for rear mounting of the engine but no details of a stand, so I made one up. The rear bearing carrier has a press fit specified but I did not want to do that as getting it out would mean pressing on the end of the crankshaft which could bend it. So I went with a push fit (actually held in the video above) and designed the stand bracket to ensure that the bearing carrier could not come out. It was shaped on the CNC

                  20261007_114032

                  And then the excess material use dto hold it by decked off on the manual mill

                  20261007_115922

                  The remaining parts were CNC cut from scraps of acrylic sheet

                  20261010_140150

                  20261011_091254

                  The exhaust “silencer” was the only part that did not have any errors, I added the missing pair of pipes and that was it. I think it actually sounds better with the silencer fitted.

                  20261011_091532

                  20261011_091559

                  20261011_091615

                  #868990
                  Grindstone Cowboy
                  Participant
                    @grindstonecowboy

                    Excellent work as usual!

                    Rob

                    #869004
                    renardiere7
                    Participant
                      @renardiere7
                      First class!

                    Viewing 9 posts - 1 through 9 (of 9 total)
                    • Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.

                    Latest Replies

                    Home › Forums › Stationary engines › Topics

                    Viewing 25 topics - 1 through 25 (of 25 total)
                    Viewing 25 topics - 1 through 25 (of 25 total)

                    View full reply list.