
What parting off tool and how to get parallel faces?

What parting off tool and how to get parallel faces?

Home Forums Beginners questions What parting off tool and how to get parallel faces?

Viewing 20 posts - 1 through 20 (of 20 total)
  • Author
    Posts
  • #861772
    interferencefit
    Participant
      @interferencefit

      Hi all,

      I’m gradually learning my way around my Myford 7. I’ve been doing a few small jobs, sometimes learning the hard way!

      Today’s project was making a 15mm thick aluminium spacer to fit a new CBN abrasive wheel to my bench grinder. I started with some aluminium round bar, bored the centre hole to a nice snug fit, and then turned the outside diameter and the end face. Since I don’t own a parting tool yet, I clamped the bar in a vice and cut the spacer off with a hacksaw.

      This is where things got tricky. I needed to face the rough, sawn side, but I found it incredibly difficult to chamber the short part back into the chuck so that it ran perfectly parallel. I only discovered how off it was after mounting my new wheel on the grinder and noticing some obvious run-out, which I traced back to the non-parallel faces of the spacer.

      I did try a few ways to square it up in the chuck. First, I tried using a centering tool in the tailstock, but the part was too short for that to be accurate. Then, I tried passing a piece of square stock through the chuck jaws to push the part flat against, but it was far too hit-and-miss. The experienced machinists among you are probably face-palming right now, which is exactly why I’m here for some guidance!

      I fully appreciate that parting off the piece would have prevented this issue entirely. This brings me to my first question: What parting tool should I buy?

      My lathe has the original Myford quick-clamp lever system (with the spring-loaded black block).


      AI  suggested a blade-style holder PARTING-SYSTEMS-FOR-SMALL-LATHESHowever, I also saw this traditional-style tool on the Myford website 10mm-Brazed-Tip-Parting-Tool-2I am not sure how the blade style works with my specific tool post, whereas the second one looks like my standard tools (though the blade doesn’t look very deep).
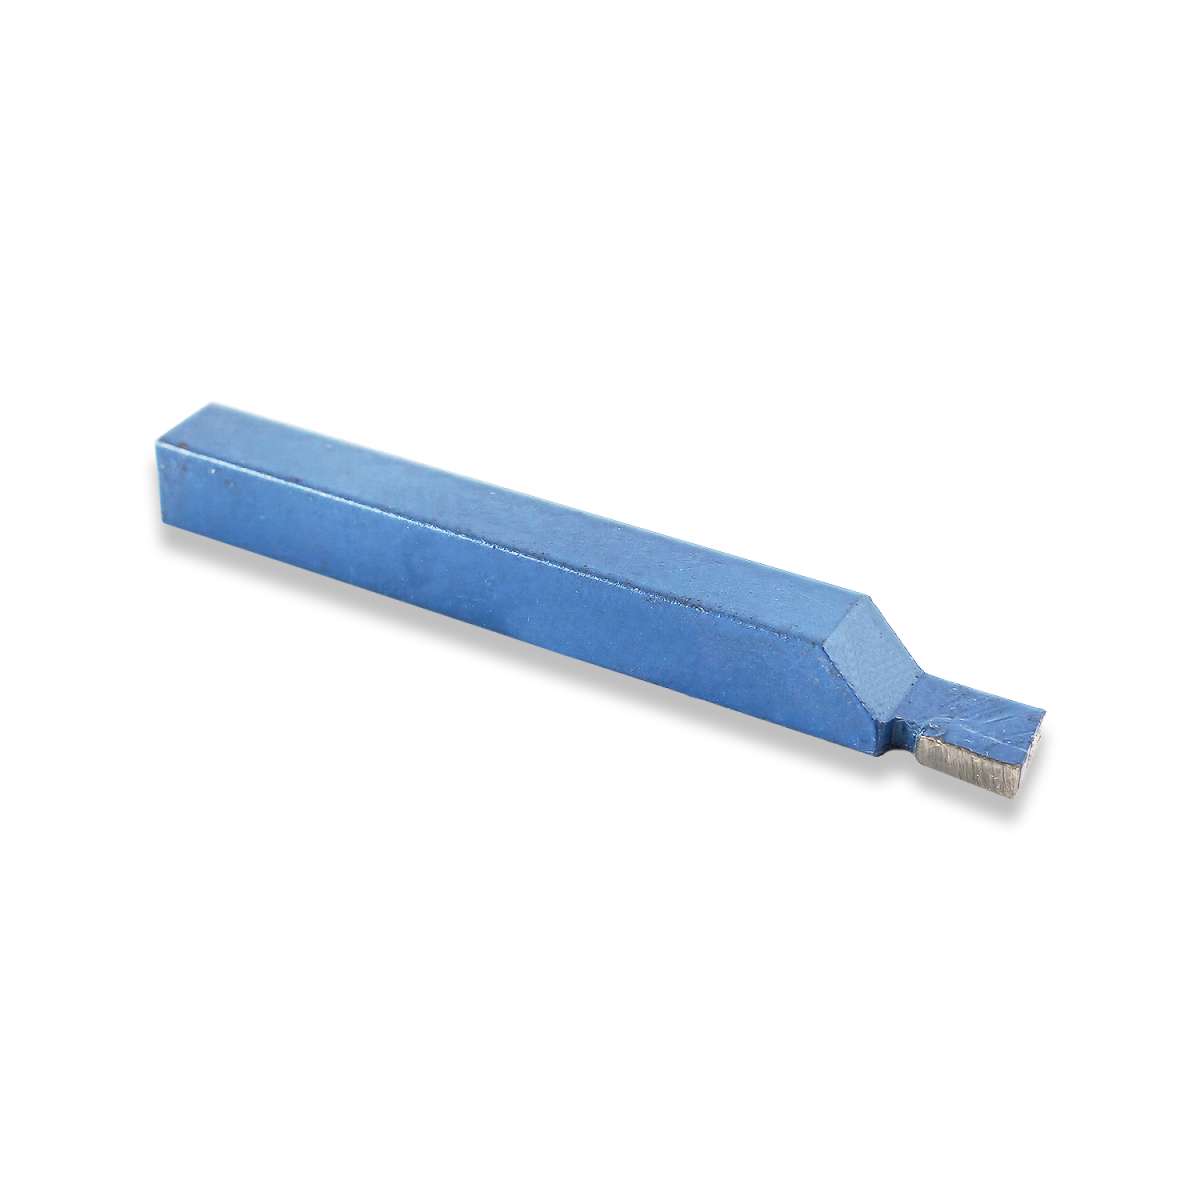
      Which style would you recommend for my setup?

      My second question is about technique: How do you accurately face the second side of a short, bored workpiece? If you have to flip a short part in the chuck to finish the opposite face, what is the best method to ensure the two faces stay perfectly parallel and true to the bore?

      Thanks in advance for any help!


      #861777
      Andrew Tinsley
      Participant
        @andrewtinsley63637

        I always move the saddle up to the chuck and adjust the parting off blade against the flat of the chuck face. This way you cannot get the parting off blade to be other than at right angles to the lathe axis.

        Of the two parting off tools that you show, the one with replaceable blades is best. However you will need to make an adapter to hold it in the traditional Myford tool holder. Unless anyone else has a smarter idea.

        Andrew.

        #861778
        JasonB
        Moderator
          @jasonb

          To save us repeating a lot of things have a look at this post from earlier in the week


          Parting off

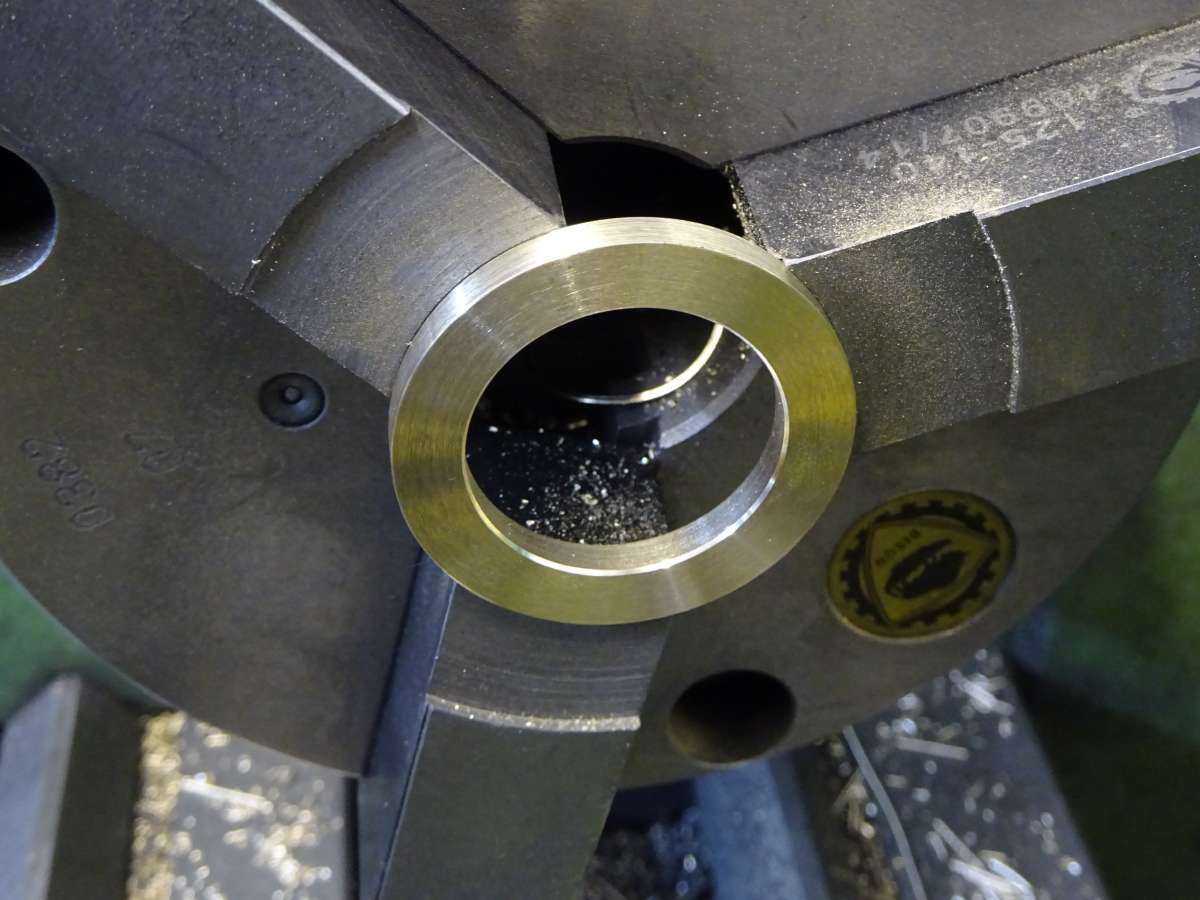
          regarding facing thin parts, a set of soft jaws are the ideal thing for this. You machine a shallow recess in the jaws the same diameter as your part and the back of the cut gives you something to push the good true face against.

          DSC02558

          #861779
          bernard towers
          Participant
            @bernardtowers37738

            If no soft jaws slide a piece of parallel steel through the jaws and push your spacer up to it, remove spacer and face off. An old bearing would make a good spacer but that would have to be left in place. Alternatively use a V tool to machine a vee in the work beyond your finished length, cut off then fit in chuck and use the v line to set true. There are so many ways to skin a cat!!

            #861780
            Hollowpoint
            Participant
              @hollowpoint

              Another method for facing thin washers, gears and other objects is to super glue the part to a faceplate or any flat surface. (Could just be a large bit of faced off bar). This is a common method used in watchmaking, though shellac was more traditional. Heat it up with a blowlamp to break the glue bond.

              As for parting tools, I like the carbide insert type with the “U” shaped grooved tips. Get the thinest one you can. 1-2mm ideally.

              #861781
              KEITH BEAUMONT
              Participant
                @keithbeaumont45476

                one trick I use is to use  the small moly magnets on  the jaws to pack out for holding thin parts  near the chuck

                #861783
                Howard Lewis
                Participant
                  @howardlewis46836

                  The HSS blade will probably last far longer than a brazed carbide tip (I seem to be able to chip them rematkably quickly.

                  In contrast to the HSS tapered blade that i was given when buying a “pre loved” ML7 some 40 years ago, used on its successor, and still not worn out.

                  With regard to holding, I would suggest turning up a holder (Collet), on the 3 jaw, with a recess to hold the washer, if soft jaws are not available.

                  The rear face of the “collet” will be square to the lathe axis, and the machined front face of the washer will seat against this, so that the hand sawn face can be faced parallel to the machined face.

                  HTH

                  Howard

                  #861786
                  ega
                  Participant
                    @ega

                    If you are sticking to the Myford “clog heel” tool holder then you might consider getting their tools mounted in a “boat” with an arcuate slot which gives height adjustment. The standard set included a parting tool.

                    When/if you upgrade, I wouldn’t rush to get a quick change holder. There are numerous designs for height adjustable holders which will serve you well while you decide how to go in future.

                    #861851
                    Clive Brown 1
                    Participant
                      @clivebrown1

                      Another way for the OP to solve his original problem is to use a back-stop in the lathe mandrel. Hemingway/Reeves market a kit specifically for the Myford 7. Making one is likely to be an interesting exercise. https://www.hemingwaykits.com/HK2010

                      #861874
                      martin haysom
                      Participant
                        @martinhaysom48469
                        On Howard Lewis Said:

                        The HSS blade will probably last far longer than a brazed carbide tip (I seem to be able to chip them rematkably quickly.


                        HTH

                        Howard

                        the cheap far east one’s chip very easily, the industrial standard one will last you forever, but the price i

                        #861892
                        Howard Lewis
                        Participant
                          @howardlewis46836

                          When I had the ML7, the standard Myford tool clamp was replaced by a Myford four way tool post.

                          Boat holders make height adjustment easy, but alter the rake angle as the cutting edge is adjusted.

                          Although many consider it a faff, I prefer to shim the tools to centre height. (Am not a lover of big top rake angles. The rear toolpost mounted HSS parting tool has zero rake, and very rarely causes problems)

                          Reputedly, QCTPs are a little less rigid that a four way, and not a lot quicker changing tools, unless there are a lot to do.

                          With four ways, front and rear, that causes me little problem, most of the time.

                          Usually only knurling or radius turning call for tool changes.

                          But you must optimise your set up.

                          Howard

                          #861906
                          ega
                          Participant
                            @ega

                            Howard Lewis:

                            Might you post a photo of your rear four way?

                            #861928
                            Fulmen
                            Participant
                              @fulmen

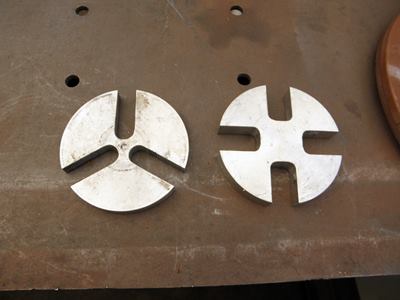
                              It’s not too hard to make a chuck spacer for these jobs:

                              https://www.homemadetools.net/forum/attachments/machinist-chuck-work-spacer-019.jpg-2079d1413923321


                              A simpler one would be to weld three flat pieces of steel to a bolt like a Y.

                              #861937
                              Chris Crew
                              Participant
                                @chriscrew66644

                                Some people confuse brazed finishing tools with parting tools which should be no more than about 2mm wide at the tip. Any tool wider than this is likely to be a finishing tool, intended to ‘rub’ the ‘thread’ off a longitudinally turned piece. A bit like setting a knife tool askew to rub to produce a finer finish. I seem to recall GHT or Sparey  had something to say about this.

                                #861938
                                ega
                                Participant
                                  @ega

                                  IIRC, GHT “set tool almost to rub”.

                                  #861957
                                  duncan webster 1
                                  Participant
                                    @duncanwebster1
                                    On bernard towers Said:

                                    ….


                                    An old bearing would make a good spacer but that would have to be left in place…

                                    Make sure the bearing is big enough that it won’t come out between the chuck jaws, or it could be flung across the workshop when you start the lathe. Or take it out first of course.

                                    I would have guessed the steps on the chuck jaws of a myford were less than 15mm, so just use the outside jaws


                                    #861961
                                    old mart
                                    Participant
                                      @oldmart

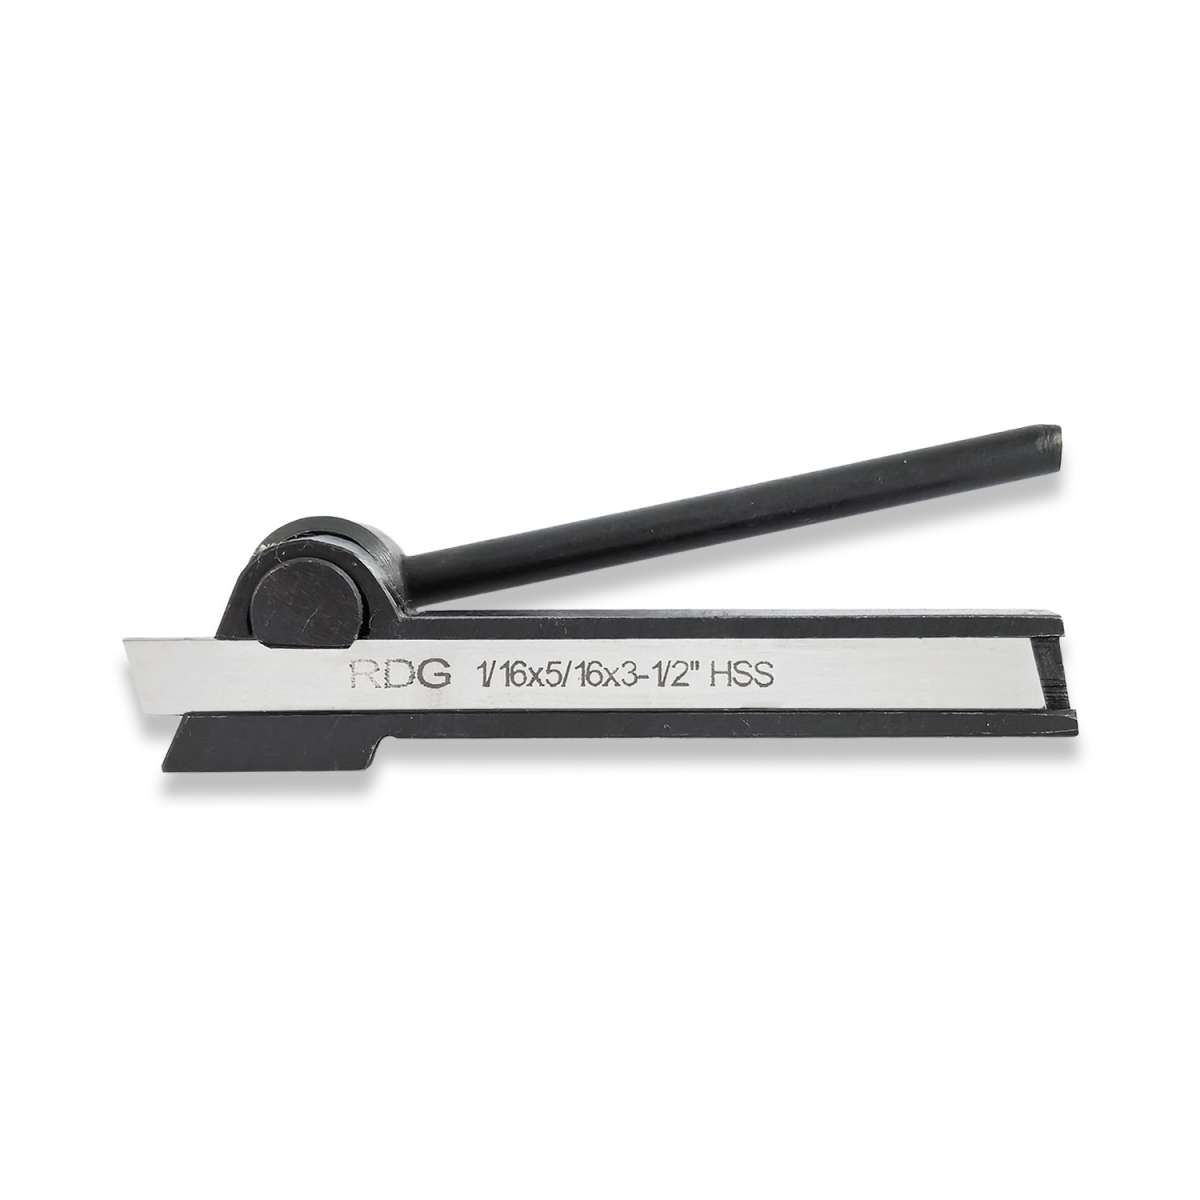
                                      For a beginner, the RDG blade and holder is much superior, and easy to keep sharp and on centre height. There are lots of printed plastic spacers to fit in chuck jaws on the market, you do need to find out if there are any to suit your chuck. Soft jaws are very good for holding difficult work and even when worn down can be drilled and tapped to hold new home made tops. With your chuck you would need to know the exact dimensions of the jaws including the “actual” pitch of the teeth before chancing buying soft jaws.

                                      #861971
                                      Howard Lewis
                                      Participant
                                        @howardlewis46836

                                        ega

                                        The  article about its construction was published in MEW 306, August 2021 and MEW 307, September 2021.

                                        It wan’t for the Myford, but a little larger, for my Engineers Tool Toom BL12-24 (Warco BH600 / Chester Craftsman etc lookalike), to look as much alike to the fronmt toolpost.

                                        It required no mods to the lathe itself, the base being bolted to the Cross Slide.

                                        So with different dimensions, or modifications, could be made for any lathe with Tee slots on the Cross Slide.

                                        It was made by laminating pieces from a 1 metre length of ground 3″ x1″ that I’d been given.

                                        Each of the laminations was machined differently from the others.

                                        The graphics team made a good job of tidying up my drawings of the G A and parts.

                                        If you want any extra help, just send me a message with your E mail address, and I do my best

                                        Howard

                                        #861974
                                        ega
                                        Participant
                                          @ega

                                          Howard:

                                          Thank you. I will turn up the MEW articles and bear in mind your kind offer.

                                          #862046
                                          old mart
                                          Participant
                                            @oldmart

                                            Another quick fix to get anything short running square, assuming the right side is already flat and not simply saw cut is to bring the tailstock up and use the end of the chuck with the jaws retracted to hold the work against.

                                          Viewing 20 posts - 1 through 20 (of 20 total)
                                          • Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.

                                          Latest Replies

                                          Home Forums Beginners questions Topics

                                          Viewing 25 topics - 1 through 25 (of 25 total)
                                          Viewing 25 topics - 1 through 25 (of 25 total)

                                          View full reply list.