
Making curved parts
Making curved parts
- This topic has 11 replies, 8 voices, and was last updated 16 September 2026 at 08:56 by
 roy entwistle.
 roy entwistle.
 Steve Huckins
 JasonB
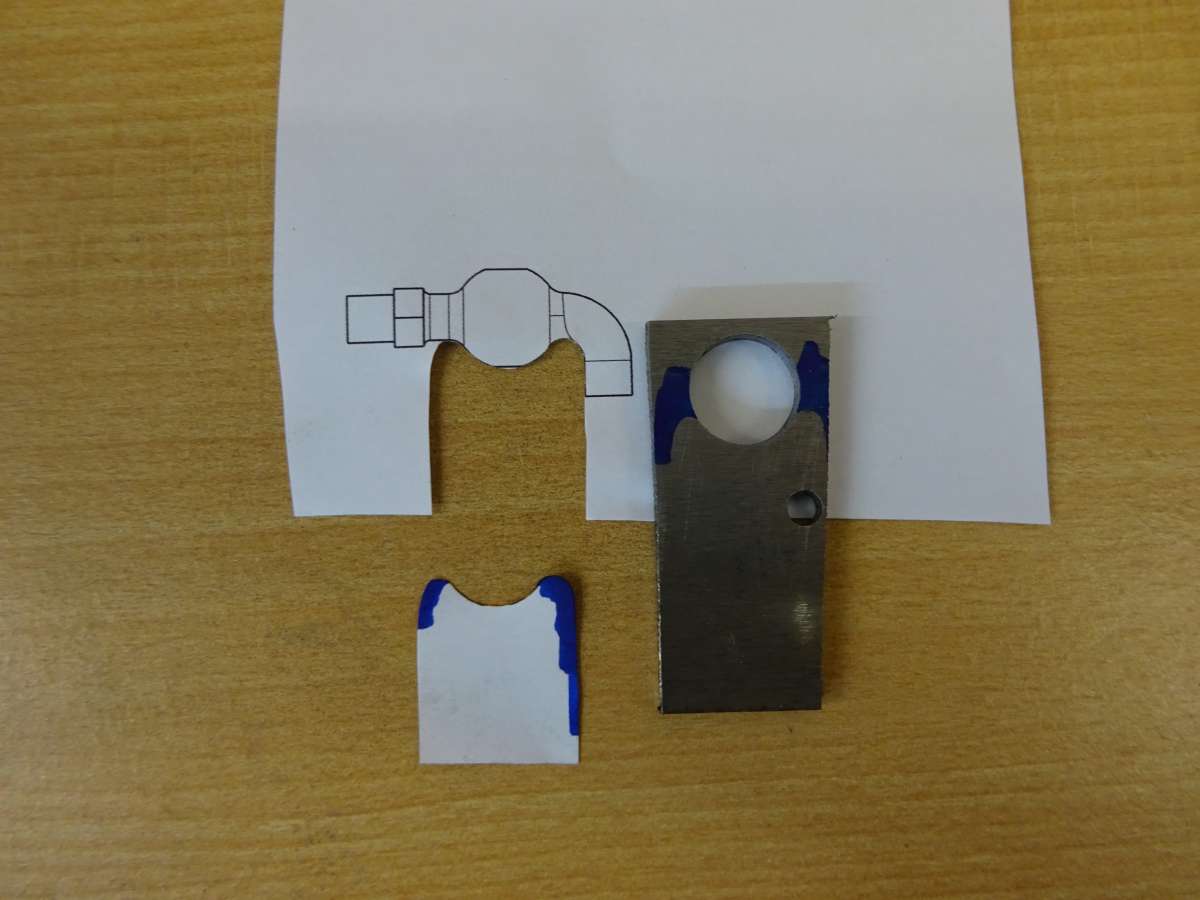
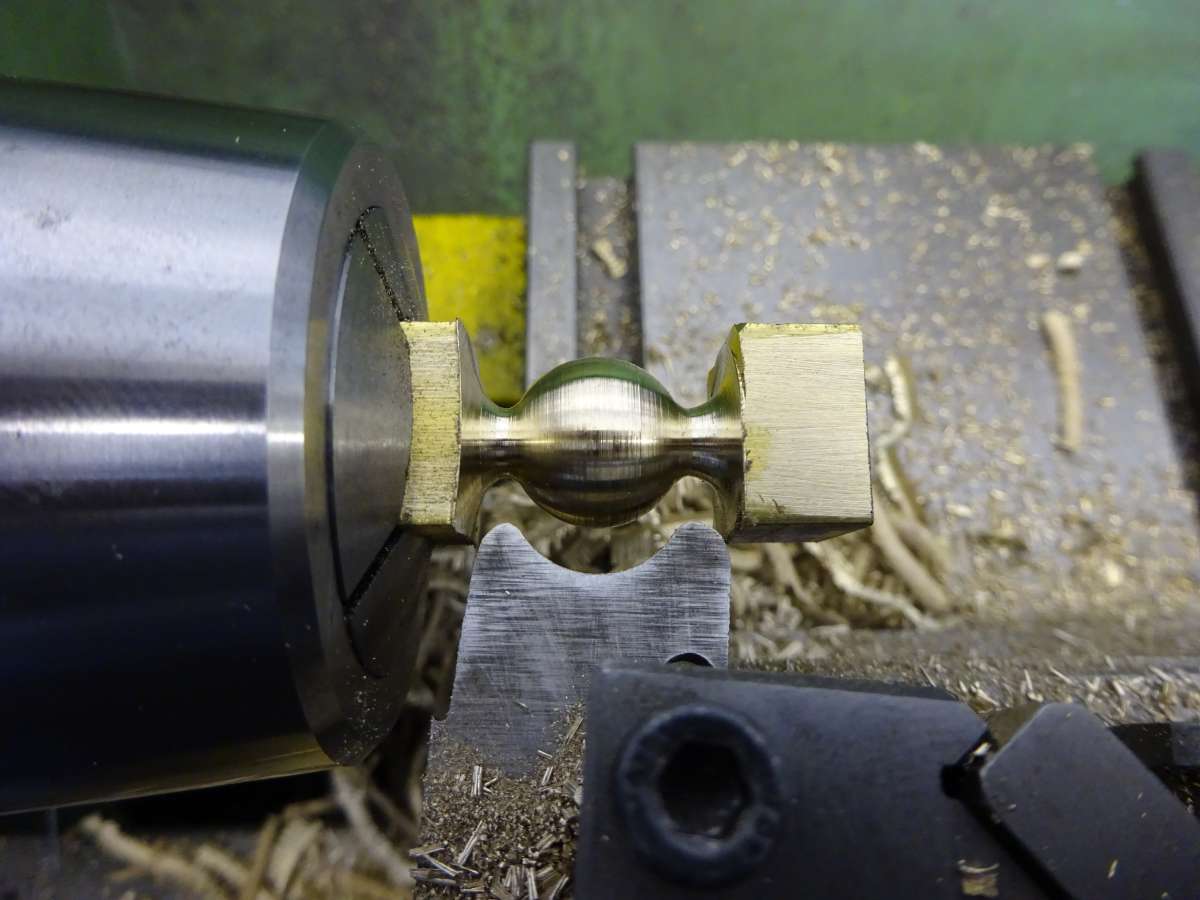
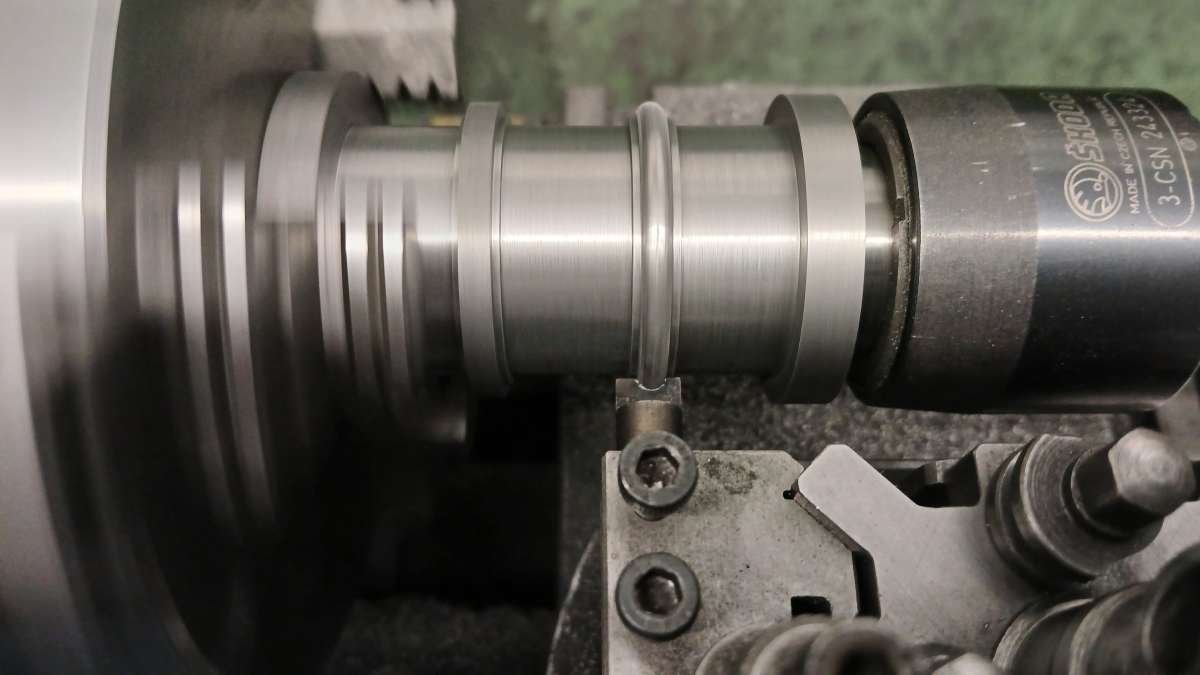
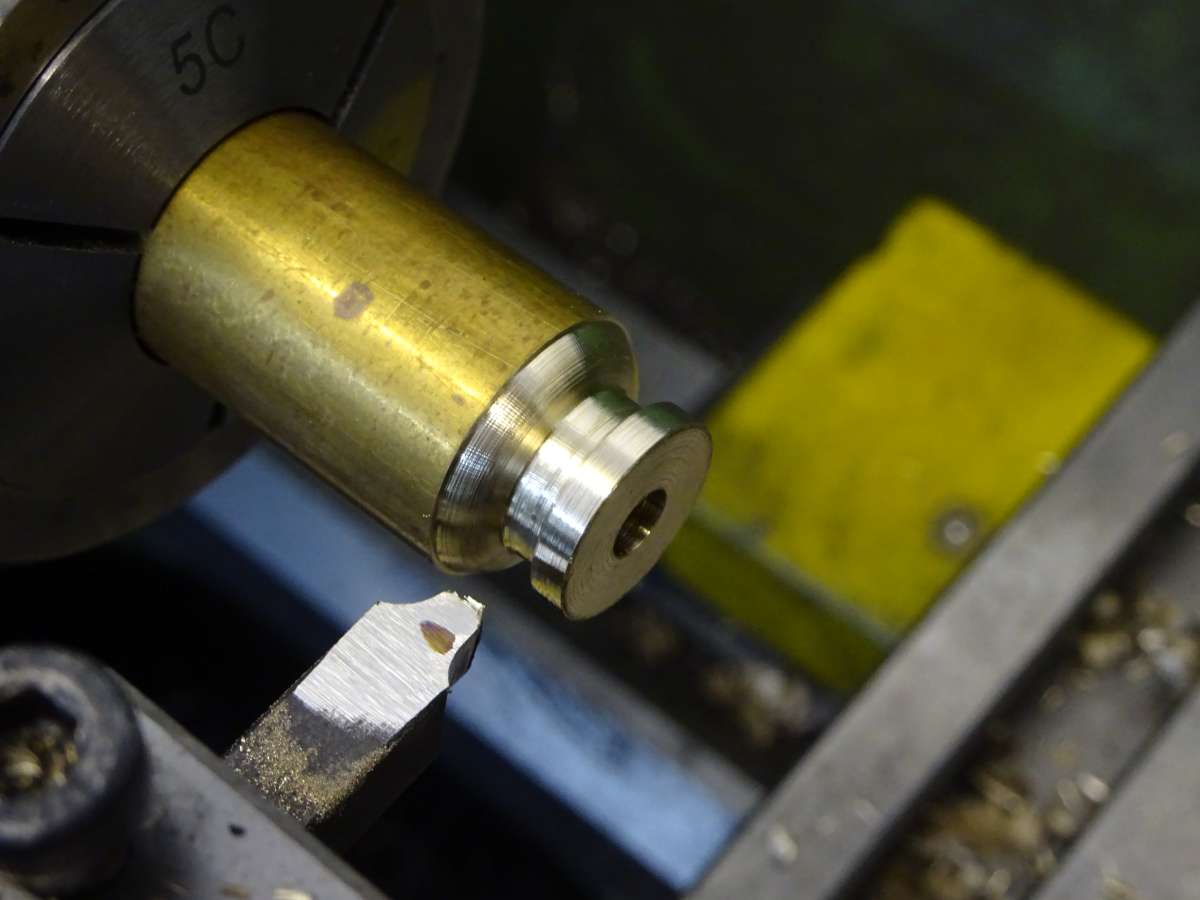
 noel shelley
 Mike Hurley
 Baz
 Chris Gunn
 Pete
 roy entwistle
- Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.
Latest Replies
-
- Topic
- Voices
- Last Post
-
-
Silver solder.
Started by:
Michael Callaghan
in: General Questions
- 9
-
9 October 2026 at 02:47
Speedy Builder5
-
Moving Targets
Started by:
Michael Gilligan
in: The Tea Room
- 6
-
9 October 2026 at 02:36
Michael Gilligan
-
Window weights as a source of cast iron.?
Started by:
File Handle
in: Materials
- 19
-
9 October 2026 at 00:49
Nigel Graham 2
-
Reverting An ML7 To Change-Wheels: Any Thoughts??
1
2
3
Started by:
Nigel Graham 2
in: Manual machine tools
- 20
-
9 October 2026 at 00:33
Nigel Graham 2
-
Dore Boring Bar set
Started by:
Andrew Tinsley
in: General Questions
- 2
-
9 October 2026 at 00:15
Nigel Graham 2
-
New Member
Started by:
starjump
in: Introduce Yourself – New members start here!
- 2
-
8 October 2026 at 23:07
starjump
-
Triangular Insert Tool
Started by:
James A
in: Workshop Tools and Tooling
- 10
-
8 October 2026 at 22:48
Bill Phinn
-
Angled d-bit / machinist reamer?
Started by:
Fulmen
in: Workshop Tools and Tooling
- 6
-
8 October 2026 at 22:41
Bazyle
-
Minnie Traction Engine – Damper Hinge Plate
Started by:
Dominic Bramley
in: Traction engines
- 6
-
8 October 2026 at 20:30
Dominic Bramley
-
Locomotion No 1 – plans
Started by:
Bob Wild
in: Help and Assistance! (Offered or Wanted)
- 5
-
8 October 2026 at 20:04
Bazyle
-
Tom Senior small vertical head axial play
Started by:
chris1984
in: Manual machine tools
- 3
-
8 October 2026 at 19:34
not done it yet
-
Gears
Started by:
Franco Convertini
in: General Questions
- 8
-
8 October 2026 at 19:07
Howard Lewis
-
Liney RV-2 Rescue
Started by:
JasonB
in: Stationary engines
- 2
-
8 October 2026 at 18:56
JasonB
-
Hello Everyone (New Member Introduction)
Started by:
cedricvale
in: Introduce Yourself – New members start here!
- 5
-
8 October 2026 at 18:47
Howard Lewis
-
Hello everyone
Started by:
andrew998
in: Introduce Yourself – New members start here!
- 4
-
8 October 2026 at 18:43
Howard Lewis
-
Canterbury lamb
Started by:
Michael Callaghan
in: General Questions
- 3
-
8 October 2026 at 17:55
noel shelley
-
Fusion CAD / CAM Problem
Started by:
Shaun Churchill
in: CAD – Technical drawing & design
- 5
-
8 October 2026 at 17:00
andrew998
-
Parkside Electronics
Started by:
Clive Steer
in: General Questions
- 8
-
8 October 2026 at 13:12
shayodon
-
Picomite Version 7 – better than Arduino?
Started by:
IanT
in: Electronics in the Workshop
- 7
-
8 October 2026 at 12:03
IanT
-
What Did You Do Today 2026
1
2
…
8
9
Started by:
JasonB
in: The Tea Room
- 53
-
8 October 2026 at 11:44
bernard towers
-
Tom Senior small vertical head axial play
Started by:
chris1984
in: Manual machine tools
- 1
-
7 October 2026 at 20:05
chris1984
-
A nice Lidl improvement … ULGD 5.0 E4
Started by:
Michael Gilligan
in: Electronics in the Workshop
- 3
-
7 October 2026 at 19:07
peak4
-
Leeky diverter valve on a ‘telephone’ style bath/shower mixer tap
Started by:
jon hill 3
in: Related Hobbies including Vehicle Restoration
- 9
-
7 October 2026 at 17:16
jon hill 3
-
Current Thoughts on 3 Phase Smart Meters
Started by:
Colin Heseltine
in: The Tea Room
- 5
-
7 October 2026 at 16:28
howardb
-
Where is it all going? Claude – CAD – product
Started by:
Mike Hurley
in: CAD – Technical drawing & design
- 9
-
7 October 2026 at 13:57
David Senior
-
Silver solder.
 Michael Callaghan
 Speedy Builder5
 Michael Gilligan
 File Handle
 Nigel Graham 2
 Andrew Tinsley
 starjump
 James A
 Bill Phinn
 Fulmen
 Bazyle
 Dominic Bramley
 Bob Wild
 chris1984
 not done it yet
 Franco Convertini
 Howard Lewis
 JasonB
 cedricvale
 andrew998
 noel shelley
 Shaun Churchill
 Clive Steer
 shayodon
 IanT
 bernard towers
 peak4
 jon hill 3
 Colin Heseltine
 howardb
 Mike Hurley
 David Senior