
End mill sharpening

End mill sharpening

Home › Forums › General Questions › End mill sharpening

Viewing 25 posts - 1 through 25 (of 34 total)
  • Author
    Posts
  • #864230
    petro1head
    Participant
      @petro1head

      Doesanyone know of somewhere I can send my end mills to to get sharpened or am I just better off buying new?

      #864233
      John Haine
      Participant
        @johnhaine32865
        #864241
        JasonB
        Moderator
          @jasonb

          Probably not worth it for smaller sizes 6mm and below. Might break even 8-10mm . Larger sizes you may save money over buying new.

          #864247
          not done it yet
          Participant
            @notdoneityet

            JB, Is that just for HSS or are you including solid carbide in your response?

            #864250
            petro1head
            Participant
              @petro1head

              Cheers John and Jason

              #864251
              noel shelley
              Participant
                @noelshelley55608

                As Jason has said small ones , not worth the effort. Bigger ones, possibly. Someone with a Clarkson T&C grinder may be able to help you for a few beer tokens ? Noel.

                #864254
                petro1head
                Participant
                  @petro1head
                  On noel shelley Said:

                  As Jason has said small ones , not worth the effort. Bigger ones, possibly. Someone with a Clarkson T&C grinder may be able to help you for a few beer tokens ? Noel.

                  Beer tokens sounds good to me


                  #864255
                  JasonB
                  Moderator
                    @jasonb

                    I can get carbide for the same sort of money FC-3 disposable HSS sells for so to me not worth it for either. Have not bought HSS milling cutters for several years now I just get carbide and use that on the manual mill as well as the CNC.

                    #864266
                    mgnbuk
                    Participant
                      @mgnbuk

                      Former work only used to have large diameter, long series end mills sharpened.

                      Large diameter here being 25mm or larger – anything smaller was more cost effective to buy new (Cutwel usually, occasionally MSC)

                      When Cromwell had local reps. (before they were taken over) we used to collect up half a dozen or so cutters & the rep took them away to get reground. Turnaround was about a fortnight.

                      Can’t recall how we got them done after the reps went, but do recall packing them up to be couriered somewhere.They didn’t need doing often, as roughing out was done with inserted cutters & the long HSS end mills were only used for full depth finishing passes where a good finish was required.

                      Nigel B.

                      #864342
                      Trevor Drabble 1
                      Participant
                        @trevordrabble1

                        Abbco Tool and Cutter grinders of Nottingham . They adjacent to the old Myford Nottingham factory.

                        #864361
                        JasonB
                        Moderator
                          @jasonb

                          It would be helpful if those suggesting grinding services could give an idea of what they have been charged which would make it a lot easier for Petrolhead to decide if he is better off buying new or getting things sharpened.

                          #864376
                          peak4
                          Participant
                            @peak4
                            On JasonB Said:

                            It would be helpful if those suggesting grinding services could give an idea of what they have been charged which would make it a lot easier for Petrolhead to decide if he is better off buying new or getting things sharpened.

                            It would also be handy if Petro1head said roughly where they live.
                            If near Buxton, they could come round, drink coffee, and learn to use a Quorn or Clarkson (with some poor home made tooling.
                            I might even learn something myself.

                            Bill

                            #864382
                            Nigel Graham 2
                            Participant
                              @nigelgraham2

                              Not just a Clarskon T&C Grinder. The Stent is designed for sharpening the cutting edges of fluted tool, too. I think so is the Quorn.

                              The Kennet won’t. It’s not designed to do so. It grinds the straight edges only.

                              #864392
                              Vic
                              Participant
                                @vic

                                I made a version of Harold Halls jig for sharpening the bottom of end mills. It works very well on larger end mills.

                                #864399
                                not done it yet
                                Participant
                                  @notdoneityet

                                  He is in Newcastle …… if he has not moved.

                                  #864483
                                  petro1head
                                  Participant
                                    @petro1head

                                    Cheers NDIY. Not moved, still in Newcastle upon Tyne which is miles away from everyone

                                    #864512
                                    bernard towers
                                    Participant
                                      @bernardtowers37738

                                      For those of us with a cutter grinder its another skill to be learned and enjoyed, its not all about the money.IMHO. Oh and the pleasure of using a sharp cutter.

                                      #864516
                                      Nigel Graham 2
                                      Participant
                                        @nigelgraham2

                                        One point:

                                        Petrolhead –

                                        Did mean sharpening the flute edges as well as the radial ones? An end-mill is supposed to cut on its side as well as end, and many of the suggestions here refer to sharpening only the end.

                                        #864525
                                        Julie Ann
                                        Participant
                                          @julieann

                                          As Nigel says, despite the name endmills are designed to cut on the side. The end teeth are ground slightly hollow and take no part in normal sideways cutting. The end only cuts when the endmill is plunging, or ramping, into the work.

                                          Many newer types of endmill have one tooth on the end that goes to the centre, so in theory the endmill can plunge cut. Albeit at a much reduced feedrate as the cutting speed in the centre is zero when plunging. The tooth reaching the centre is really intended to improve ramping and helical cuts on a CNC mill.

                                          Julie

                                          #864577
                                          petro1head
                                          Participant
                                            @petro1head
                                            On Julie Ann Said:

                                            As Nigel says, despite the name endmills are designed to cut on the side. The end teeth are ground slightly hollow and take no part in normal sideways cutting. The end only cuts when the endmill is plunging, or ramping, into the work.

                                            Many newer types of endmill have one tooth on the end that goes to the centre, so in theory the endmill can plunge cut. Albeit at a much reduced feedrate as the cutting speed in the centre is zero when plunging. The tooth reaching the centre is really intended to improve ramping and helical cuts on a CNC mill.

                                            Julie

                                            On Nigel Graham 2 Said:

                                            One point:

                                            Petrolhead –

                                            Did mean sharpening the flute edges as well as the radial ones? An end-mill is supposed to cut on its side as well as end, and many of the suggestions here refer to sharpening only the end.

                                            Yes, thinking of the end to get sharpened


                                            #864587
                                            Martin Johnson 1
                                            Participant
                                              @martinjohnson1

                                              A good few years ago, I got a price in for a local(ish) company to sharpen a batch of 20 15mm endmills (3 fluters).  It was cheaper to go and buy new.  Given that setting up a T&C grinder is most of the battle, and most people won’t possess that many cutters in a single size, the only routes left are buy new or get your own grinder.

                                              Martin

                                              #865348
                                              petro1head
                                              Participant
                                                @petro1head

                                                I finally got my finger out and spoke to Dan at Raynor

                                                i asked if I could post the costs.  Obviously prices may change,

                                                there are 2 cost: full sharpen and end only.  The prices are for carbon steel, HSS will be slightly cheaper.

                                                8-10mm £8.84 £6.34

                                                10.1-12 12.25. 10.07

                                                12.1-16 15.17 11.16

                                                16.1-20 18.97. 13.15

                                                I have asked for a price for HSS end only 10×2, 12×2, 14×3, 16×3, 18, 20 and will let you know so you get an idea for bulk

                                                #865428
                                                David George 1
                                                Participant
                                                  @davidgeorge1

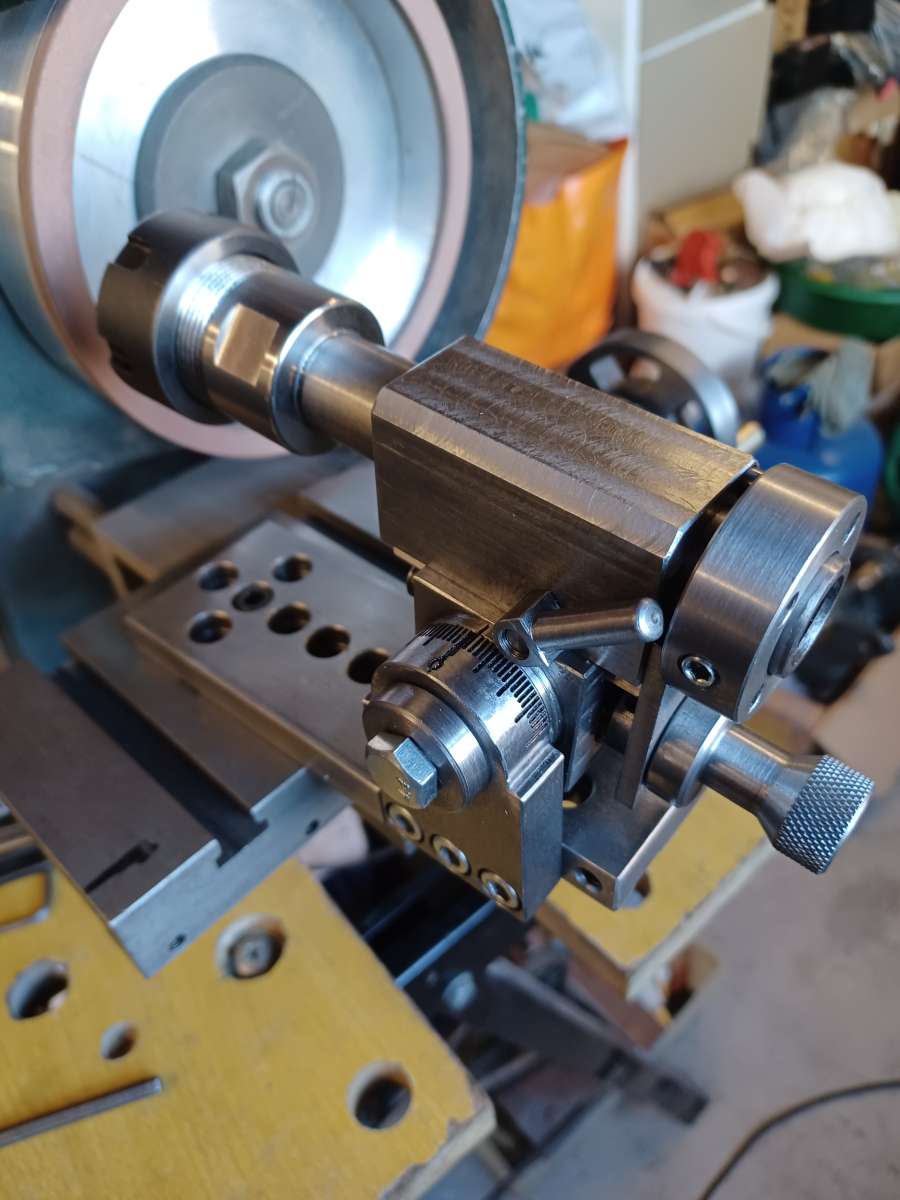
                                                  I have started grinding my own sometimes as mainly bottom of cutters need sharpening or drill edge needs a better than hand eye coordination, as I get older. The Grinder that I modified does most sharpening. I made the tool holder my self and gets me out of a hole or two occasionally.

                                                  20250228_143155

                                                  I can grind most angles and also sides of milling cutters quite acceptable and also mod cutters to cut a taper if i wish but it takes time. I ground a carbide endmill to cut a slot with a 5 degree angle to make a lead in on a square aperture with round corners in tough steel block for a punch guide for a jewellery friend.

                                                  David


                                                  #865433
                                                  Nigel Graham 2
                                                  Participant
                                                    @nigelgraham2

                                                    Neat design, David.

                                                    Can you sharpen 3-flute as well as 2 and 4 flute cutters?

                                                    I find the Worden T&C grinder is limited to 2 and 4 edges only, as its indexing is by the tool-holder block’s square cross-section, but a second block of equilateral-triangular section to fit the existing guides would overcome that.

                                                    #865483
                                                    David George 1
                                                    Participant
                                                      @davidgeorge1

                                                      I index the teeth for the end by using aa collar with holes in. And by unclamping the side clamp pull back the collet holder, rotate to next hole, push back to depth and re clamp and wind over face of grinding wheel and repeat till all faces are ground. II haven’t made a collar for three hole yet but should I need one it wont take very long. There is a dowel in the end of the body and aa set of holes in the collar which is held on by a grub screw to the shaft of a collet set which holds the cutter or drill and also sets depth when sliding out off the location dowel rotate and push back to locate next hole ready to sharpen next face.

                                                      David

                                                    Viewing 25 posts - 1 through 25 (of 34 total)
                                                    • Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.

                                                    Latest Replies

                                                    Home › Forums › General Questions › Topics

                                                    Viewing 25 topics - 1 through 25 (of 25 total)
                                                    Viewing 25 topics - 1 through 25 (of 25 total)

                                                    View full reply list.