
The lazy man’s fly cutter

The lazy man’s fly cutter

Home › Forums › Workshop Tools and Tooling › The lazy man’s fly cutter

Viewing 13 posts - 1 through 13 (of 13 total)
  • Author
    Posts
  • #868607
    Sonic Escape
    Participant
      @sonicescape38234

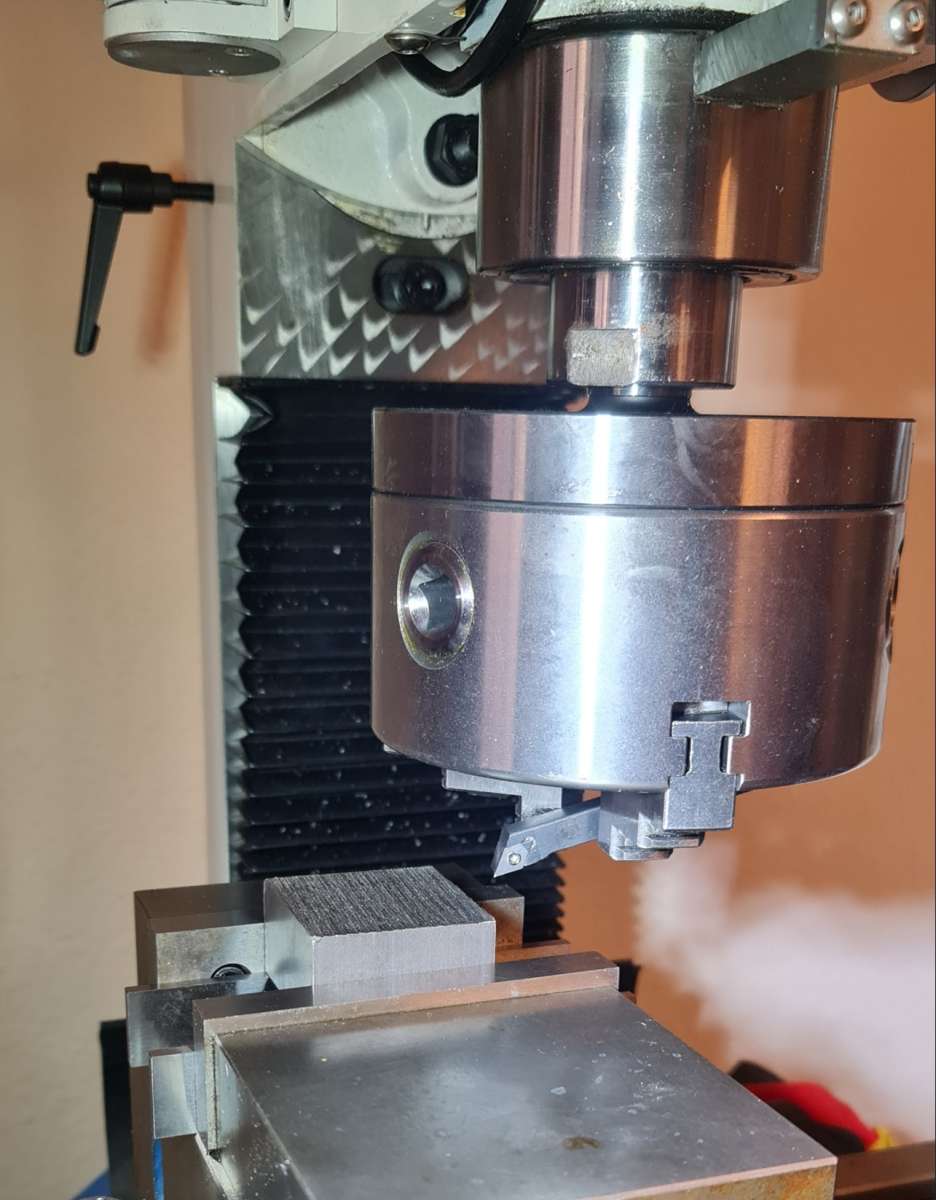
      I’ve wanted to make a fly cutter for a long time but never had the time. Once again, it turns out that laziness leads to optimal solutions. I have a faceplate with a MT3 mount for a 125mm chuck, which I use on my lathe. This morning, it occurred to me to move the chuck to the milling machine and clamp a cutter into it. It works really well!


      ssss

      #868615
      Clive Foster
      Participant
        @clivefoster55965

        The flywheel effect of the heavy chuck probably improves finish and keeps the cutter more stable as it inters the cut. Which would seem to be an advantage on smaller machines.

        Not completely convinced about pull out resistance with the cutter clamped canter wise between the three jaws tho’.

        Clive

        #868630
        Baz
        Participant
          @baz89810

          Same as Clive, not totally convinced about clamping tool like that but top marks for the flywheel effect of the chuck.

          #868633
          Dave Halford
          Participant
            @davehalford22513

            I’m not totally convinced that dodge could be used on a machine with plastic gears very often given the inertia involved.

            #868640
            Robert Atkinson 2
            Participant
              @robertatkinson2

              I’d be concerned about the cutter being flung out too. A bit of round bar with an angled slot milled in it and two or 3 set  screws would not be hard to make and more secure.

              Robert.

              #868643
              Andrew Crow
              Participant
                @andrewcrow91475

                Before I had a milling machine I used that method on lathe with the job bolted to the cross slide or vertical slide, never had a problem with the tool coming out of the chuck.

                Andy

                #868646
                JasonB
                Moderator
                  @jasonb

                  For the 40 plus years I have been model engineering I have regularly seen that method suggested as a way to hold work in the lathe so don’t see any more risk of a tool flying out as there would be with a workpiece. Many here seem to suggest Spary’s book to beginners and he was up for using that method.

                  Used that method to grip work a few times myself

                  As for plastic gears I’m inclined to think the opposite. A lightweight flycutter will stop and start as the tool enters and leaves the cut which loads and unloads the gears. As mentioned by others the innertia in the heavy chuck will go some way to damping out that stop start load.

                  #868652
                  Sonic Escape
                  Participant
                    @sonicescape38234

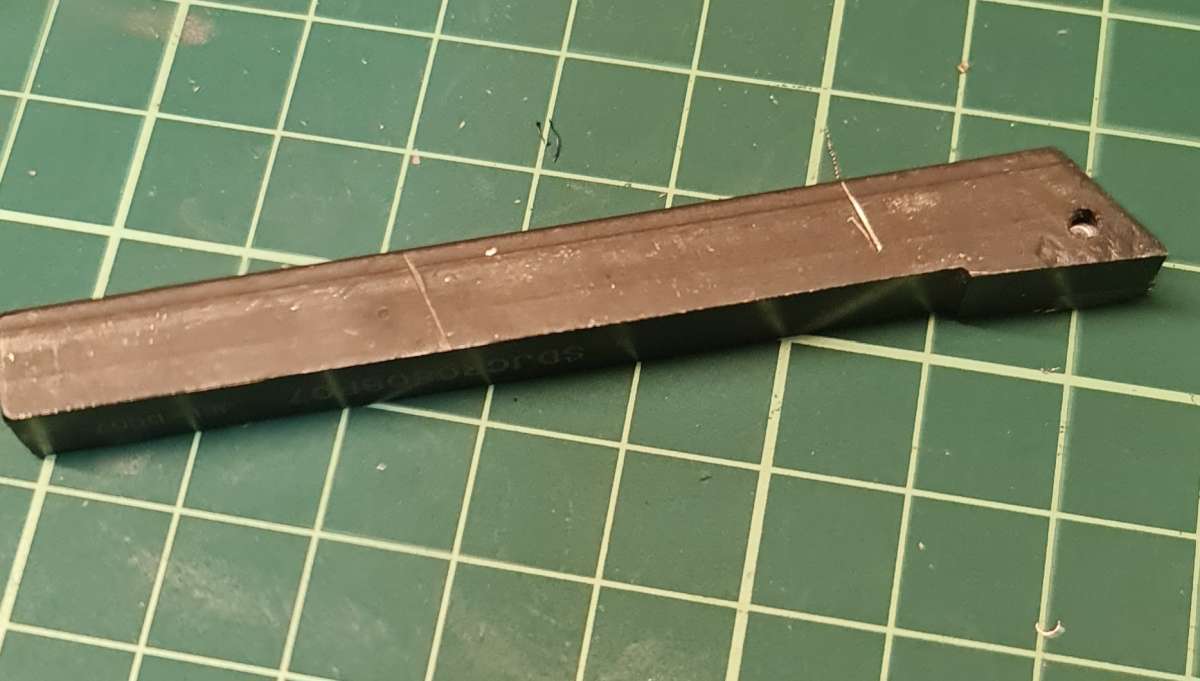
                    The milling machine is HBM BF28, it has a belt, no gears. So no problem there. I was also suspicious at first about whether it was safe. I never went beyond 400rpm. But it looks like the chuck jaws are biting in the tool. See the two lines.

                    ssss2

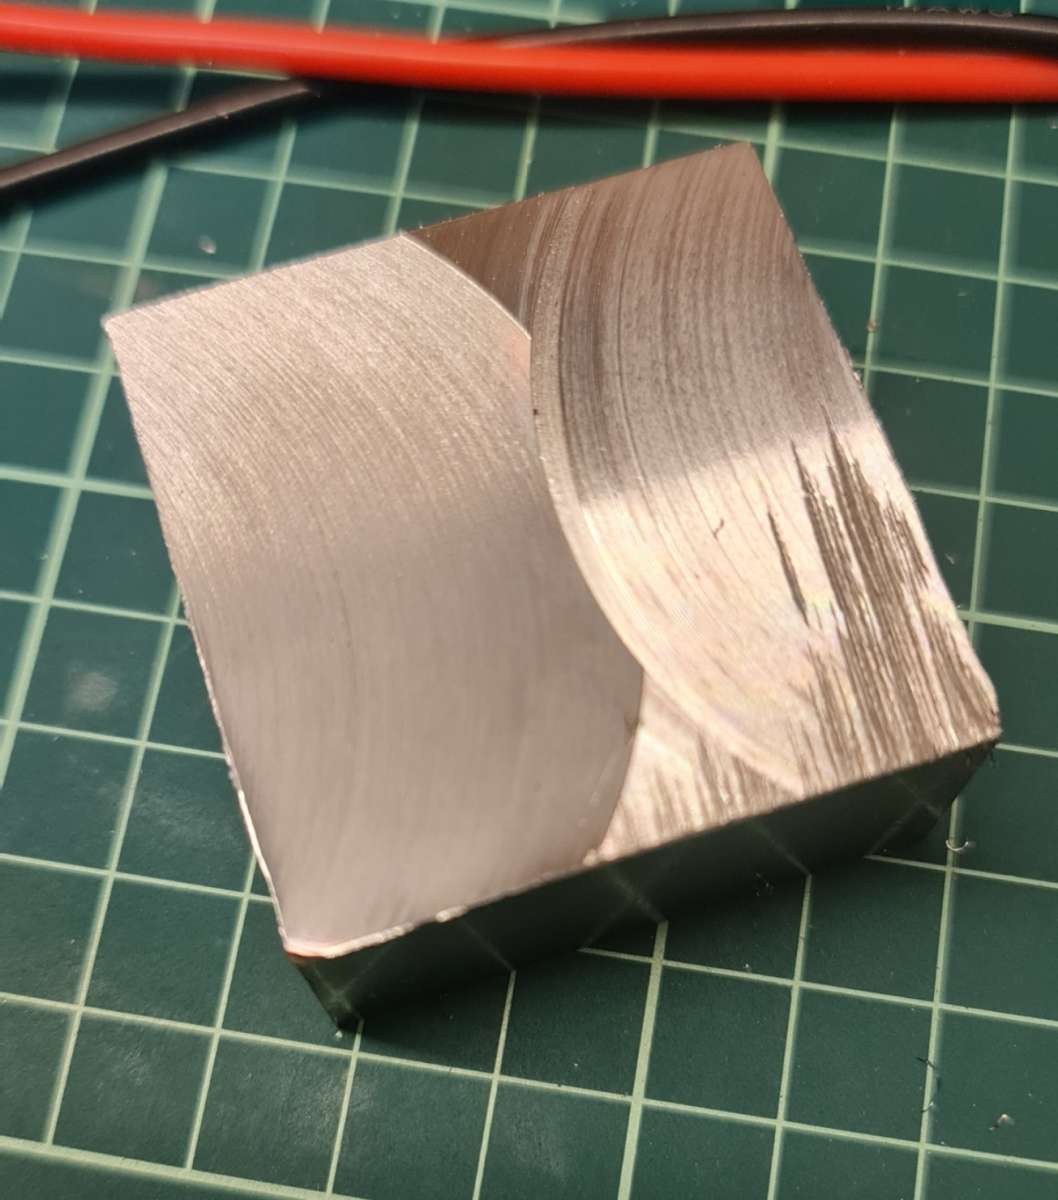
                    Also the cutting forces are small. It should be safe. This is a C45 steel cube. Thee feed rate was not optimal. But still the left part feels very smooth. The right half was done with wrong turning direction. And resulted also in a brocken tool tip.

                    ssss1

                    #868653
                    Clive Foster
                    Participant
                      @clivefoster55965

                      The, very experienced, machinist who introduced me to such canter wise clamping of square or rectangular stock in three jaw chuck was adamant that the material should sit back tight against the chuck body and not project more than the external jaw depth. He said that if that advice was not religiously followed it was certain that a workpiece would self eject sooner or later.

                      He considered this an undesirable occurrence.

                      I guess it’s like so many things. You can push the envelope a bit if you know what you are doing and take appropriate care in setting up. Going in all gang ho and willy nilly is asking for trouble. Which may, or may not, ever find you.

                      For sure its easier to get a secure, well aligned hold when the chuck is in the lathe with a secure base to work against than when its pointing down on a mill spindle or just a loose chuck and arbor.

                      I’ve only every used the idea for squaring up smallish material or sorting out rodent nibble quality cuts on an end. Always gone fine for me but I made sure to take that extra bit of care setting up and verify tightness after the first three or four cuts. Whether or not I ever encountered things actually working loose has long faded from memory. For sure I’ve never used the technique this century.

                      Clive

                      #868656
                      Tony Pratt 1
                      Participant
                        @tonypratt1

                        I personally wouldn’t abuse a fairly new 3 jaw chuck like that but each to their own.

                        Tony

                        #868667
                        Dave Halford
                        Participant
                          @davehalford22513
                          On JasonB Said:

                          For the 40 plus years I have been model engineering I have regularly seen that method suggested as a way to hold work in the lathe so don’t see any more risk of a tool flying out as there would be with a workpiece. Many here seem to suggest Spary’s book to beginners and he was up for using that method.

                          Used that method to grip work a few times myself

                          As for plastic gears I’m inclined to think the opposite. A lightweight flycutter will stop and start as the tool enters and leaves the cut which loads and unloads the gears. As mentioned by others the innertia in the heavy chuck will go some way to damping out that stop start load.

                          I was thinking about the start up not the cut.

                          #868671
                          JasonB
                          Moderator
                            @jasonb

                            I don’t see it as much different to a plastic geared minilathe starting up, they seem to manage that quite a few times without stripping the gears. Probably less load actually, as the toolbit is minimal compared to the possible weight of a large piece of material in the chuck when it is mounted on the lathe.

                            Although belted I regularly used to use the lathe chuck on the milling head of my Unimat 3 motor and pulley/belt arrangement was exactly the same so no difference in load.

                            Big chucks are more likely to draw more current on startup so motor/board would be more of a possible area of worry than the gears.

                            I assume that the chuck used on a smaller plastic geared mill will be in proportion to that shown so 80 to 100mm

                            #868677
                            old mart
                            Participant
                              @oldmart

                              A left handed lathe tool would enable normal forward spindle rotation. I would be concerned about the sideways uneven loading on the poor chuck.

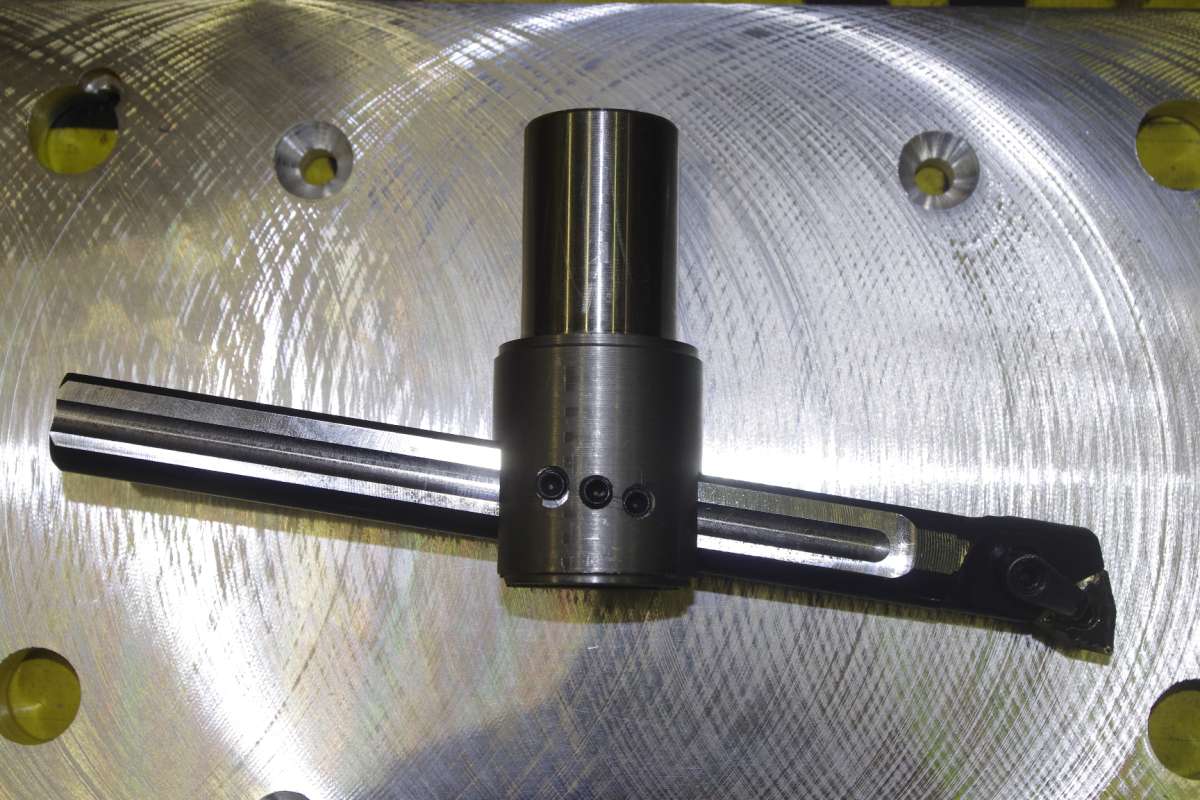
                              My effort on the subject of flycutting was a 20mm lefthanded boring bar with a WNMG08 or WNGT08 insert with a 30mm shank to fit in a_IGP3584n R8 to er40 collet.

                            Viewing 13 posts - 1 through 13 (of 13 total)
                            • Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.

                            Latest Replies

                            Viewing 25 topics - 1 through 25 (of 25 total)
                            Viewing 25 topics - 1 through 25 (of 25 total)

                            View full reply list.