
Warco WM180 Autofeed Speed

Warco WM180 Autofeed Speed

Home › Forums › Workshop Tools and Tooling › Warco WM180 Autofeed Speed

Viewing 25 posts - 1 through 25 (of 37 total)
  • Author
    Posts
  • #867244
    James A
    Participant
      @jamesalford67616

      The autofeed rate, as delivered, on my WM180 seems to be rather high. I have looked at the gearing and I  think that it is at the finest feed already.

      Does anyone know whether the feed rate can be reduced?


      James

      #867274
      Pete
      Participant
        @pete41194

        Google seems to indicate it can be done by changing the gear ratio. That should be something that’s in your lathe manual I would think.

        #867277
        bernard towers
        Participant
          @bernardtowers37738

          Reading the manual it looks like you get 3.5 thou per rev so how low do you want to go? Perhaps you tool tips are a bit sharp?

          #867284
          James A
          Participant
            @jamesalford67616
            On Pete Said:

            Google seems to indicate it can be done by changing the gear ratio. That should be something that’s in your lathe manual I would think.

            You can do that, but any change looks like it will increase the feed rate, not slow it down.

            On bernard towers Said:

            Reading the manual it looks like you get 3.5 thou per rev so how low do you want to go? Perhaps you tool tips are a bit sharp?

            It seems quicker than my  old lathe, although I have not measured the different rates.


            James

            #867287
            duncan webster 1
            Participant
              @duncanwebster1

              Looks like James has had the same problem I had, content of message disappeared

              #867291
              James A
              Participant
                @jamesalford67616
                On duncan webster 1 Said:

                Looks like James has had the same problem I had, content of message disappeared

                It did…

                On Pete Said:

                Google seems to indicate it can be done by changing the gear ratio. That should be something that’s in your lathe manual I would think.

                You can change it, but I cannot see how to make it slower.

                On bernard towers Said:

                Reading the manual it looks like you get 3.5 thou per rev so how low do you want to go? Perhaps you tool tips are a bit sharp?

                My old lathe’s feed rate was 1.5 thou per turn sothe Warco seems very quick in comparison. I am using carbide tips.

                James

                #867308
                JasonB
                Moderator
                  @jasonb

                  Looking at the manual there does not seem to be much room left on the banjo to get any larger gears in as the 72T is at the top of the banjo slot. Also I expect the use of the two 80T and 72T gears along with the smaller ones are using up all the supplied gears at the extreams of the available selection.

                  0.0035″ is only a bit coarser than I generally use, my finishing feed of choice is 0.0025″ and roughing 0.005″

                  If your cutting tool has a point then you will get what is in effect a fine screw thread, round the corner slightly on a slip stone or diamond slip and that should give a smoother finish assuming tools are sharp. Inserts will already come with teh tip radius.

                  #867316
                  James A
                  Participant
                    @jamesalford67616

                    Third time lucky……………….

                    On 30 September 2026 at 22:10 Pete Said:
                    Google seems to indicate it can be done by changing the gear ratio. That should be something that’s in your lathe manual I would think.

                    Yes, it can be changed, but I cannot see any scope for slowing the rate. I am not sure whether I am misreading the manual, though.


                    On 30 September 2026 at 22:14 bernard towers Said:
                    Reading the manual it looks like you get 3.5 thou per rev so how low do you want to go? Perhaps you tool tips are a bit sharp?

                    My old Flexispeed had a feed rate of 1.5 thou per turn, so the Warco does seem rather quick. My HSS tool was sharp, but the tip to which I changed was as supplied.


                    On 1 October 2026 at 06:58 JasonB Said:
                    Looking at the manual there does not seem to be much room left on the banjo to get any larger gears in as the 72T is at the top of the banjo slot. Also I expect the use of the two 80T and 72T gears along with the smaller ones are using up all the supplied gears at the extreams of the available selection.

                    0.0035″ is only a bit coarser than I generally use, my finishing feed of choice is 0.0025″ and roughing 0.005″

                    If your cutting tool has a point then you will get what is in effect a fine screw thread, round the corner slightly on a slip stone or diamond slip and that should give a smoother finish assuming tools are sharp. Inserts will already come with teh tip radius.

                    Thank you, Jason. That comparison of the rates that you use is helpful. Yes: I was getting a fine screw thread with my HSS tool, but the tip gave a finer finish.

                    I shall have a another look at the supplied gears as there is a bag of them that I have not really explored in detail yet.

                    James

                    #867332
                    James A
                    Participant
                      @jamesalford67616

                      Jason.

                      In reply to your seemingly vanished post, my WM180 has a tpi of 13 on the leadscrew.

                      James

                      #867335
                      John Haine
                      Participant
                        @johnhaine32865

                        13 tpi, really? Could it be 2mm?

                        #867348
                        JasonB
                        Moderator
                          @jasonb

                          No, looking at the gear train 12tpi on an imperial lathe gives 0.0034722″ which would be the rounded up 0.0035″/rev

                          Metric machine has a 2mm pitch, confirmed by the gear train giving 0.083mm/rev

                          #867429
                          James A
                          Participant
                            @jamesalford67616


                            On John Haine Said:

                            13 tpi, really? Could it be 2mm?

                            I have checked and it is nearer to 1.5mm pich.

                            #867463
                            James A
                            Participant
                              @jamesalford67616

                              It seems that when I try to post anything using my phone, the message disappears.

                              I checked last night and the pitch of the leadscrew, in mm, is a little over 1.75, as best as I can measure. It is a little fiddly to measure as there is a springy concertina cover over the leadscrew.

                              James.

                              #867467
                              Niels Abildgaard
                              Participant
                                @nielsabildgaard33719
                                #867480
                                Michael Gilligan
                                Participant
                                  @michaelgilligan61133
                                  On James A Said:

                                  It seems that when I try to post anything using my phone, the message disappears.

                                  I checked last night and the pitch of the leadscrew, in mm, is a little over 1.75, as best as I can measure. It is a little fiddly to measure as there is a springy concertina cover over the leadscrew.

                                  James.

                                  Measure the actual movement of the saddle, over some conveniently large number of turns of your leadscrew.

                                  MichaelG.

                                  #867484
                                  Michael Gilligan
                                  Participant
                                    @michaelgilligan61133

                                    Posting problem persists … Grrr!!

                                    #867488
                                    JasonB
                                    Moderator
                                      @jasonb

                                      I did let the back room boys know yesterday morning and they are working on it

                                      #867492
                                      Michael Gilligan
                                      Participant
                                        @michaelgilligan61133

                                        Thanks, Jason

                                        MichaelG.


                                        .

                                        IMG_2112

                                        .


                                        #867518
                                        Neil A
                                        Participant
                                          @neila

                                          As far as I am aware, the lead screw on the WM180 lathe is 2mm pitch on the metric model and 12TPI on the imperial model. I don’t think there were any other options produced.

                                          Check the dials on the cross-slide and saddle, these will indicate if the graduations are in millimetres or inches. Most newer machines are metric and would have a 2mm pitch lead screw.

                                          The 0.083mm/rev converts to 0.0033″/rev, so midway between Jason’s feed rates. I’m afraid you have been spoilt by the Flexispeed’s 0.0015″/rev. The 0.04mm radius on my inserts usually produces an acceptable turned finish, depending on the actual material and whether any cutting oil is used.

                                          Neil

                                          #867524
                                          not done it yet
                                          Participant
                                            @notdoneityet

                                            The easy way, if there is a handle to advance/retract the carriage is to measure the carriage movement over multiple lead-screw revolutions and then do a tiny bit of maths to find the distance travelled per revolution of the led-screw.

                                            #867563
                                            Nicholas Farr
                                            Participant
                                              @nicholasfarr14254

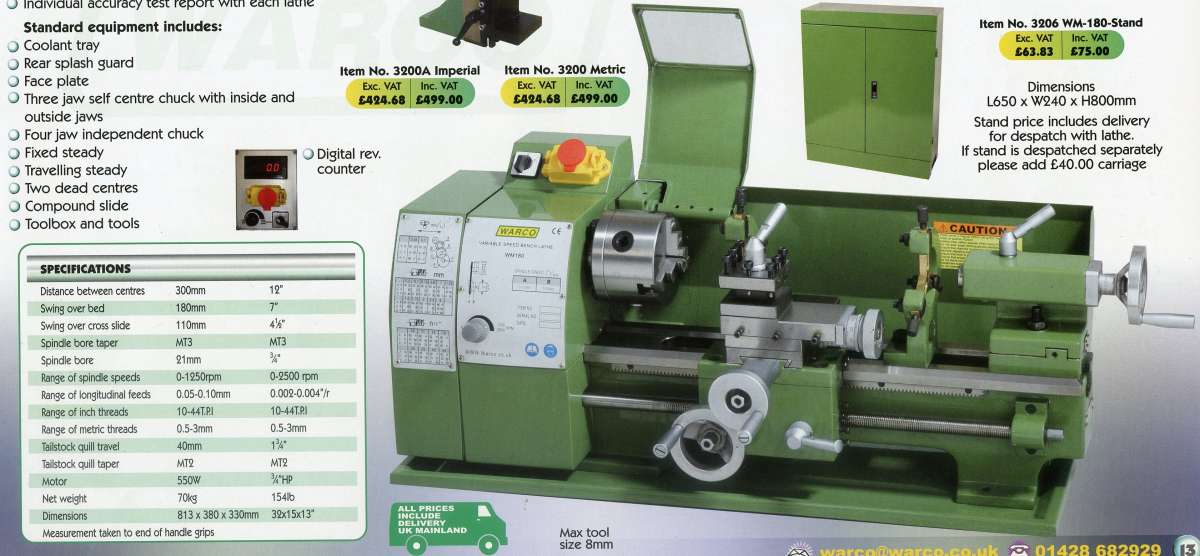
                                              Hi, here’s a scan of a WM-180 from their 30 years catalogue, which shows the specs for both metric and imperial machines, which may be of help.

                                              wm180001

                                              As NDIY has said, if you can turn the leadscrew a full number of known turns, and then measure how far the carriage has moved, it well tell you the pitch.

                                              Click on the scan for a bigger picture.

                                              Regards Nick.

                                              #867676
                                              James A
                                              Participant
                                                @jamesalford67616

                                                Thank you for all of the replies.

                                                As Neil suggests, I have been spoilt by the 1.5 thou feed on my old machine.

                                                Leaving aside the precise pitch of the leadscrew, it seems that if I wish to reduce the feed rate, I will need to explore alternative gears or add a separate power feed. Alternatively, live with it as it is and get used to it.

                                                James.

                                                #867682
                                                JasonB
                                                Moderator
                                                  @jasonb

                                                  As I said in my first reply the chance of just being able to swap gears is going to be quite limited by the slot in the banjo. You could only get a larger driven one in if the top stud can be slide further away from the lower one, you also have to take care that where you have large andd small gears on the studs that they do not interfere with what is on the adjacent stud so reducing the drivers tooth count won’t work.

                                                  At best you might be able to gain a bit of room on the banjo to get maybe another 80T on there otherwise it is a case of making a new banjo  to take an extra stud and not being able to fit the gear guard when using fine feed.


                                                  ELS would be another option.

                                                  #867694
                                                  James A
                                                  Participant
                                                    @jamesalford67616

                                                    I do take your point, Jason. Accepting the supplied speed, a separate power feed or an ELS are the realistic options.


                                                    James

                                                    #867697
                                                    John Haine
                                                    Participant
                                                      @johnhaine32865

                                                      It should be straighforward to calculate the LS pitch, from the gear ratios given in the threading chart for a given screw pict.

                                                    Viewing 25 posts - 1 through 25 (of 37 total)
                                                    • Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.

                                                    Latest Replies

                                                    Viewing 25 topics - 1 through 25 (of 25 total)
                                                    Viewing 25 topics - 1 through 25 (of 25 total)

                                                    View full reply list.