
Best approach to pip removal

Best approach to pip removal

Home › Forums › Workshop Techniques › Best approach to pip removal

Viewing 22 posts - 1 through 22 (of 22 total)
  • Author
    Posts
  • #868870
    Bill Phinn
    Participant
      @billphinn90025

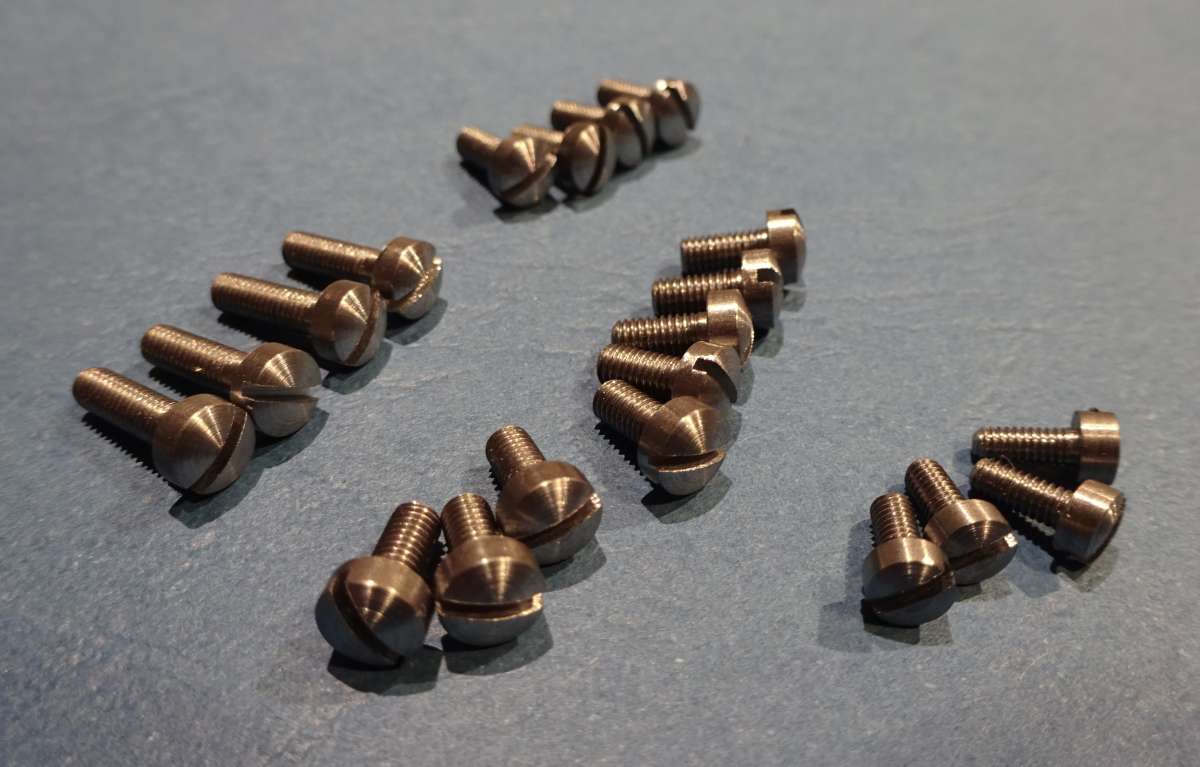
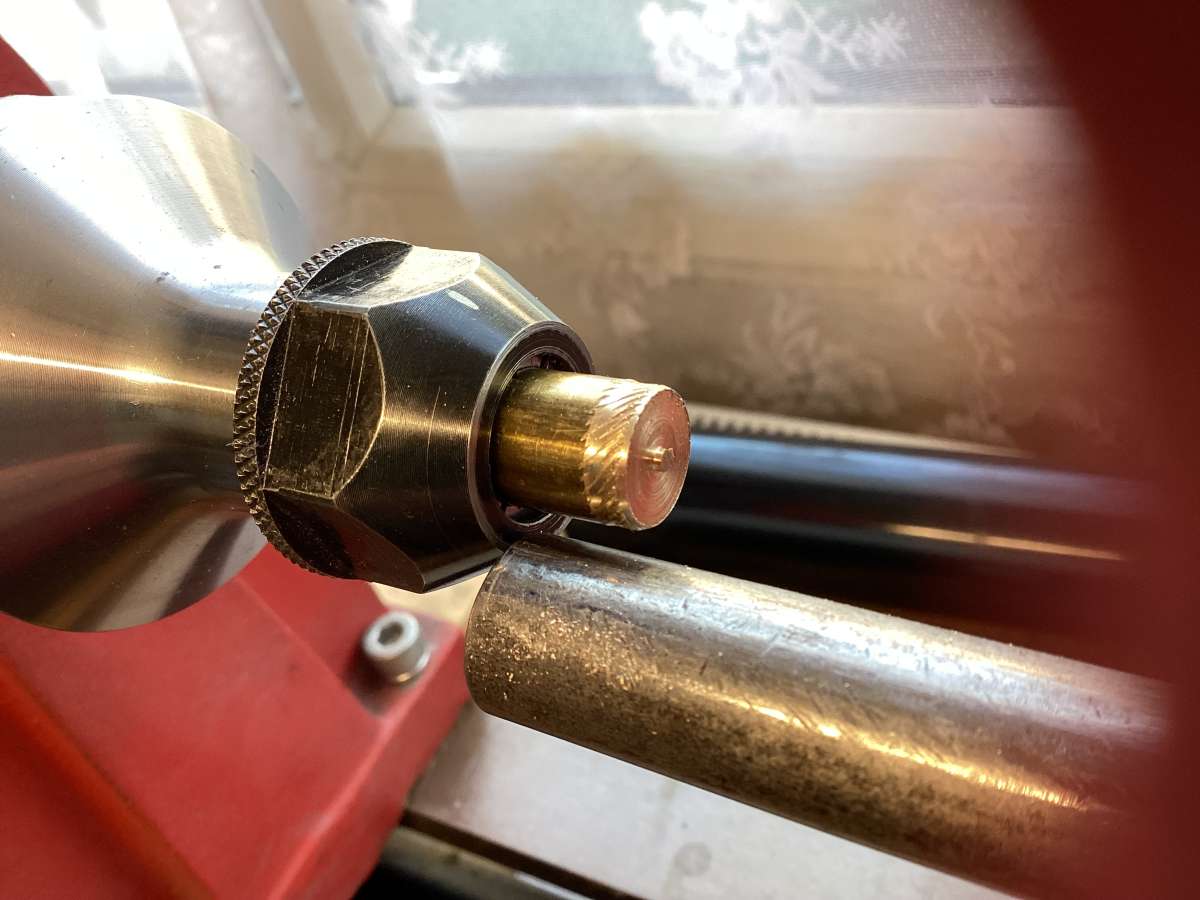
      When you have to remove a small pip after parting off a small (i.e. less than 1/2”) diameter part, and the pip you’re concerned with is on the back of the piece you’ve parted off, meaning the part has to be re-chucked and there is a slight increase in runout as a consequence, what is the best approach?

      I ask because the forces involved in removing the pip seem very considerable at times, whether I face off the pip or advance the carriage to do so, or use a combination of both.

      What type of tool is best for the job and what sort of spindle rpm? I’m doing brass mainly (e.g. knurled thumb screws), am after a very good surface finish (maybe even a slightly domed end) and I’m wondering whether this might be a job for a hand-held tool, not just to achieve the dome but to remove the pip as well.

      #868883
      peak4
      Participant
        @peak4

        I can’t really speak for brass pips, but generally I’ve found that the job is very sensitive to tool height.
        Also, particularly if the pip is off centre, ground carbide inserts are more sensitive to chipping, as it’s a small area of metal that’s hitting the insert at a comparatively low speed.
        I tend to knock off the pip as fast an RPM as possible, and face at whatever speed seems appropriate.
        Easier with a VFD driven motor of course.
        Alternatively, use a fine file, and then face.

        Bill

        #868887
        Michael Gilligan
        Participant
          @michaelgilligan61133

          It seems like an ideal job for the hand Graver

          Sorry … old age and Arthritis have made me too clumsy to demonstrate.

          MichaelG.

          .

          Edit: … You might start here:

          .

          .

          #868888
          JasonB
          Moderator
            @jasonb

            If you want a domed end then you have two options.

            1. File against the rotating work, moving the file to create the dome shape and you can just file off the pip first. Single cut lathe file will make quick work of it.

            2. Requires a better grip so maybe a threaded split bush so that you can use a form tool set on ctr height it will also deal with the pip


            For a flat end if filing off the pip is not good enough then just a sharp HSS or **GT insert with small 0.2 tip radius. Ideally hold in a split bush as you won’t get a solid grip on a threaded surface so the pip may want to ride up over the tool.

            In all cases small dia brass wants a fast speed probably as fast as your lathe will go but whatever is quick to select.

            The pip can be reduced if you use a parting tool with an angled end. Again what ever parting tool used needs to be sharp.

            Or do it a sI do when making screws for my engines. Turn shank and thread (knurl in your case). Saw off from bar a bit over length. Hold by threaded end as appropriate and use a form tool to shape the head. Works well with batches of screws as well as singles

            DSC03782

            #868889
            Dell
            Participant
              @dell

              If I want a slight dome on a part no matter if it’s on the Pultra or the Myford I use a graver because it will also remove the pip but if the item is to be slotted then I don’t mind the pip as it shows centre of part, my hand parting tools have slight taper left & right so if I want the pip on part I use right taper or left if I don’t want pip on part.

              This video may help as the end of it has a rounded end it was for a drum clock I restored.

              #868891
              Hollowpoint
              Participant
                @hollowpoint

                You can get such a thing as an engineering chisel, for exactly this type of thing. Cut the pip off flush with the chisel and then face the part as normal. CCGT tips and high speed give a fantastic finish.

                #868903
                Michael Gilligan
                Participant
                  @michaelgilligan61133

                  Nice demo, Dell

                  … compared with all that, of course, removing a pip is a doddle !


                  MichaelG.

                  #868904
                  Julie Ann
                  Participant
                    @julieann

                    Use a right hand parting tool so it doesn’t leave a pip on the work in the first place.

                    Julie

                    #868933
                    Howard Lewis
                    Participant
                      @howardlewis46836

                      Grinding a HSS parting tool with a slight front angle may help, but it does impose a sideways force on the tool, (So you might get a sloping end face) and makes the swarf wider than the groove, so the risk of a jam up increases.

                      Using a carbide tipped parting tool, with its central groove,  giving two narrow streams of swarf towards the centre of the groove may help.

                      Howard

                      #868937
                      Colin Teasdale
                      Participant
                        @colinteasdale

                        I find that I only get a pip if the tool height is wrong.

                        A pip shows the tool is too low, while a slight ‘mound’ shows the tool is too high. Adjust the tool so that you can face the pip off and the tool should be at the correct height for the next operation.

                        #868956
                        Bill Phinn
                        Participant
                          @billphinn90025

                          Many thanks for the trove of interesting replies.

                          To first clarify matters touched on by Bill and Colin, the parting tool and subsequent turning tool are absolutely on centre. A significant part of the problem, I think, is that once the part is flipped round in the three-jaw and re-chucked, the pip isn’t quite on centre, even if it’s a very small quite. Don’t forget also, Colin, that the pip isn’t being left after a facing operation but after a parting operation, and that’s partly because I deliberately held off from pushing the parting tool all the way in and the part broke off anyway before I got that far. I’m pretty sure my dithering and an insufficient spindle speed contributed to this outcome.

                          My parting tool doesn’t have a bias on it; I’m using GTN2 inserts, which I’ve found to be excellent for parting everything from aluminium to high tensile steel. I’m loath to give them up for general parting work, but I do want to experiment grinding parting tools with a bias on them when I have time.

                          Making a form tool to do the doming is also something I’ve been meaning to get round to; it makes sense to have one, particularly for repeat work as shown by Jason. I wouldn’t want to hand-hold a graver in any case if work is in the three jaw; I’d fit a collet chuck instead or transfer it to my woodturning lathe with its own slimline collet chuck.

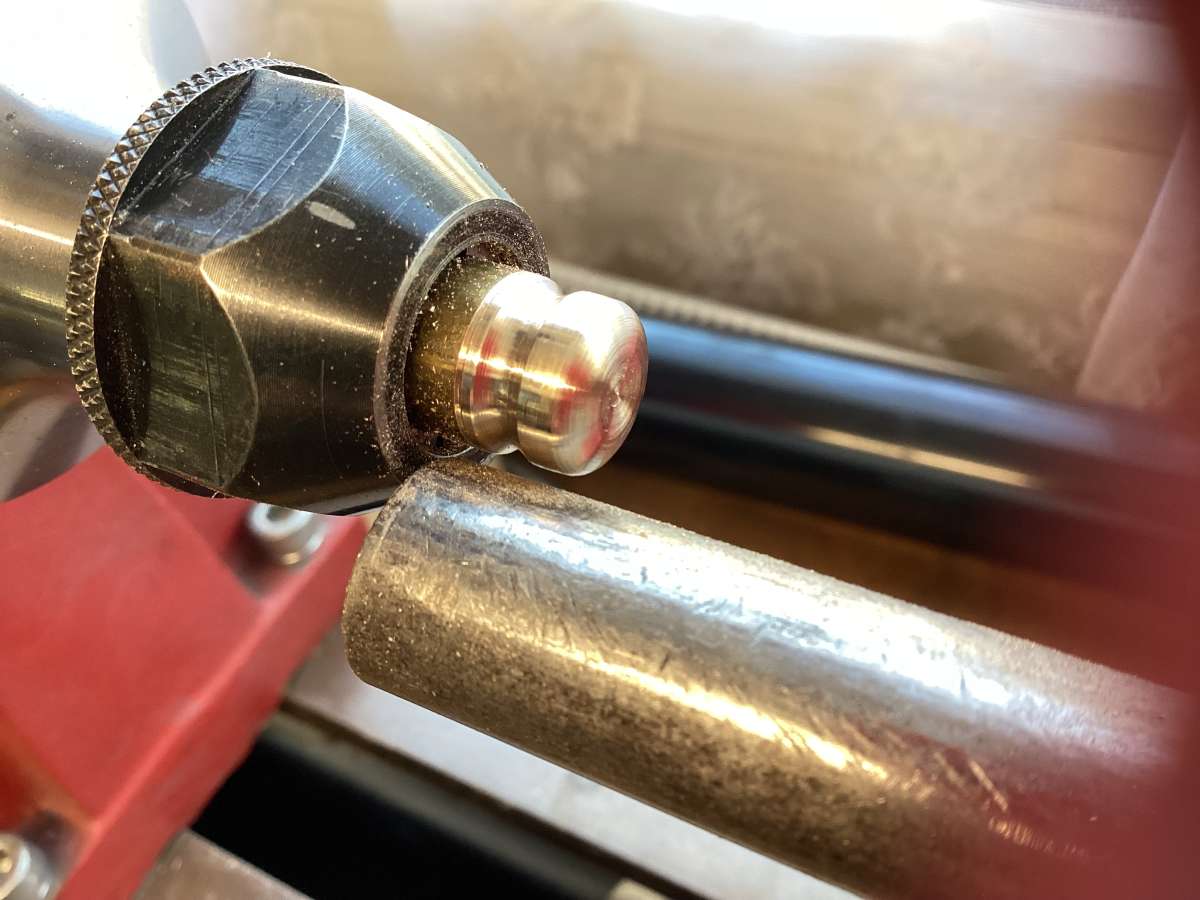
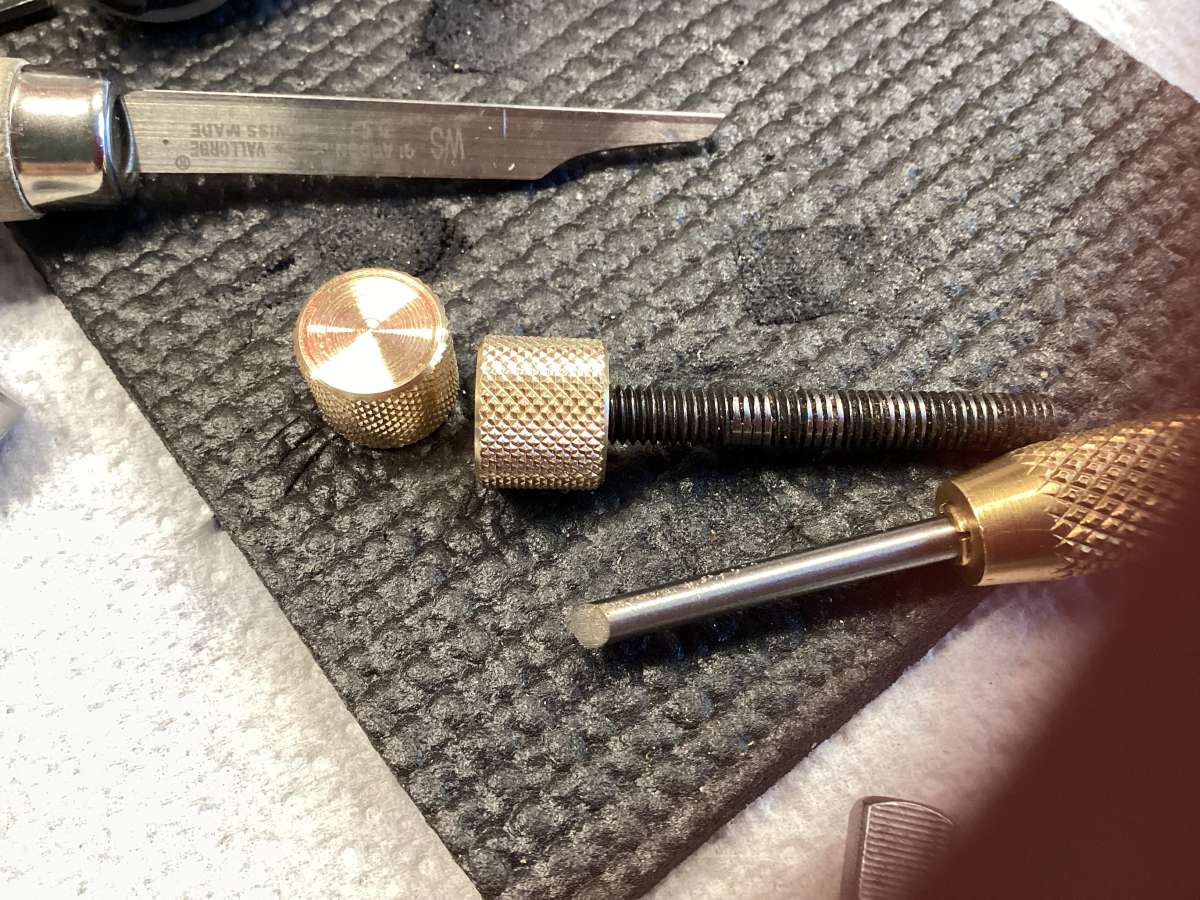
                          I had a ten minute play earlier, and removing the pip in the wood lathe with the round graver pictured (next to the knurled thumb nuts) was pretty effortless, as was the random bit of doming and grooving achieved with the same graver. BTW, the chewed up screw inserted in one of the thumb nuts is sacrificial for holding things in the three-jaw, not part of any finished work.

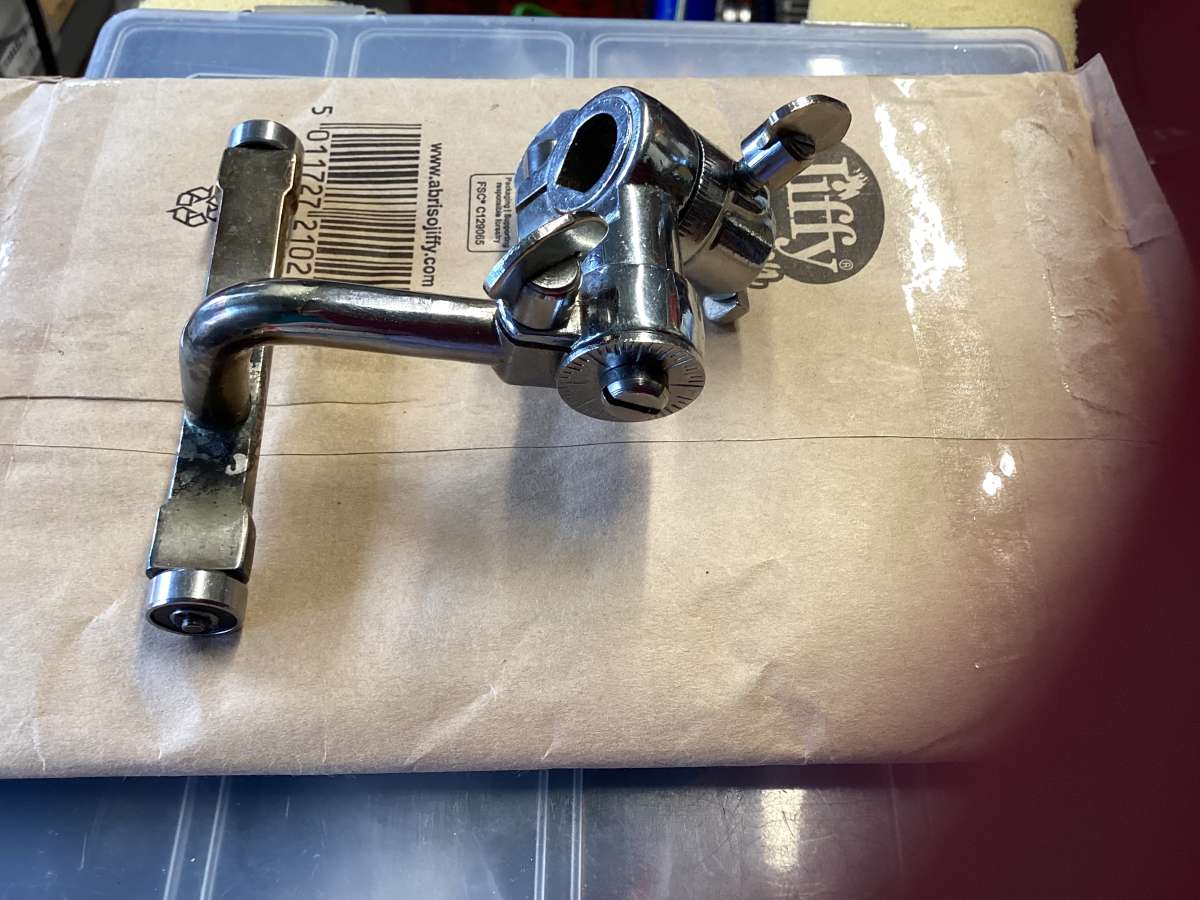
                          The two videos were a useful refresher course for me, thank you. It’s been a while since I got my gravers out. I don’t use a wooden block as a jig for sharpening, as shown in Michael’s video, but a Crocker type jig (pictured), which I adapted after seeing Bergeon’s own off-the-peg graver sharpening jig, which runs on bearings.

                          Hollowpoint, can you show me a picture of the engineering chisel you mention?IMG_2443IMG_2445IMG_2442IMG_2440

                          #868965
                          JasonB
                          Moderator
                            @jasonb

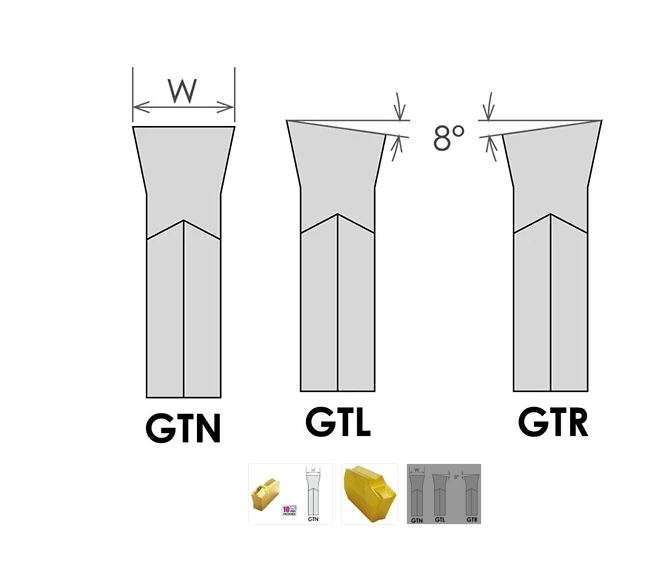
                            You do not need to give up your parting inserts. The “N” in GTN stands for neutral eg flat across the end. You can also buy GTL and GTR depending on what side you want to leave a pip. Also as with turning inserts you can get most of the parting blades with “sharper” edges which will not be pushing against the metal as much as the usual moulded ones.

                            hand gt

                            Parting is always likely to leave a pip even with a tool on ctr height as the small diameter remaining as you get towards the end of the cut is unable to support the part being parted off, the usual half hard brass will fracture before a more ductile metal will.

                            #868967
                            Bill Phinn
                            Participant
                              @billphinn90025

                              That’s great news, Jason, on the existence of left and right GT variants. I’ll do a search for those in the usual places right away.

                              I take it these are the right hand ones.

                              …or these

                              #868977
                              Julie Ann
                              Participant
                                @julieann

                                The OP was asking about brass, so worries about swarf jamming in the groove don’t apply.

                                This is my angled parting tool, it could do with a little TLC:

                                Parting Tool

                                It’s a left hand tool because it is behind the headstock and normal spindle rotation is backwards compared to most lathe. It works fine on steel and brass and leaves no pip on the work. A futher pull on the handle and the tool removes the cone shaped pip left on the stock.

                                This is my form tool for creating domed ends:

                                Form Tool

                                It was ground free hand and is a fairly sharp curve as it is mostly used for rounding the end of studs.

                                Julie

                                #868994
                                Bill Phinn
                                Participant
                                  @billphinn90025

                                  Thanks for that, Julie Ann.

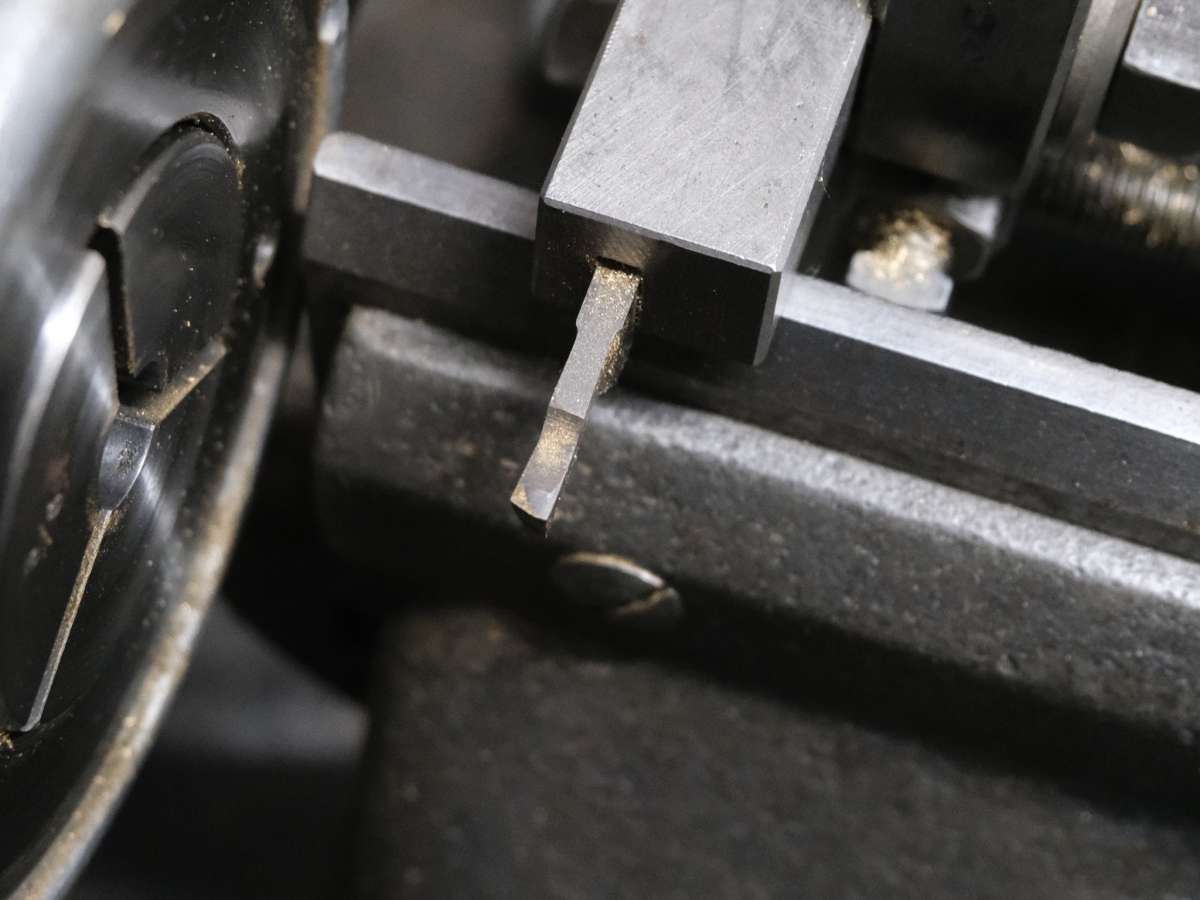
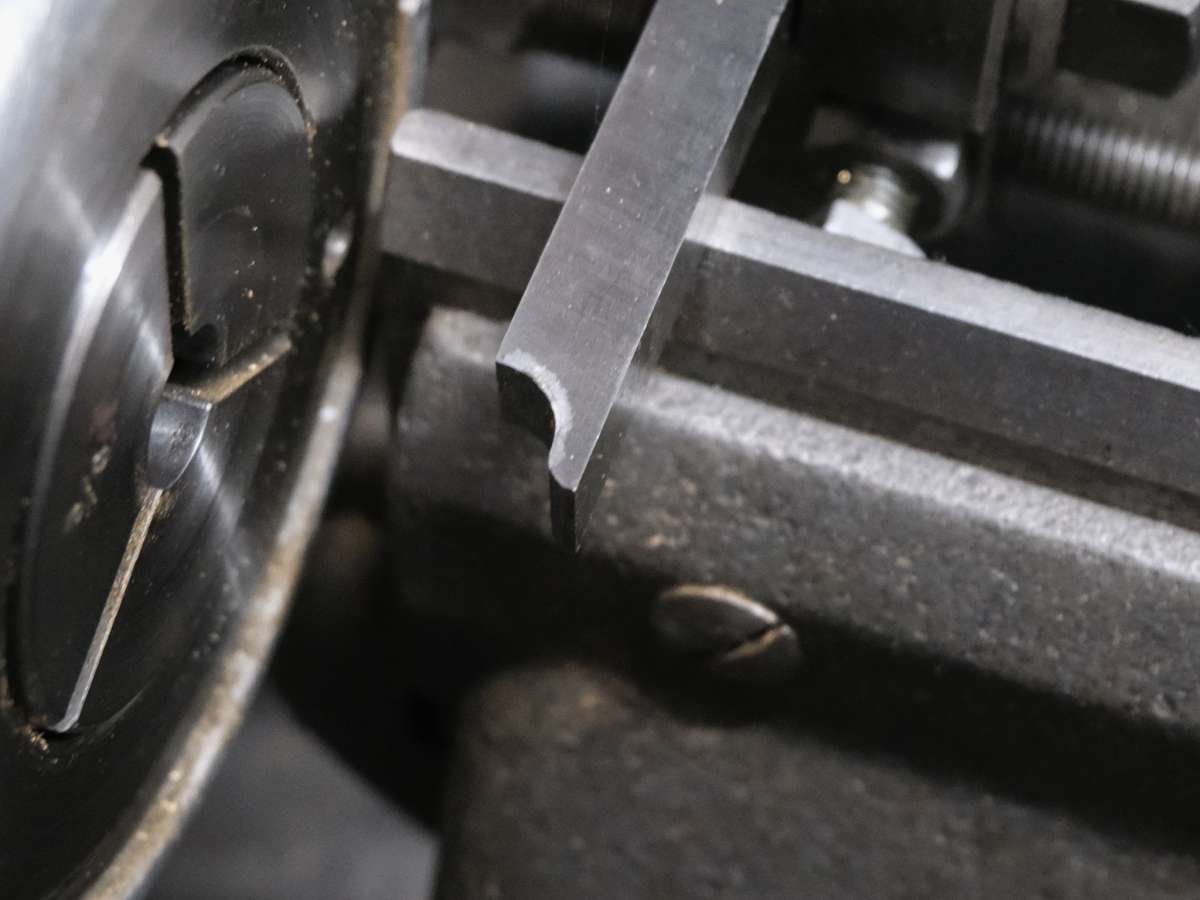
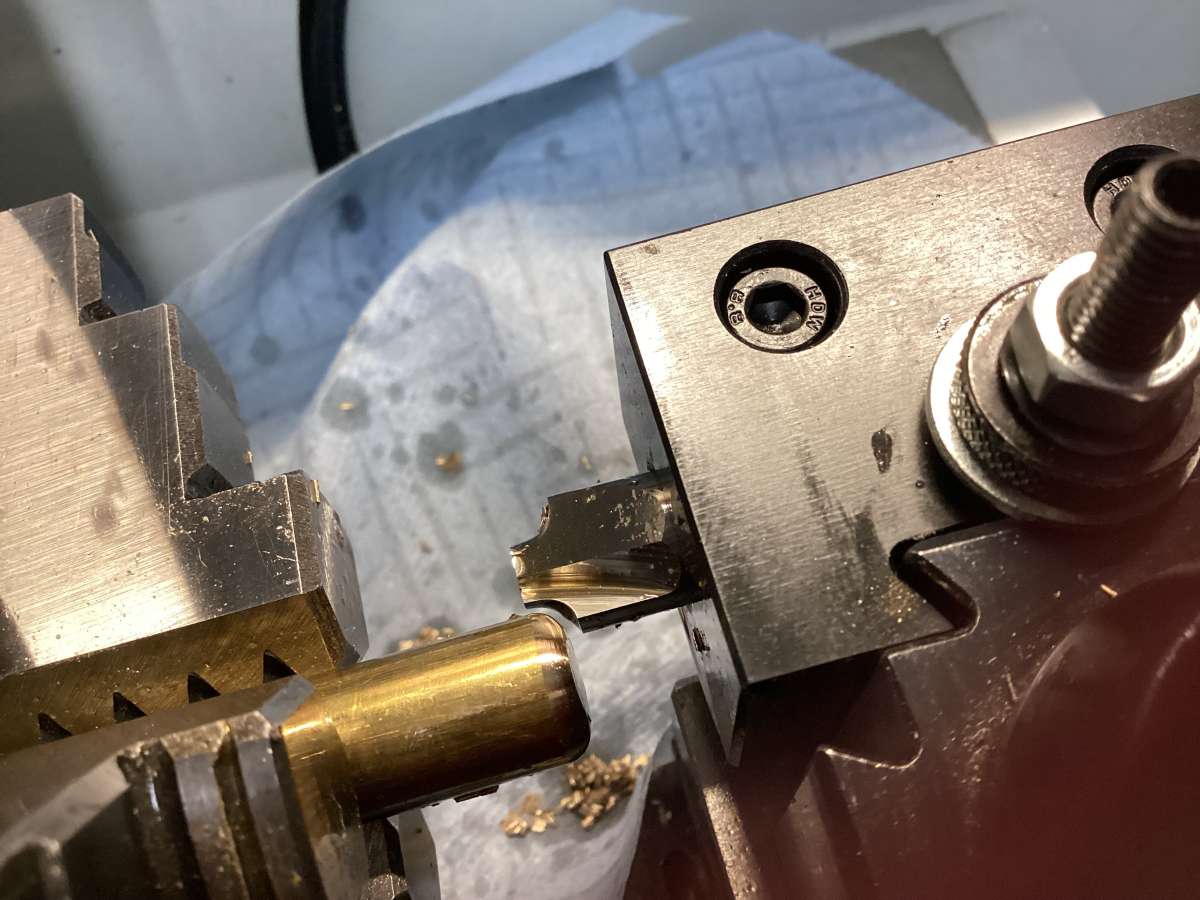
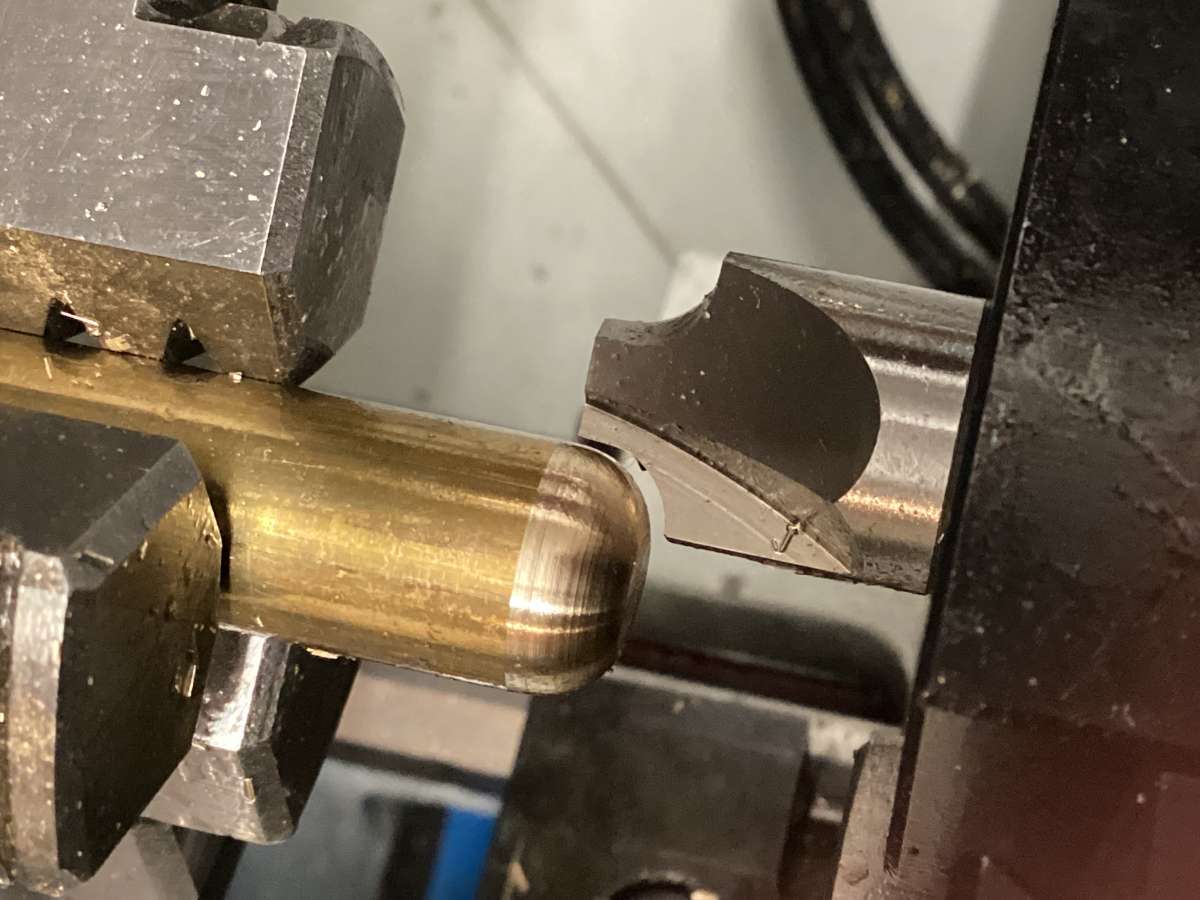
                                  I still mean to make a form tool and experiment with my own ground parting tool. For the time being, I’ve had a go with two corner-rounding end mills.

                                  IMG_2448IMG_2449

                                  #869007
                                  Nigel Graham 2
                                  Participant
                                    @nigelgraham2

                                    The pip on brass is usually slightly brittle.

                                    Often, I shear it off by holding the face of the work against a sharp edge, perhaps the edge of a square HSS tool shank, pip resting on the edge, and giving the work a sharp tap with a mallet or block of wood. It leaves a slight boss, which may not matter or can be filed or faced off to taste, but at least removing the little spike.

                                    #869072
                                    Hollowpoint
                                    Participant
                                      @hollowpoint

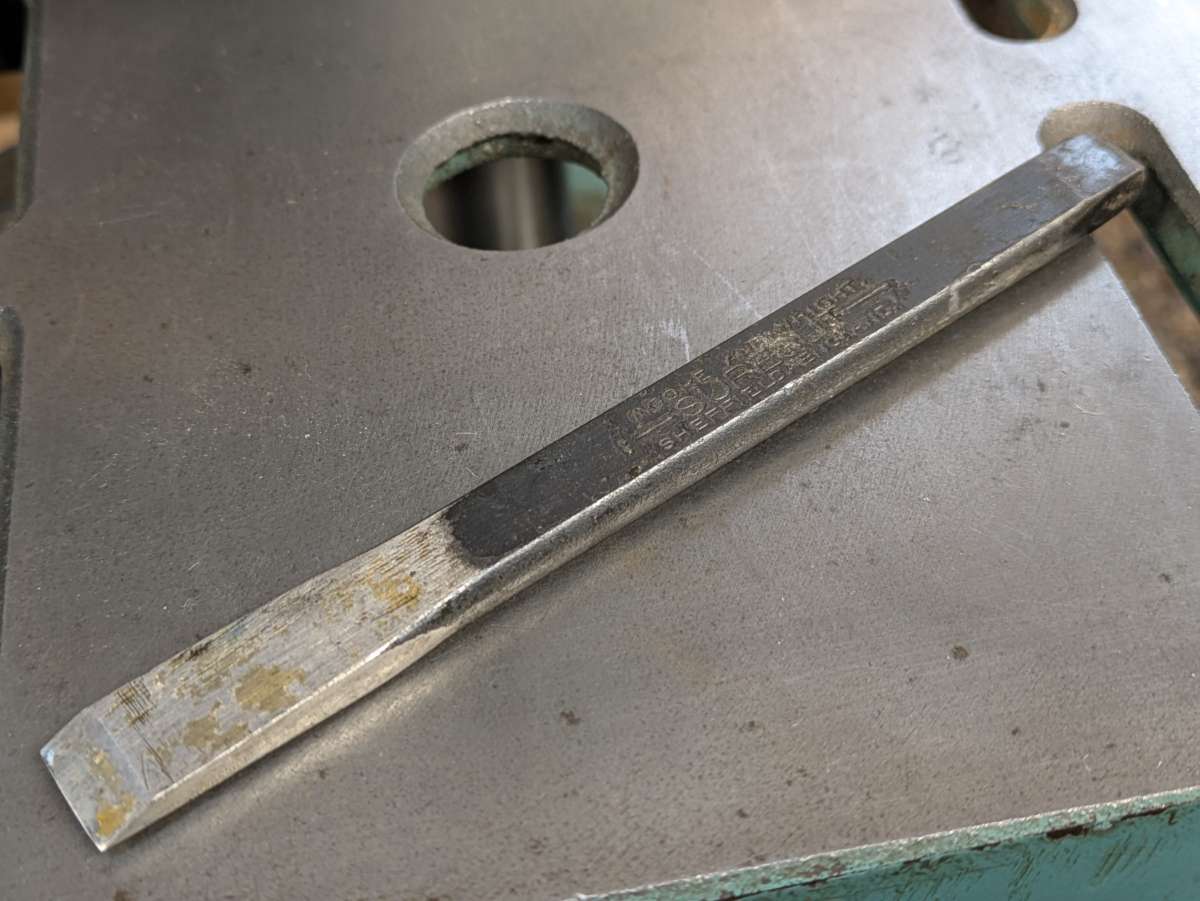
                                      This is a Moore & Wright “Surecut” chisel. Not a lot different from any other chisel, but only bevelled on one side, quite sharp and probably harder than normal steel.

                                      PXL_20261012_125052752


                                      #869184
                                      Bill Phinn
                                      Participant
                                        @billphinn90025

                                        Thanks, Nigel and Hollowpoint.

                                        It seems that pip removal not involving cutting with a lathe tool but rather cutting using pure violence is an accepted practice in some quarters. If it gets the job done, why not?, I suppose.

                                        #869189
                                        Nigel Graham 2
                                        Participant
                                          @nigelgraham2

                                          “pure violence”? That’s a bit strong! 🙂

                                          It’s hardly “use a bigger ‘ammer, guv” territory!

                                          #869197
                                          JasonB
                                          Moderator
                                            @jasonb

                                            Pure Violence, depends on the size of your chisel and how hard you hit it. I have seen some very intricate engraving done with chisel and hammer.

                                            Also lets not forget that back in the day before we all had milling machines a chisel in the right hands would be used to cut keyways, steam ports, etc. I have a little 3/16″ wide one that still gets used where appropriate, such as where a milling cutter leaves a radius in a corner the chisel can deal with that.

                                            #869211
                                            Hollowpoint
                                            Participant
                                              @hollowpoint

                                              Bill, you might be surprised at how easy it is to break/cut a pip off with a chisel. Especially in brass. As long as its under say 1mm in diameter it’s just a light tap.

                                              #869328
                                              Bill Phinn
                                              Participant
                                                @billphinn90025

                                                Thank you for the further replies.

                                                I didn’t know chisels were still used in this way in the machine room. Given that I’ve been known to use a graver for shaving metal in awkward places, then the use of chisels begins to look less unusual.

                                                Also, Hollowpoint and Nigel’s posts remind me that I do own such a thing as an air hammer and I have used it with air chisels to remove rivets, which it did effortlessly. I’m sure I could easily grind up a spare air chisel with a bevel on only one side.

                                              Viewing 22 posts - 1 through 22 (of 22 total)
                                              • Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.

                                              Latest Replies

                                              Home › Forums › Workshop Techniques › Topics

                                              Viewing 25 topics - 1 through 25 (of 25 total)
                                              Viewing 25 topics - 1 through 25 (of 25 total)

                                              View full reply list.