
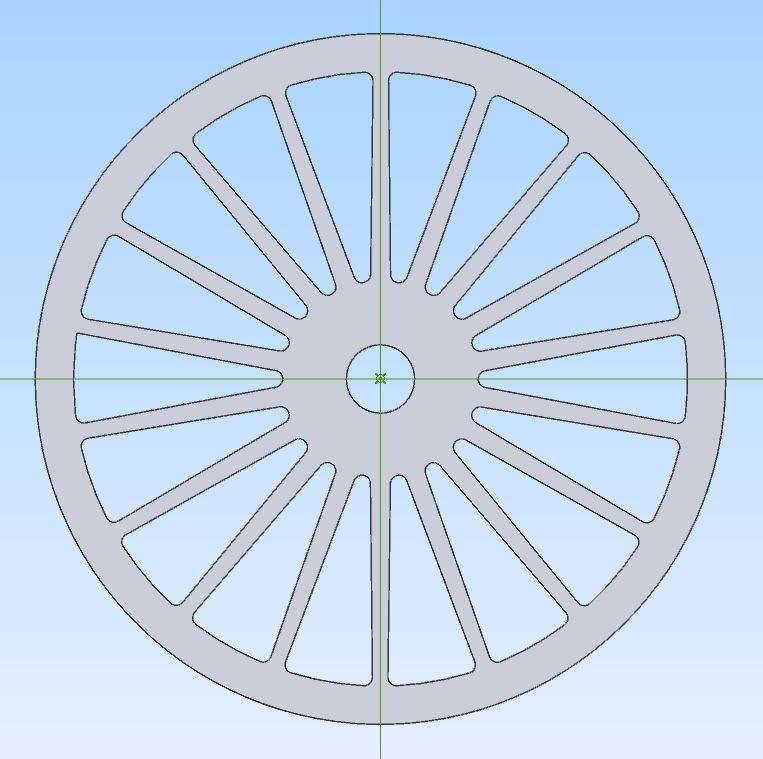
rotary table issue
rotary table issue
- This topic has 7 replies, 5 voices, and was last updated 12 October 2026 at 22:47 by
 duncan webster 1.
 duncan webster 1.
 tatler
 Clive Foster
 Andrew Crow
 JasonB
 duncan webster 1
- Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.
Latest Replies
-
- Topic
- Voices
- Last Post
-
-
Still On IMSI’s Books!
Started by:
Nigel Graham 2
in: CAD – Technical drawing & design
- 1
-
13 October 2026 at 00:34
Nigel Graham 2
-
Farm Gate Lock.
Started by:
Grizzly bear
in: The Tea Room
- 11
-
13 October 2026 at 00:07
duncan webster 1
-
Best approach to pip removal
Started by:
Bill Phinn
in: Workshop Techniques
- 10
-
12 October 2026 at 23:07
Nigel Graham 2
-
Workshop building – have lots of space
Started by:
Carl Farrington
in: General Questions
- 7
-
12 October 2026 at 22:59
duncan webster 1
-
rotary table issue
Started by:
tatler
in: Workshop Tools and Tooling
- 5
-
12 October 2026 at 22:47
duncan webster 1
-
Tom Senior small vertical head axial play
Started by:
chris1984
in: Manual machine tools
- 3
-
12 October 2026 at 20:45
Kiwi Bloke
-
Model Engineer Magazine Collection
Started by:
mfengine1
in: Books
- 11
-
12 October 2026 at 20:12
noel shelley
-
rotary table to make 1 gauge drive wheels
Started by:
tatler
in: Locomotives
- 2
-
12 October 2026 at 19:43
JasonB
-
Model Turbines
1
2
…
26
27
Started by:
Turbine Guy
in: Stationary engines
- 28
-
12 October 2026 at 19:22
Turbine Guy
-
Midlands Exhibition, share a taxi
Started by:
duncan webster 1
in: Exhibitions, Shows and Club Events
- 1
-
12 October 2026 at 18:30
duncan webster 1
-
Does anyone have any info about these vices
Started by:
bjcolyer
in: Introduce Yourself – New members start here!
- 2
-
12 October 2026 at 17:39
Nigel Bennett
-
New Member
Started by:
starjump
in: Introduce Yourself – New members start here!
- 4
-
12 October 2026 at 16:37
Howard Lewis
-
Motorcycle Centre Stand Pivot
Started by:
COLIN MARTIN 2
in: Related Hobbies including Vehicle Restoration
- 8
-
12 October 2026 at 15:04
COLIN MARTIN 2
-
Moving Targets
Started by:
Michael Gilligan
in: The Tea Room
- 11
-
12 October 2026 at 13:07
Martin Johnson 1
-
Powerfeeders
Started by:
larry phelan 1
in: Help and Assistance! (Offered or Wanted)
- 5
-
12 October 2026 at 12:32
larry phelan 1
-
Clutch for ML7R
Started by:
Andrew Tinsley
in: Manual machine tools
- 7
-
12 October 2026 at 10:49
Dave Wootton
-
The lazy man’s fly cutter
Started by:
Sonic Escape
in: Workshop Tools and Tooling
- 12
-
12 October 2026 at 09:45
Andy Stopford
-
Reverting An ML7 To Change-Wheels: Any Thoughts??
1
2
3
Started by:
Nigel Graham 2
in: Manual machine tools
- 22
-
12 October 2026 at 09:33
Charles Lamont
-
What Did You Do Today 2026
1
2
…
8
9
Started by:
JasonB
in: The Tea Room
- 54
-
11 October 2026 at 23:25
Nigel Graham 2
-
3 1/2” gauge loco, coupling height?
Started by:
Paul McDonough
in: Locomotives
- 5
-
11 October 2026 at 22:14
Paul McDonough
-
Liney RV-2 Rescue
Started by:
JasonB
in: Stationary engines
- 3
-
11 October 2026 at 21:43
renardiere7
-
Preview of whats coming in Freecad 26.3
1
2
Started by:
Russell Eberhardt
in: CAD – Technical drawing & design
- 8
-
11 October 2026 at 20:36
lee webster
-
Myford ML4 Identification
Started by:
Steven Volz
in: Manual machine tools
- 7
-
11 October 2026 at 17:08
Howard Lewis
-
Hello from Pensford
Started by:
ralpharama
in: Introduce Yourself – New members start here!
- 3
-
11 October 2026 at 16:08
Howard Lewis
-
Too much to take in in one go, FreeCAD 26.3
Started by:
Russell Eberhardt
in: CAD – Technical drawing & design
- 1
-
11 October 2026 at 15:47
Russell Eberhardt
-
Still On IMSI’s Books!
 Nigel Graham 2
 Grizzly bear
 Bill Phinn
 Carl Farrington
 tatler
 chris1984
 Kiwi Bloke
 mfengine1
 noel shelley
 JasonB
 Turbine Guy
 bjcolyer
 Nigel Bennett
 starjump
 Howard Lewis
 COLIN MARTIN 2
 Michael Gilligan
 Martin Johnson 1
 larry phelan 1
 Andrew Tinsley
 Dave Wootton
 Sonic Escape
 Andy Stopford
 Charles Lamont
 Paul McDonough
 renardiere7
 Russell Eberhardt
 lee webster
 Steven Volz
 ralpharama
Latest Issue
Newsletter Sign-up
Latest Replies