
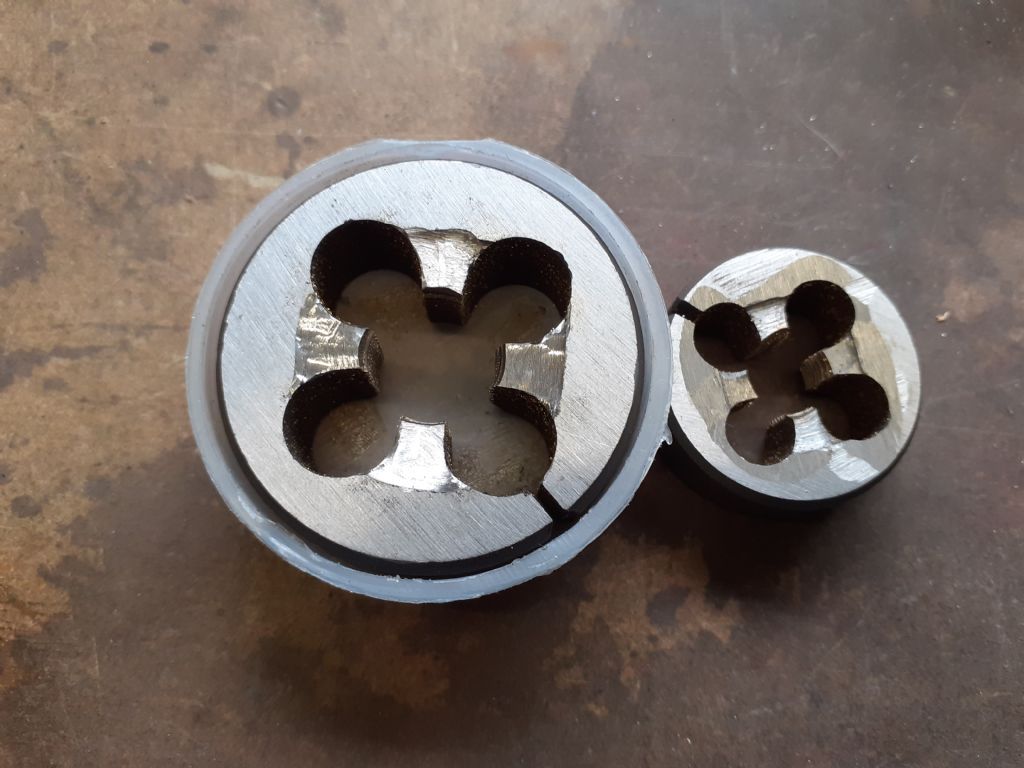
Make-shift surface grinding of a threading die face
Make-shift surface grinding of a threading die face
- This topic has 10 replies, 7 voices, and was last updated 22 February 2021 at 11:40 by
 Lainchy.
 Lainchy.
 Greensands
 Mike Poole
 Pete Rimmer
 10ba12ba
 BOB BLACKSHAW 1
 JasonB
 Lainchy
- Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.
Latest Replies
-
- Topic
- Voices
- Last Post
-
-
ML10 and Chuck cleaning Information
1
2
Started by:
starjump
in: Beginners questions
- 10
-
19 October 2026 at 23:05
duncan webster 1
-
ML7 change gear caluclator
Started by:
drnewcomb
in: Manual machine tools
- 6
-
19 October 2026 at 21:15
Georgineer
-
Rivetting with a hydraulic press
Started by:
Martin Johnson 1
in: Workshop Tools and Tooling
- 16
-
19 October 2026 at 20:34
old mart
-
carbide insert lathe tools
1
2
Started by:
davidwf
in: Workshop Tools and Tooling
- 16
-
19 October 2026 at 20:30
old mart
-
LAzar egde finder
Started by:
ian Holdsworth
in: Beginners questions
- 5
-
19 October 2026 at 19:55
Ches Green UK
-
Coventry die head
Started by:
lug lord
in: Workshop Techniques
- 8
-
19 October 2026 at 18:27
John MC
-
The Latest INDEX to Model Engineer & Workshop (Also past issues of MEW)
1
2
3
Started by:
David Frith
in: Model Engineer & Workshop
- 7
-
19 October 2026 at 17:04
David Frith
-
Rush of blood or not
Started by:
BOB BLACKSHAW 1
in: 3D Printers and 3D Printing
- 8
-
19 October 2026 at 16:56
BOB BLACKSHAW 1
-
Pencil Sharpener
1
2
Started by:
Vic
in: The Tea Room
- 17
-
19 October 2026 at 14:07
Joseph Noci 1
-
Making a Lathe Bench for a Myford ML10
1
2
Started by:
starjump
in: Beginners questions
- 11
-
19 October 2026 at 13:17
southernchap
-
PROGRESS
Started by:
Phillip weaver
in: Introduce Yourself – New members start here!
- 5
-
19 October 2026 at 12:01
Phillip weaver
-
Su251-53
1
2
Started by:
parovoz
in: Locomotives
- 15
-
19 October 2026 at 11:04
noel shelley
-
What Did You Do Today 2026
1
2
…
8
9
Started by:
JasonB
in: The Tea Room
- 54
-
18 October 2026 at 20:28
Bazyle
-
Trying a new controller
Started by:
John Haine
in: CNC machines, Home builds, Conversions, ELS, automation, software, etc tools
- 4
-
18 October 2026 at 13:58
Joseph Noci 1
-
The Sunday bazar
1
2
Started by:
Sonic Escape
in: The Tea Room
- 19
-
18 October 2026 at 12:44
Sonic Escape
-
Myford ML4 Identification
Started by:
Steven Volz
in: Manual machine tools
- 7
-
18 October 2026 at 04:43
Steven Volz
-
Richard B’s Minnie.
Started by:
Richard B
in: Traction engines
- 4
-
17 October 2026 at 22:22
Richard B
-
Weight of Myford Super 7 / ML7R
Started by:
Andrew Tinsley
in: General Questions
- 6
-
17 October 2026 at 21:06
Zan
-
Scroll Saw Blades for Steel
1
2
Started by:
James A
in: Workshop Tools and Tooling
- 15
-
17 October 2026 at 21:05
bernard towers
-
Model Turbines
1
2
…
26
27
Started by:
Turbine Guy
in: Stationary engines
- 28
-
17 October 2026 at 19:22
Turbine Guy
-
Bridge collapse
1
2
Started by:
JA
in: The Tea Room
- 13
-
17 October 2026 at 18:21
JA
-
My week this week! My workshop videos
1
2
…
13
14
Started by:
Phil Whitley
in: The Tea Room
- 16
-
17 October 2026 at 15:14
Phil Whitley
-
Old topics on this Forum
Started by:
JA
in: Website Questions, Comments, and Suggestions
- 5
-
17 October 2026 at 14:40
John Haine
-
Lathe arriving – source some practice materials
1
2
Started by:
starjump
in: Beginners questions
- 18
-
17 October 2026 at 10:24
vic newey
-
injector operation
Started by:
Garry Coles
in: General Questions
- 6
-
17 October 2026 at 09:38
MichaelR
-
ML10 and Chuck cleaning Information
1
2
 starjump
 duncan webster 1
 drnewcomb
 Georgineer
 Martin Johnson 1
 old mart
 davidwf
 ian Holdsworth
 Ches Green UK
 lug lord
 John MC
 David Frith
 BOB BLACKSHAW 1
 Vic
 Joseph Noci 1
 southernchap
 Phillip weaver
 parovoz
 noel shelley
 JasonB
 Bazyle
 John Haine
 Sonic Escape
 Steven Volz
 Richard B
 Andrew Tinsley
 Zan
 James A
 bernard towers
 Turbine Guy
 JA
 Phil Whitley
 vic newey
 Garry Coles
 MichaelR
Latest Issue
Newsletter Sign-up
Latest Replies
- ML10 and Chuck cleaning Information
- ML7 change gear caluclator
- Rivetting with a hydraulic press
- carbide insert lathe tools
- LAzar egde finder
- Coventry die head
- The Latest INDEX to Model Engineer & Workshop (Also past issues of MEW)
- Rush of blood or not
- Pencil Sharpener
- Making a Lathe Bench for a Myford ML10