
finding involute gear cutter

finding involute gear cutter

Home › Forums › Workshop Techniques › finding involute gear cutter

Viewing 25 posts - 1 through 25 (of 27 total)
  • Author
    Posts
  • #866472
    vic newey
    Participant
      @vicnewey60017

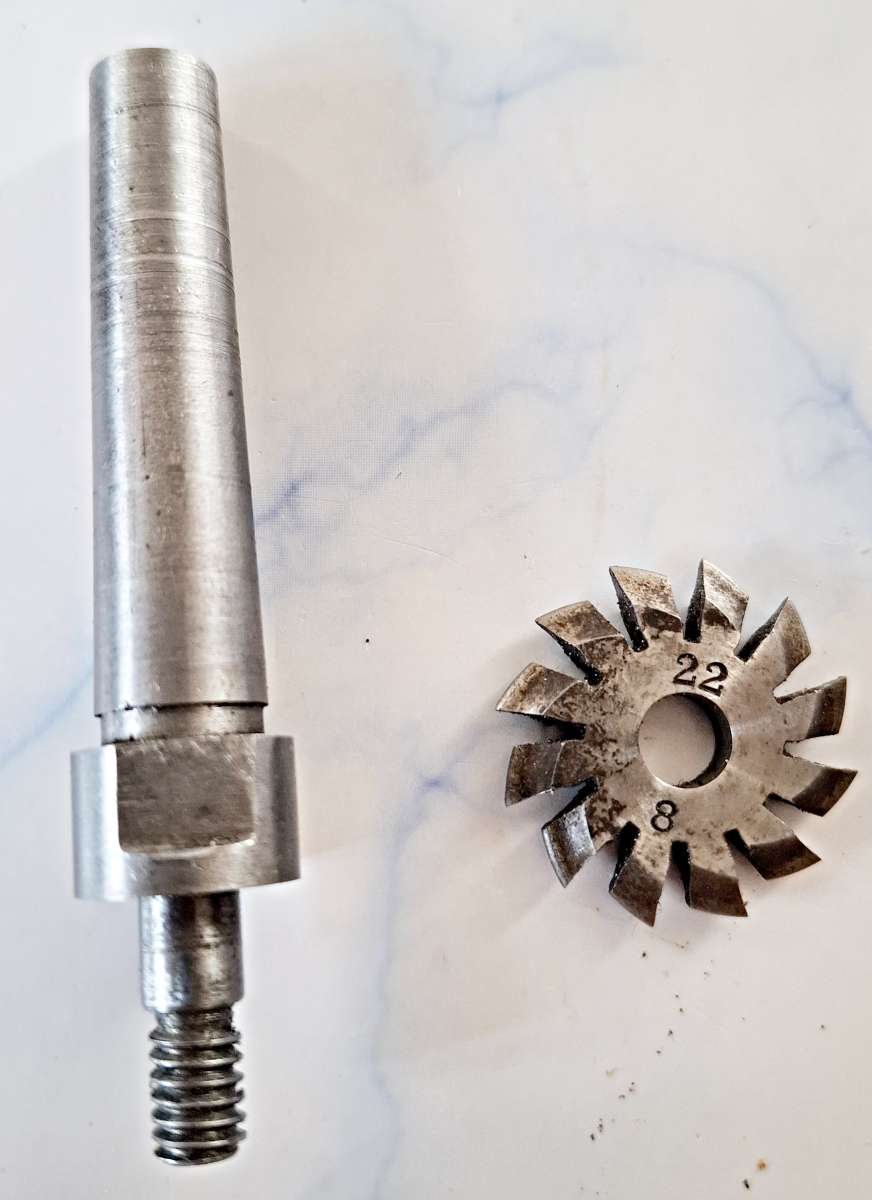
      Looking for 22 Dp number 8 involute cutter, seems they are hard to find, bore is 1/4″ and fits my MT1 drilling spindle.

      cutter

      #866478
      DC31k
      Participant
        @dc31k

        Please say what pressure angle you require.

        I think you will struggle to find one with that small bore.

        RDG and eBay have 14.5 PA with 1″ bore.

        #866484
        Huub
        Participant
          @huub

          If it is for a single gear, try making a gear cutter (fly cutter). For this you only need a milling machine.  There are more examples on YouTube.

          A number 8 cutter is intended for 12..13 tooth gear, quit small.
          22 DP is about module 1.155, a non standard value.
          Check the dimensions of the gear to be sure it is 22 DP.
          Besides the DP you also need to know the pressure angle of the gear. Looking at the cutter it probably is 20°. Another standard value could be 14.5°
          Use a CAD system (FreeCAD) and draw such a gear. Print it out and check if it matches the gear you want to make.

          These type of gear cutters can be resharpened. Just grind the flat cutting edge a bit and they perform as new.


          edit:

          That number 8 gear cutter could also be for a 135 tooth gear, depending on the table you use.

          #866493
          bernard towers
          Participant
            @bernardtowers37738

            If its an older cutter its more likely to be 14.5 deg, single tooth (fly cutter) is probably the way to go deppending on howmany you need to make.

            #866507
            Julie Ann
            Participant
              @julieann
              On Huub Said:

              That number 8 gear cutter could also be for a 135 tooth gear, depending on the table you use.

              It only depends upon whether the cutter is for imperial or metric. For imperial (DP) gears the number 8 cutter is used for 12 or 13 teeth. For metric (module) gears the cutters are numbered the other way round, so the number 8 cutter is for 135 teeth to a rack.

              Julie

              #866518
              vic newey
              Participant
                @vicnewey60017

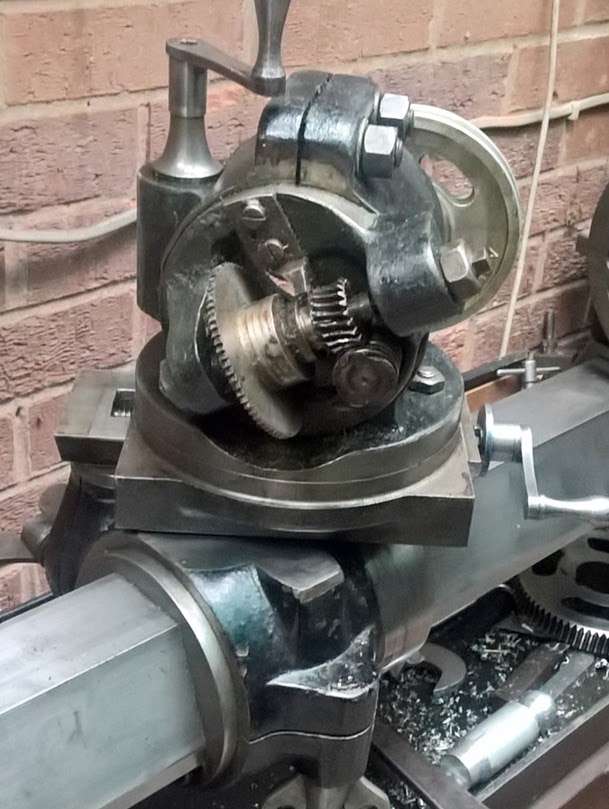
                Thanks for the replies, I am just making a copies of a small gear on my vintage lathe as a project having not tried cutting gears before.
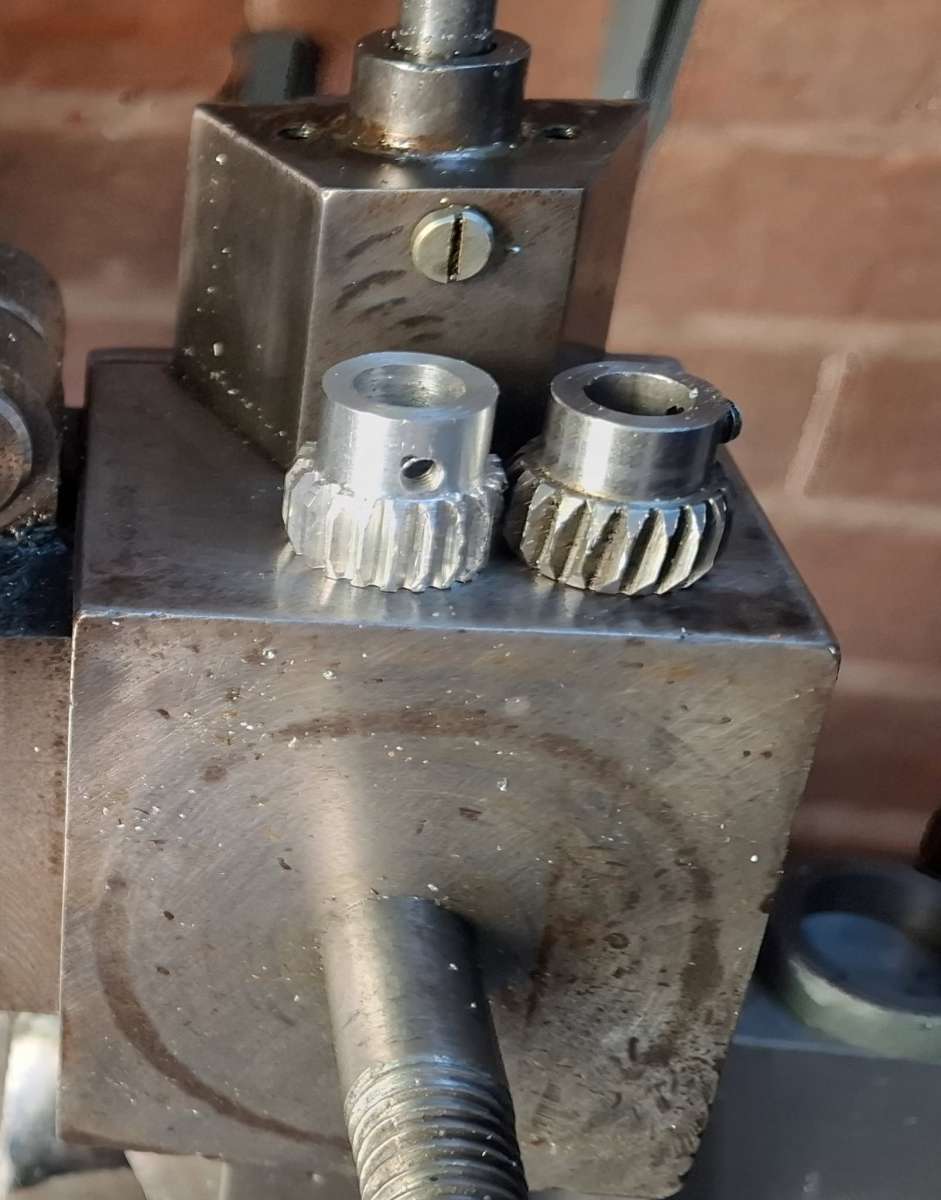
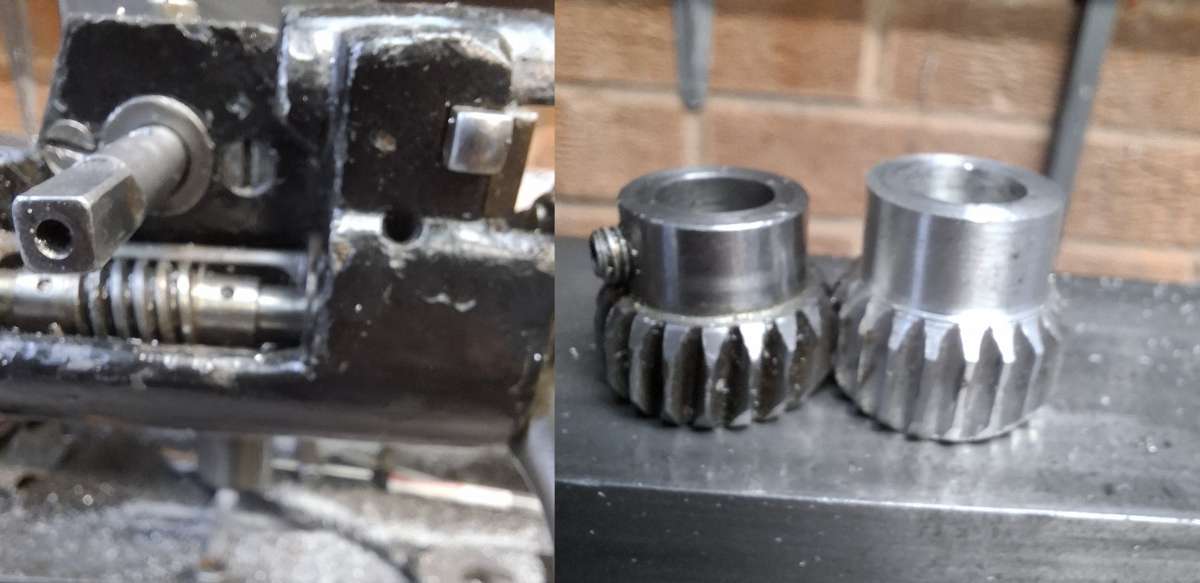
                I have cut two in Aluminium that work perfectly. the gear connects to a worm to power the cross-slide. However I wanted to make one in steel as is the original but the cutter is now worn although it cuts aluminium with ease. The lathe has a dividing attachment so it’s all self contained


                cutterpair

                #866520
                DC31k
                Participant
                  @dc31k

                  May I offer an observation?

                  If you count the visible teeth in the photograph and extrapolate to the full perimeter, it seems to total more than 13.

                  Clearly, the only person to give a definitive answer to the required tooth count is the OP, but it may be that a number 8 cutter is not the correct one.

                  #866526
                  JasonB
                  Moderator
                    @jasonb

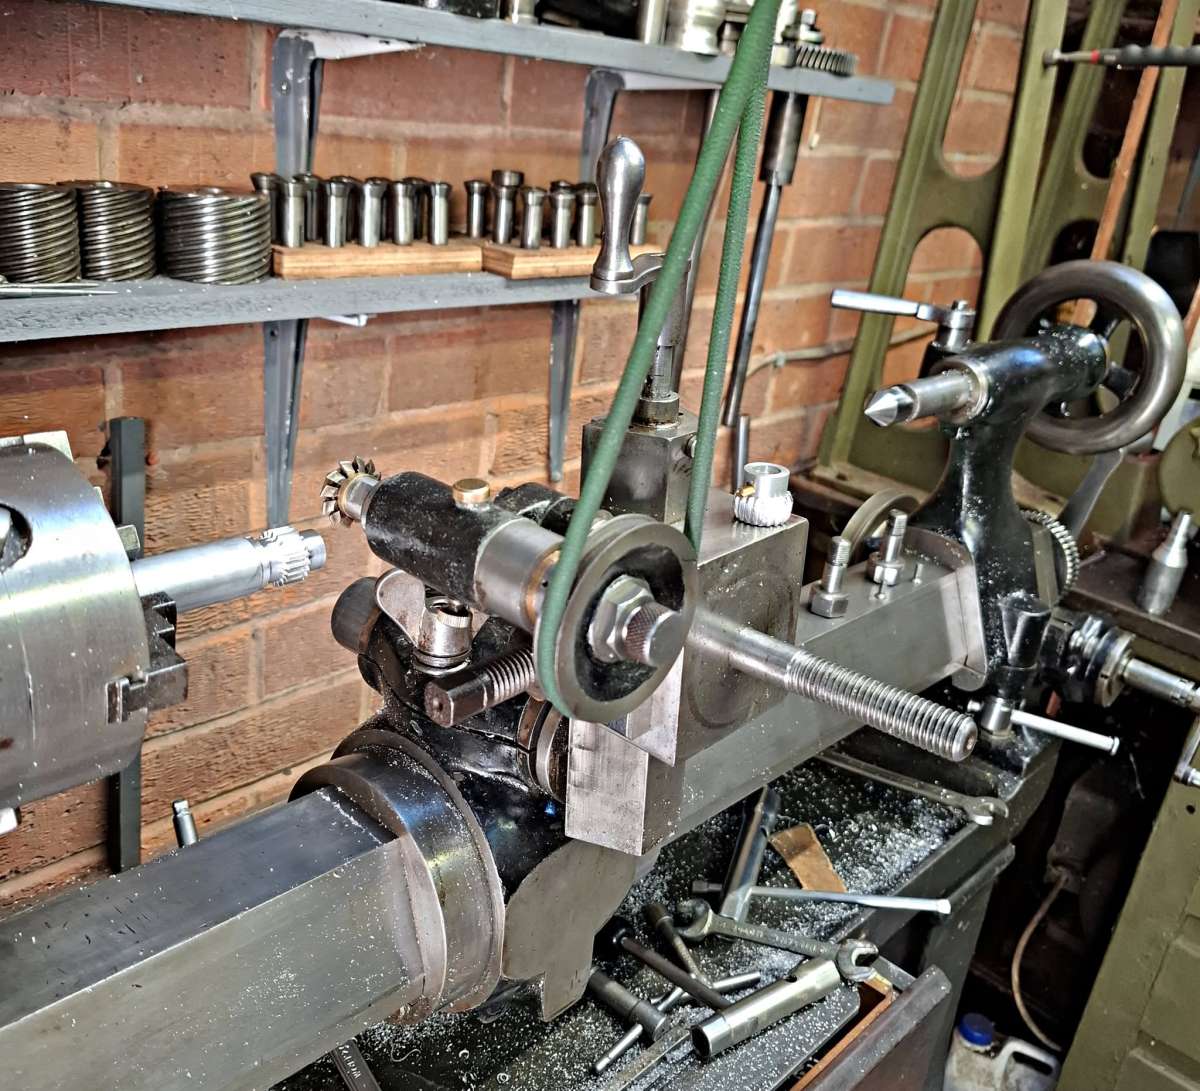
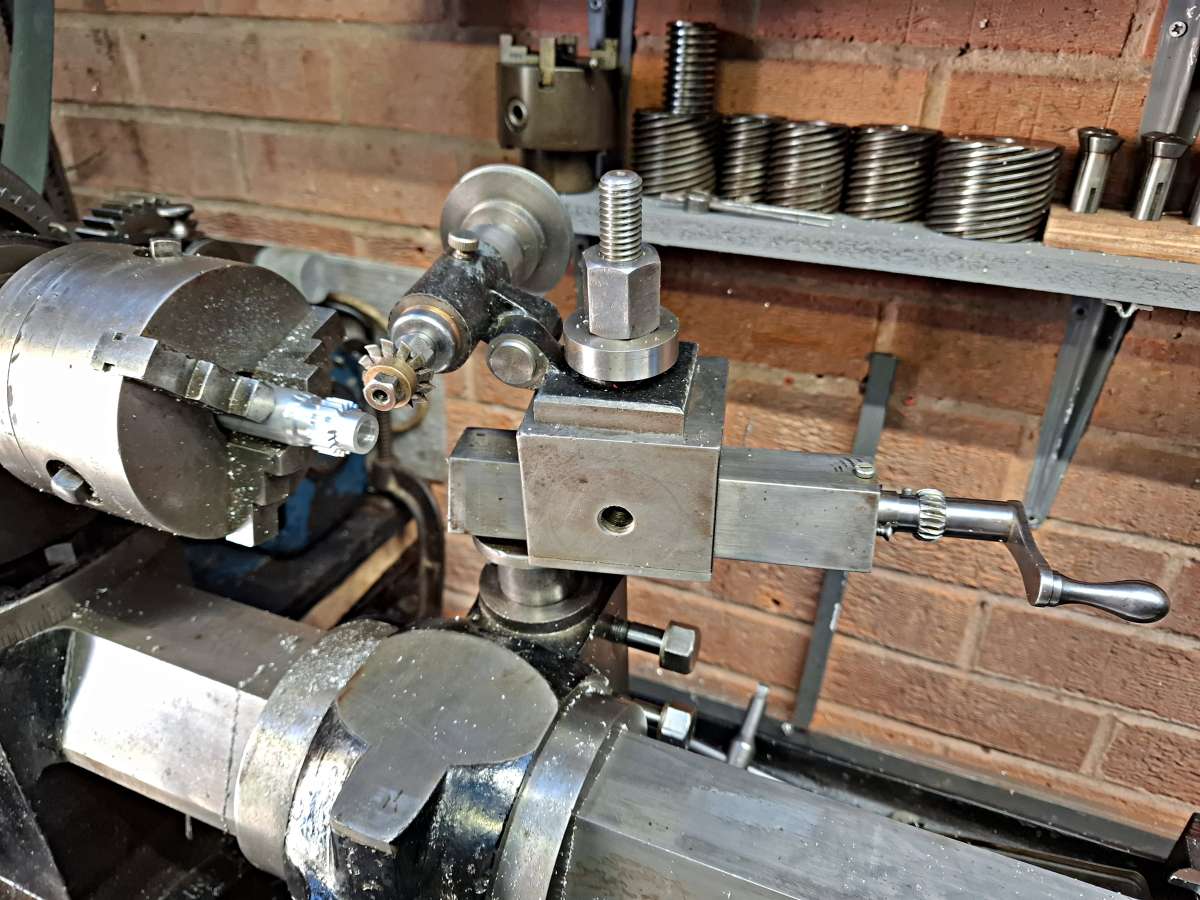
                    I’m also thinking the setup is wrong for a worm wheel.

                    The steel one has angled teeth and I would also hazard a guess they are cut with a hobbing action. Running a straight cut steel gear against your old worm may not do it a lot off good


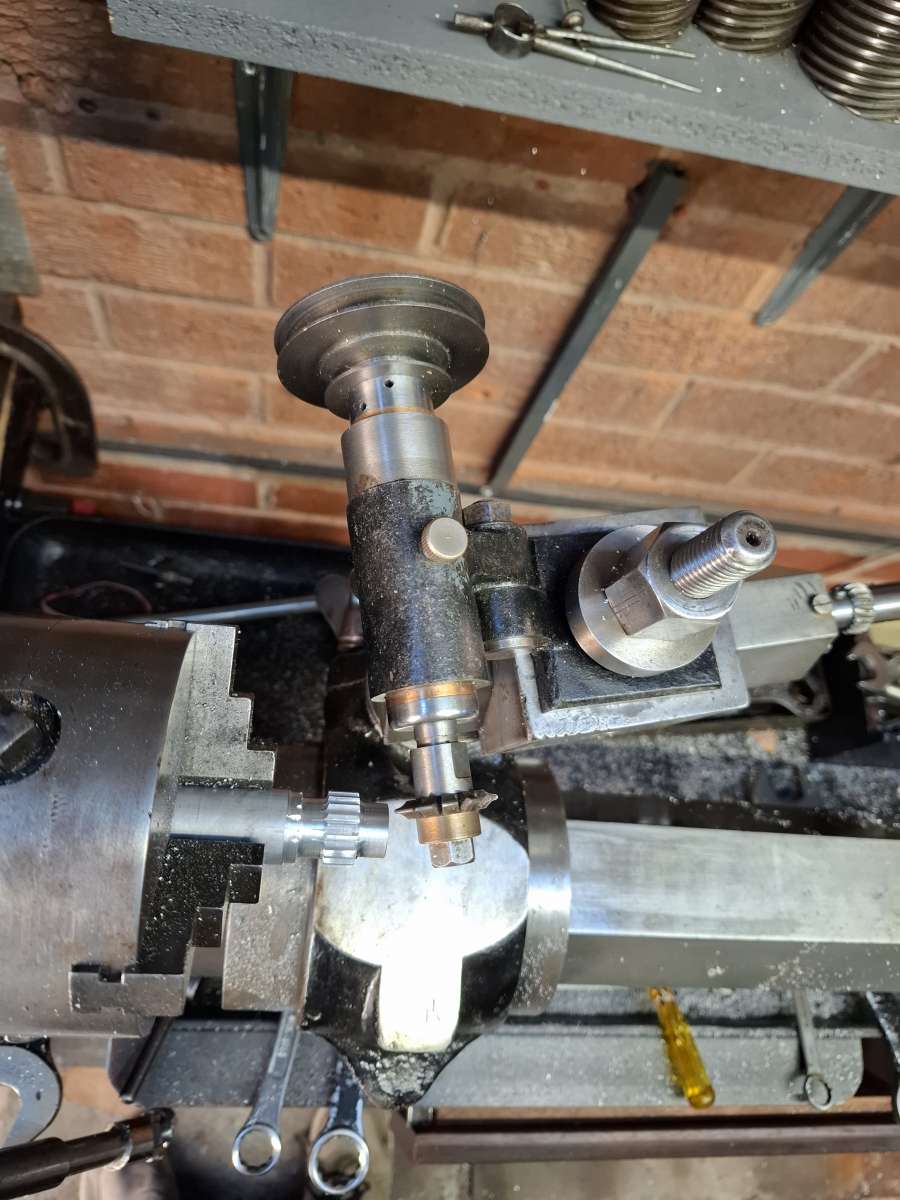
                    Looks like the cutter spindle may be set at an angle but is being fed along the bed as I can’t see any sign of a compound slide. May even be why it is not cutting steel as the cutter is being fed slightly sideways.

                    #866539
                    Dave Halford
                    Participant
                      @davehalford22513

                      According to “Lathes” Pittler was 14.5 deg PA and most of the worms are multi start as seen on your shelf.

                      If the cutter is set straight along the bed it should cut steel, feeding just hard enough to produce chips and produce a straight cut spur gear for mating to other straight cut gears. Don’t mix these with the ones from your lathe.

                      #866594
                      DC31k
                      Participant
                        @dc31k
                        On JasonB Said:

                        Looks like the cutter spindle may be set at an angle but is being fed along the bed…

                        I do not know how sophisticated the Pittler is, but if the carriage feed were via the leadscrew AND the leadscrew is appropriately geared to the spindle*, the proper realtive motion necessary for a helical gear could be possible.

                        * in terms of screwcutting, it would be a super coarse pitch, with a tiny amount of spindle rotation producing a huge amount of longitudinal movement, hence why the leadscrew needs to be the driver (c.f. cutting the thread on a Quorn column).

                        #866610
                        vic newey
                        Participant
                          @vicnewey60017
                          On DC31k Said:
                          On JasonB Said:

                          Looks like the cutter spindle may be set at an angle but is being fed along the bed…

                          I do not know how sophisticated the Pittler is, but if the carriage feed were via the leadscrew AND the leadscrew is appropriately geared to the spindle*, the proper realtive motion necessary for a helical gear could be possible.

                          * in terms of screwcutting, it would be a super coarse pitch, with a tiny amount of spindle rotation producing a huge amount of longitudinal movement, hence why the leadscrew needs to be the driver (c.f. cutting the thread on a Quorn column).

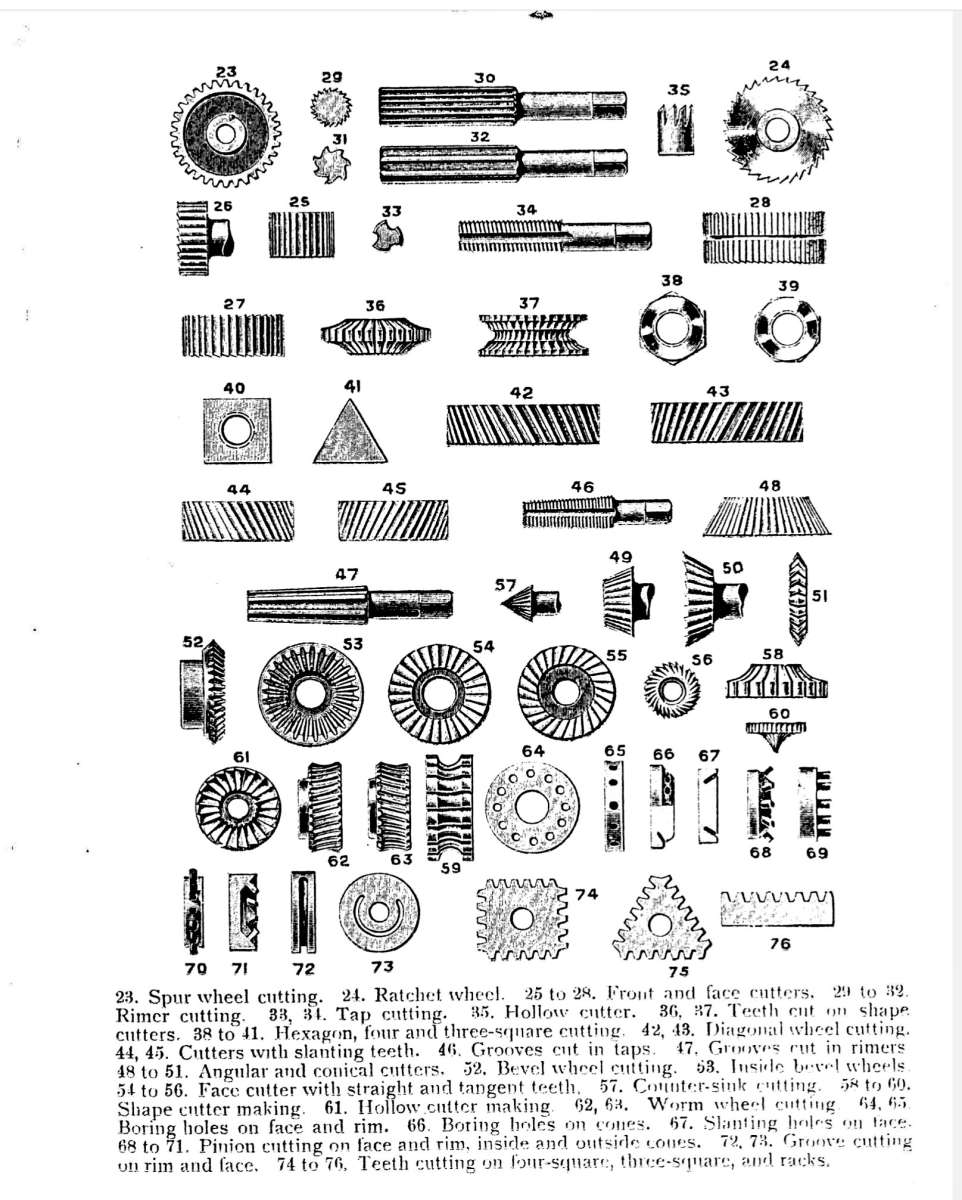
                          The machine is capable of a multitude of different tasks, over 200 in fact even though it’s dated to 1894. I am simply trying out gear cutting methods and in this photo with the spindle on top the angle can be adjusted and advanced by the cross slide. See the catalogue image of what this machine is capable of

                          I have an original equipment heavy drum  type cutter attachment I featured in another post this can swivel the cutter at any angle from horizontal to vertical and has it’s own slide for advancement
                          However I only have a number of plain cutters/ slitting saws etc and not prepared to spend £25 upwards for a cutter just to play around with.

                          I know I asked where I might find a cutter to fit the small drill spindle but will persevere with the cutter I have and make another one in aluminium.crossside

                          #866611
                          vic newey
                          Participant
                            @vicnewey60017

                            As a point of interest this machine is able to cut any of the examples in this catalogue image, with the correct cutters of course

                            examples

                            #866636
                            John Haine
                            Participant
                              @johnhaine32865

                              Home

                              Might sharpen you cutter

                              #866693
                              vic newey
                              Participant
                                @vicnewey60017

                                I’ve done another one which is better than the original and it works perfectly.  I repositioned the spindle and set it on the top of the cross slide and advanced the tool via it’s handle, the slide being slightly askew from the main lathe bed

                                The previous owner made the little gear as the original was lost but had nothing to copy, I note that the teeth are quite narrow at the tip although the worm is coarse. I made a very short video of me testing it using a drill.
                                Normally it works off a universal joint but as I have the lathe set up for indexing the headstock drive belt is slackened off.

                                I am now going to try making one in Bronze as I still think steel is going to struggle. The only problem with Aluminium is the grub screw on such a short thread, the gear itself has 20 teeth although I am told the cutter is  for 12-13 tpi but nevertheless it works like a dream

                                https://youtu.be/1DqqcUi8DRo?si=fg5E8JE5LjBgUdjV


                                final cut

                                #866736
                                Huub
                                Participant
                                  @huub

                                  The only problem with Aluminium is the grub screw on such a short thread

                                  Make the shaft thicker or use a smaller grub screw having a finer pitch.
                                  Seem to work OK.

                                  #866759
                                  vic newey
                                  Participant
                                    @vicnewey60017
                                    On Huub Said:

                                    The only problem with Aluminium is the grub screw on such a short thread

                                    Make the shaft thicker or use a smaller grub screw having a finer pitch.
                                    Seem to work OK.


                                    Barely enough room to make it thicker though as it’s level with the bottom of the teeth. l think l will make one in Bronze as it will be easier on the cutter than steel and l have a suitable piece to use

                                    #866775
                                    John Haine
                                    Participant
                                      @johnhaine32865

                                      As I suggested above, you might ask PP Thornton if they could sharpen your cutter as it’s quite small.  Though they generally sharpen cycloidal cutters, either type only needs grinding on the front face of the teeth so the tooth shape is irrelevant.

                                      #866784
                                      Michael Gilligan
                                      Participant
                                        @michaelgilligan61133

                                        FWIW

                                        The mighty Google directed me to this page:

                                        Making spur gears using a dividing head

                                        See the notes on Brown & Sharpe cutters for small gears

                                        … and also to this useful video:

                                        .

                                        MichaelG.

                                        #866790
                                        Bazyle
                                        Participant
                                          @bazyle

                                          It should be possible to make a simple guide in hard plastic that enables you to touch up the teeth with a diamond file. To avoid clogging the file design the guide so that the guide faces bear on the file ends which are wrapped in Sellotape.
                                          3D printing for the guide comes to mind.

                                          #866803
                                          vic newey
                                          Participant
                                            @vicnewey60017
                                            On Michael Gilligan Said:

                                            FWIW

                                            The mighty Google directed me to this page:

                                            Making spur gears using a dividing head

                                            See the notes on Brown & Sharpe cutters for small gears

                                            … and also to this useful video:

                                            .

                                            MichaelG.

                                            An interesting video for sure, it explains things very clearly. The problem is that with my current set up milling spindle the bore is only 1/4″ I have an original equipment drilling spindle that is much more robust but it only takes collets. My other original equipment multi angle drum type milling attachment with a geared head and it’s own cross slide takes 25mm bore which cutters are around £25 each from RDG so just to experiment with gear cutting it’s a bit much unless I had something I actually needed to make, repair or replace something missing etc.

                                            I’m not sure if sending the cutter off for sharpening is worthwhile either as it will probably cost half the price of a new 1″ cutter so I am going to look for a more reasonable 25mm cutter


                                            unnamed

                                            #866805
                                            Juddy
                                            Participant
                                              @juddy
                                              #866808
                                              vic newey
                                              Participant
                                                @vicnewey60017
                                                On Juddy Said:

                                                Try Home and workshop for cutters: https://www.homeandworkshop.co.uk/stock-item/dp-gear-cutters/246/


                                                They have a huge selection there ! but no mention of bore size as I can see on RDG there are 22mm and 16mm as well as 1″
                                                Those are £20 each and not sure if VAT is included so with shipping they would end up similar to RDG £25 inc post

                                                #866812
                                                Michael Gilligan
                                                Participant
                                                  @michaelgilligan61133

                                                  I suspect that you need to make a difficult choice, Vic

                                                  The [original Pittler-supplied?] cutter has a 1/4” bore, but Horological cutters have 7mm … so not only is it a rare item but it might be difficult to get professionally sharpened … £££

                                                  I wish you success with whatever approach you take.

                                                  MichaelG.

                                                  #866817
                                                  vic newey
                                                  Participant
                                                    @vicnewey60017
                                                    On Michael Gilligan Said:

                                                    I suspect that you need to make a difficult choice, Vic

                                                    The [original Pittler-supplied?] cutter has a 1/4” bore, but Horological cutters have 7mm … so not only is it a rare item but it might be difficult to get professionally sharpened … £££

                                                    I wish you success with whatever approach you take.

                                                    MichaelG.

                                                    Thanks Michael, the one I just used was made by Potts, UK 1930’s era so not a Pittler one, I have several cutters with 1/4″ bore and a number of MT1 mandrels to fit them, they came with another smaller Pittler lathe I have. Not really a problem as I already pointed out I am just enjoying trying out some of the things the machine is capable of so now will try something different I think

                                                    #866827
                                                    Michael Gilligan
                                                    Participant
                                                      @michaelgilligan61133

                                                      Just for the record … here is Brown’s patent:

                                                      https://worldwide.espacenet.com/patent/search?q=pn%3DUS45294A

                                                      MichaelG.

                                                    Viewing 25 posts - 1 through 25 (of 27 total)
                                                    • Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.

                                                    Latest Replies

                                                    Home › Forums › Workshop Techniques › Topics

                                                    Viewing 25 topics - 1 through 25 (of 25 total)
                                                    Viewing 25 topics - 1 through 25 (of 25 total)

                                                    View full reply list.