
Coventry die head
Coventry die head
- This topic has 6 replies, 6 voices, and was last updated 16 October 2026 at 10:32 by
 bernard towers.
 bernard towers.
 lug lord
 Huub
 bernard towers
 Andrew Crow
 JohnF
 Clive Foster
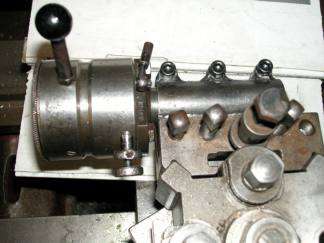
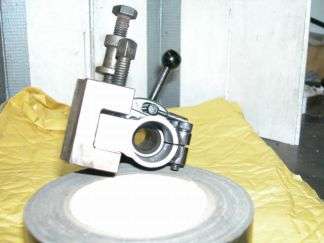
- Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.
Latest Replies
-
- Topic
- Voices
- Last Post
-
-
CAST IRON JOINING
Started by:
ian Holdsworth
in: Beginners questions
- 7
-
16 October 2026 at 11:26
Trevor Drabble 1
-
Weight of Myford Super 7 / ML7R
Started by:
Andrew Tinsley
in: General Questions
- 2
-
16 October 2026 at 11:11
Andrew Tinsley
-
Angled d-bit / machinist reamer?
Started by:
Fulmen
in: Workshop Tools and Tooling
- 12
-
16 October 2026 at 10:36
bernard towers
-
Coventry die head
Started by:
lug lord
in: Workshop Techniques
- 6
-
16 October 2026 at 10:32
bernard towers
-
Does anyone have any info about these vices
1
2
Started by:
bjcolyer
in: Introduce Yourself – New members start here!
- 12
-
16 October 2026 at 10:20
bjcolyer
-
Picomite Version 7 – better than Arduino?
Started by:
IanT
in: Electronics in the Workshop
- 8
-
16 October 2026 at 09:29
IanT
-
Myford ml7r
Started by:
lug lord
in: Introduce Yourself – New members start here!
- 1
-
16 October 2026 at 08:06
lug lord
-
Super Simplex Build
Started by:
Peter Hoerlein
in: Work In Progress and completed items
- 7
-
15 October 2026 at 23:29
Peter Hoerlein
-
ML7 change gear caluclator
Started by:
drnewcomb
in: Manual machine tools
- 3
-
15 October 2026 at 21:11
peak4
-
Lathe turning tool nomenclature
Started by:
JA
in: Workshop Tools and Tooling
- 9
-
15 October 2026 at 19:48
old mart
-
Model Engineering Website
Started by:
Geoff Rogers
in: General Questions
- 5
-
15 October 2026 at 16:14
JA
-
Parkside Electronics
Started by:
Clive Steer
in: General Questions
- 8
-
15 October 2026 at 13:13
shayodon
-
Model Engineer Magazine Collection
Started by:
mfengine1
in: Books
- 11
-
15 October 2026 at 12:13
bcaddle62
-
John Haining 2″ Ruston
Started by:
Pixel_Porpoise
in: Help and Assistance! (Offered or Wanted)
- 2
-
15 October 2026 at 11:32
Pixel_Porpoise
-
Scroll Saw Blades for Steel
1
2
Started by:
James A
in: Workshop Tools and Tooling
- 15
-
15 October 2026 at 10:32
larry phelan 1
-
Searching for roller chain with pitch 2.5 mm
Started by:
Werner Habbel
in: Hints And Tips for model engineers
- 4
-
15 October 2026 at 10:16
Werner Habbel
-
Model Engineering Website
Started by:
Neil A
in: The Tea Room
- 1
-
15 October 2026 at 10:03
Neil A
-
Lathe arriving – source some practice materials
1
2
Started by:
starjump
in: Beginners questions
- 17
-
15 October 2026 at 09:48
starjump
-
Greenbat 3 ton battery loco
Started by:
Pippin
in: Work In Progress and completed items
- 2
-
15 October 2026 at 08:52
Pippin
-
Printed circuit boards
Started by:
duncan webster 1
in: Electronics in the Workshop
- 7
-
14 October 2026 at 21:33
duncan webster 1
-
What Are the Most Practical Ways to Make Manufacturing More Sustainable?
Started by:
andrew998
in: Workshop Techniques
- 6
-
14 October 2026 at 16:41
ega
-
Home workshop site down?
Started by:
Andrew Tinsley
in: General Questions
- 4
-
14 October 2026 at 16:39
Brian Baker 2
-
Sealant for bolting a dome casting to a model boiler
Started by:
Greensands
in: Hints And Tips for model engineers
- 6
-
14 October 2026 at 15:37
Derek Drover
-
Involute cutters
Started by:
michael howarth 1
in: General Questions
- 2
-
14 October 2026 at 14:59
not done it yet
-
Powerfeeders
Started by:
larry phelan 1
in: Help and Assistance! (Offered or Wanted)
- 8
-
14 October 2026 at 13:00
duncan webster 1
-
CAST IRON JOINING
 ian Holdsworth
 Trevor Drabble 1
 Andrew Tinsley
 Fulmen
 lug lord
 bjcolyer
 IanT
 Peter Hoerlein
 drnewcomb
 peak4
 JA
 old mart
 Geoff Rogers
 Clive Steer
 shayodon
 mfengine1
 bcaddle62
 Pixel_Porpoise
 James A
 larry phelan 1
 Werner Habbel
 Neil A
 starjump
 Pippin
 duncan webster 1
 andrew998
 ega
 Brian Baker 2
 Greensands
 Derek Drover
 michael howarth 1
 not done it yet