
Slitting Saws?

Slitting Saws?

Home › Forums › Workshop Tools and Tooling › Slitting Saws?

Viewing 21 posts - 51 through 71 (of 71 total)
  • Author
    Posts
  • #745468
    Michael Gilligan
    Participant
      @michaelgilligan61133

      Good analysis, Jason

      Personally, however, I remain much more interested in how some of these cheap saws come to be so badly made … at the moment this is a purely intellectual exercise for me [because I have no facility to use the ones I already own]

      If we can get to understand that … it might help us identify what features typify the bad-uns.

      MichaelG

      #745472
      Anonymous
        #745474
        JasonB
        Moderator
          @jasonb

          Unground parts of the teeth/gullet may be one feature to avoid but unlikely to show on any online site particularly the fine toothed one like the OP bought, so hard to avoid if web shopping. Though I can’t find them on their website today!

          #745479
          Bo’sun
          Participant
            @bosun58570
            #745487
            JasonB
            Moderator
              @jasonb

              It was a rare occasion but I did make an adaptor so I can mount the metric ones on the MT3 arbor that I use on the X3, video was with the ARC arbor in the SX2.7.

              A bit less rushed this morning and I would say it could be a bit more eccentric about 0.01mm but that is still a big improvement over what you have.

              Interesting to work out the cutting speeds and chip loads. For that second power feed cut that was the faster of the two I make that about 150mm/min feed @350rpm.

              It’s a 24T blade so that works out at a chip load of 0.018mm (0.0007″) which is more than the eccentricity of the blade so all will be cutting to some extent and it did sound better as did the first when I wound up the power feed a bit more part way through the cut.

              For something like your clevis it would not be that easy to feed in at such a rate and then stop at the right depth. A better option would have been to set the depth of the slot by touching off against the end of the work, feeding in as required and then making the cut in the Y direction where you can wind away at speed and not worry about when to stop as you are just passing right through the metal.e

              #745492
              KEITH BEAUMONT
              Participant
                @keithbeaumont45476

                I have long since thought that this is not a quality problem and that there is a reason other than sloppy manufacture for the concentricity with slitting saws. In spite of all the traffic, no one has appeared to say, I buy from “x” and they are allways perfect.  This morning I phoned the Company in Michael’s link,of a few days ago and asked to speak to a technician regarding concentricity. He was very helpful, but assured me that they work to the British Standard of +/- 0.001″ on concentricity,across their whole range. He said that when they get complaints on this subject,it is always down to the machine or arbor having run-out.

                So it would seem to be a quality thing and we know where to buy them if we want perfection!

                Keith.

                #745498
                SillyOldDuffer
                Moderator
                  @sillyoldduffer
                  #745501
                  Michael Gilligan
                  Participant
                    @michaelgilligan61133

                    Thanks, Keith … Your telephone call was evidently the right approach, as I have not yet received any reply to the eMail that I sent to them on Sunday evening.

                    MichaelG.

                    #745503
                    JasonB
                    Moderator
                      @jasonb
                      #745505
                      Michael Gilligan
                      Participant
                        @michaelgilligan61133
                        #745512
                        Neil Lickfold
                        Participant
                          @neillickfold44316

                          Cutter grinders are not cheap, like what was in the video link. They do allow for custom tools though that can sometimes be an advantage. Slitting saws and side face cutters are almost a forgotten tool. Sometimes you can get bargains from auctions etc where often the saws and side face cutters are almost not bid on.

                          #745531
                          Nicholas Farr
                          Participant
                            @nicholasfarr14254

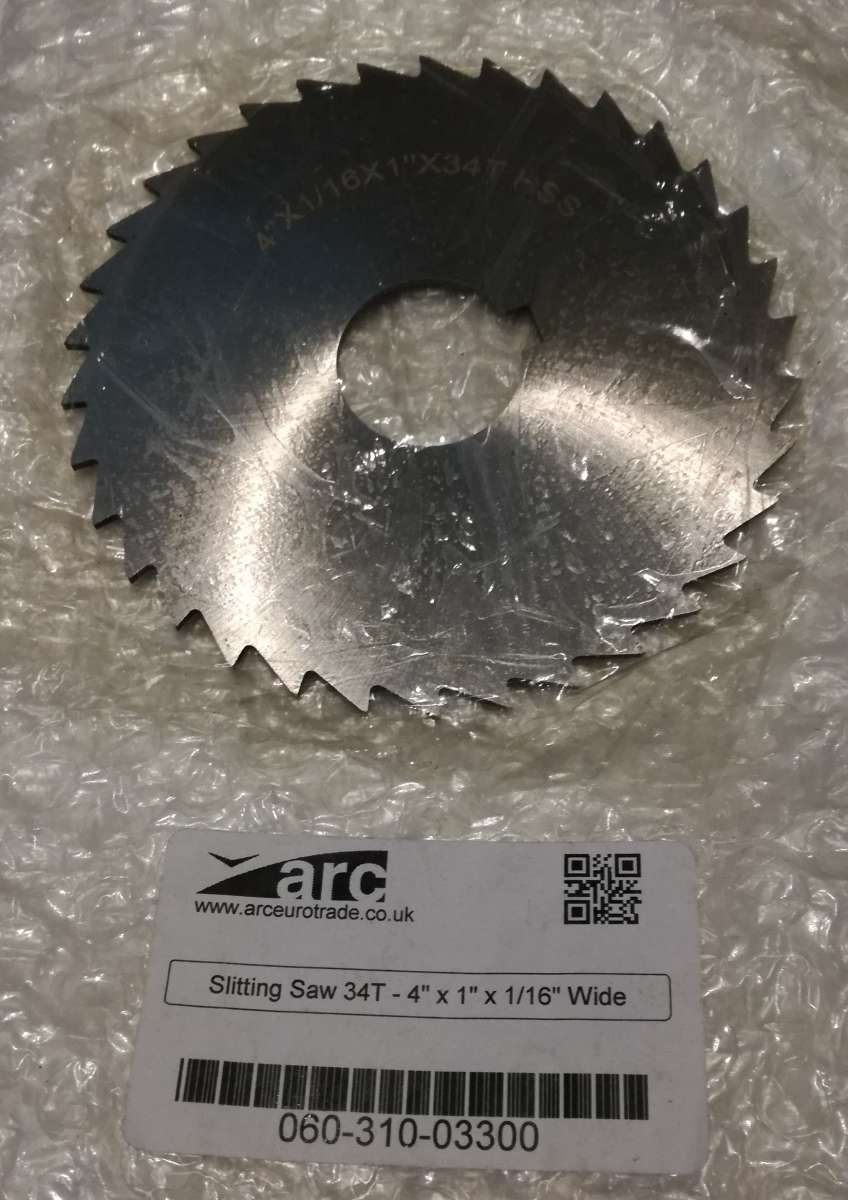
                            Hi, well out of curiosity, I checked my arbore for runout, and it has in one spot, 0.00025″/ 0.00635mm high, which I’m not going to worried about. I mounted an Arc 42 x 1/16″ x 34T slitting saw, which has never been out of the thin poly bag, let alone never been used, and has no shake at all on the arbore, and I then checked the teeth in the same way as JasonB has shown, after getting my dial gauge to 0 onto one of the teeth, and then turning the spindle slowly by hand, I got a variation  of some of the teeth not quite making the needle reaching back to the 0 position, while others moved it to almost 0.0015″ / 0.0381mm past the 0 position, some of these readings were in-between each other, while some came in pairs, but at least two teeth, not even close to each other. only just moved the the needle, I rotated it at least three full turns, and the readings were very much the same each time. I have no problem with these results either, and I’m very confident that it will cut okay when it gets used.

                            slitting saw

                            Regards Nick.

                            #745541
                            SillyOldDuffer
                            Moderator
                              @sillyoldduffer
                              #745546
                              JasonB
                              Moderator
                                @jasonb

                                I’m not sure that slitting saws are a forgotten tool, I seen several videos of 5 axis machines making small parts and all are held in the compact self-centering CNC vices and the last op is to “part off” with a pass or two of a slitting saw to leave a wafer-thin piece of metal allowing the part to simply be broken off.

                                I have linked to this one before, the saw blade is about £500 plus whatever the arbor costs.


                                #745553
                                Bo’sun
                                Participant
                                  @bosun58570

                                  Jason,

                                  Referring to you post earlier.  I did cut the clevis slot on the Y axis, but it was somewhat painful with around half a millimeter of runout.

                                  While it did the job, it’s still disappointing.  Especially when other suppliers (or at least one) can clearly do considerably better for around the same price.

                                  #745558
                                  Anonymous
                                    #745561
                                    Bo’sun
                                    Participant
                                      @bosun58570

                                      Andrew,

                                      Yes, they “seem to cut OK” in as much as I ended up with a slot in a relatively small piece of 1/4″ dia brass.  How they’d fare in something larger and somewhat tougher is anybody’s guess.  You’re quite correct in relating slitting saw standards to S&F milling cutters, but that’s where in this case, cost clearly enters the discussion.  However, around half a millimetre of runout, even in an inexpensive cutter, seems excessive.  Even if I’m being generous, I still have over 100 teeth not doing anything.

                                      #745685
                                      Anonymous
                                        On Bo’sun Said:

                                        …around half a millimetre of runout, even in an inexpensive cutter, seems excessive.

                                        No question about that, it is totally unacceptable. The accuracy/price line is non-linear. It shouldn’t be too difficult to hit, say, less than 0.1mm eccentricity. I’d be upset if I couldn’t do better than that at home. Hitting 0.01mm eccentricity should be possible without too much expense in a commercial operation. Of course if 0.001mm eccentricity is needed then it is going to cost!

                                        One thing that hasn’t been mentioned is that sometimes a slitting saw needs to cut to specific depth, which will obviously be messed up if there is significant eccentricity.

                                        I assume that you know that fine pitch slitting saws are designed for shallow grooves, such as screwdriver slots on screwheads? For deeper cuts a coarse pitch slitting saw is needed so that the gullet doesn’t get choked.

                                        Andrew

                                        #745694
                                        JasonB
                                        Moderator
                                          @jasonb

                                          I deal with the depth issue by touching off the rotating saw on the edge of the job and feeding in from that point. Doing it static could cause a problem if things are too far off.

                                          #745709
                                          Michael Gilligan
                                          Participant
                                            @michaelgilligan61133
                                            #745769
                                            Bo’sun
                                            Participant
                                              @bosun58570
                                            Viewing 21 posts - 51 through 71 (of 71 total)
                                            • Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.

                                            Latest Replies

                                            Viewing 25 topics - 1 through 25 (of 25 total)
                                            Viewing 25 topics - 1 through 25 (of 25 total)

                                            View full reply list.