
Have I got 12-28 UNF wrong or has Völkel?
Have I got 12-28 UNF wrong or has Völkel?
- This topic has 29 replies, 12 voices, and was last updated 17 September 2026 at 19:12 by
 peak4.
 peak4.
 JasonB
 Bill Phinn
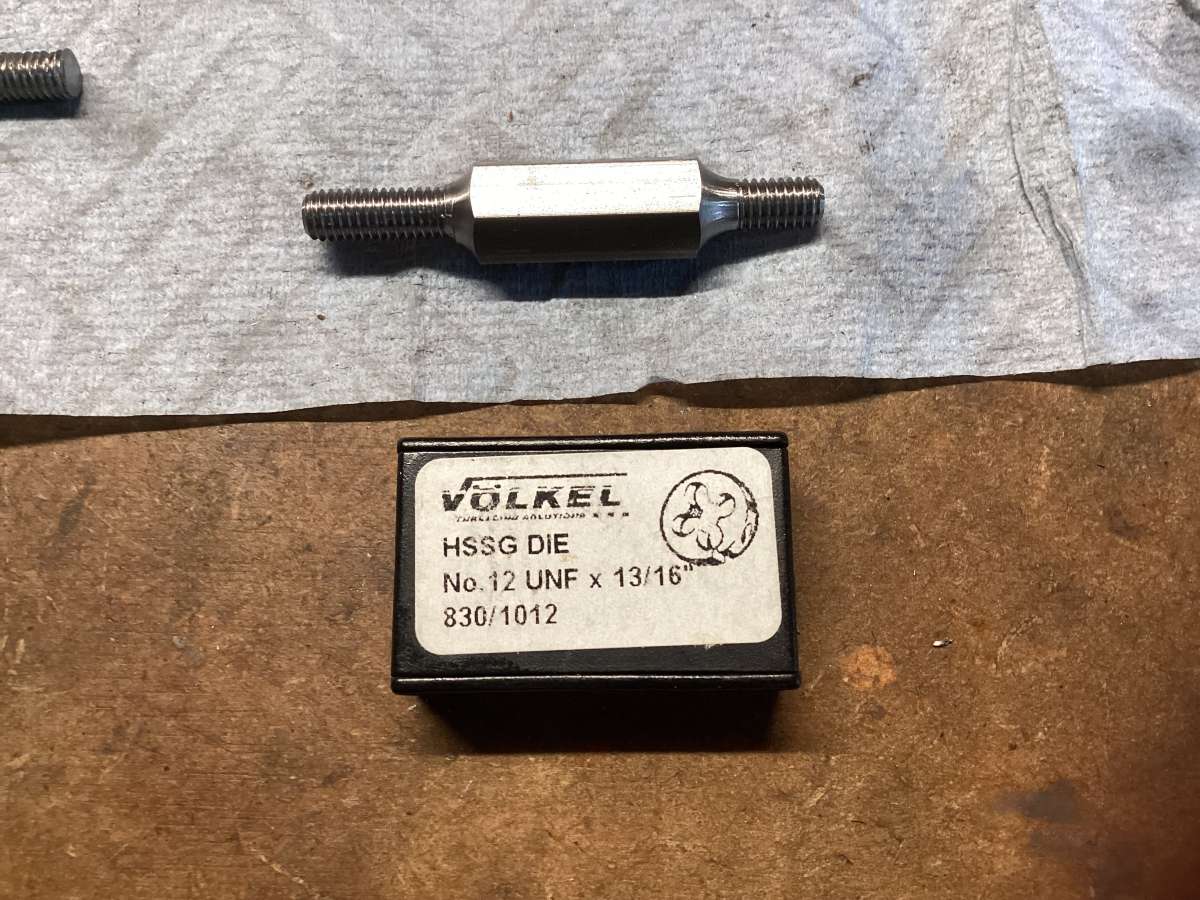
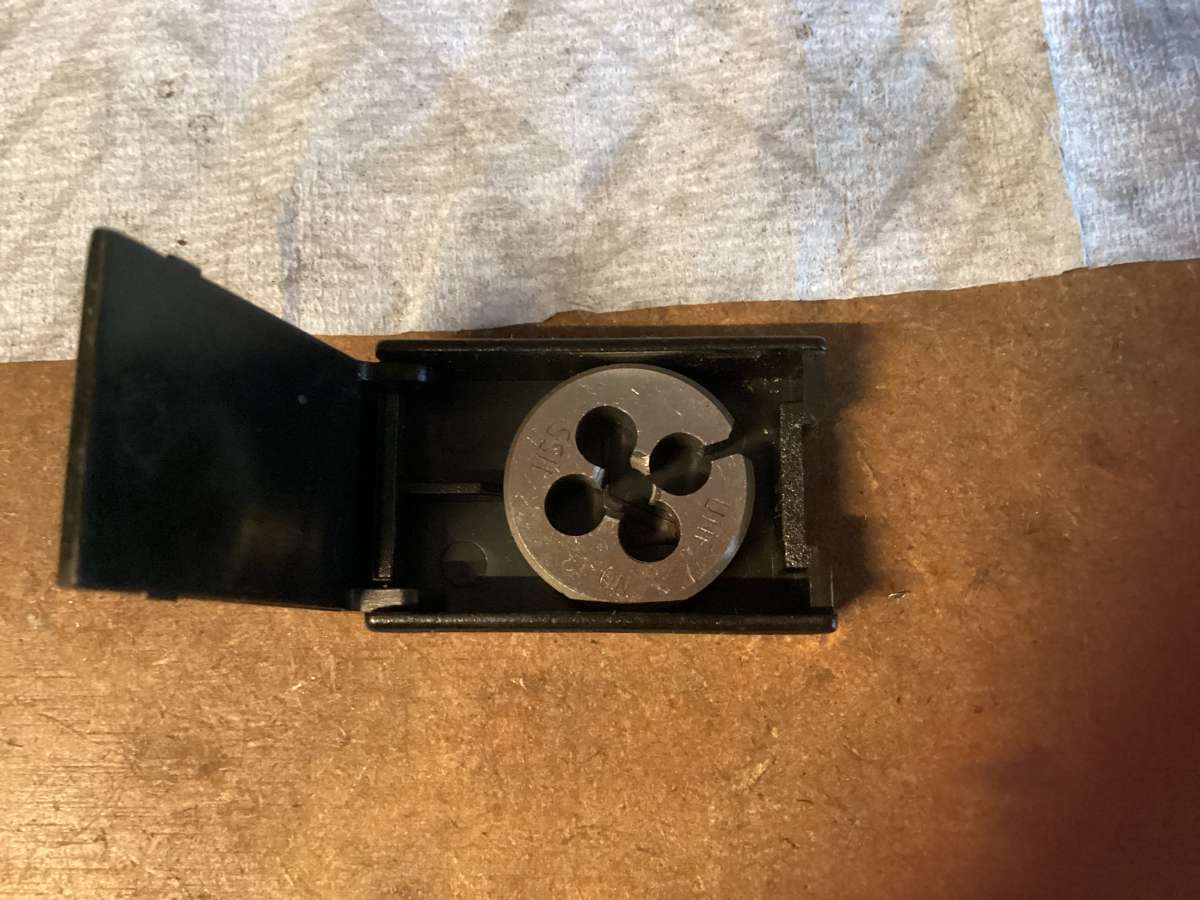
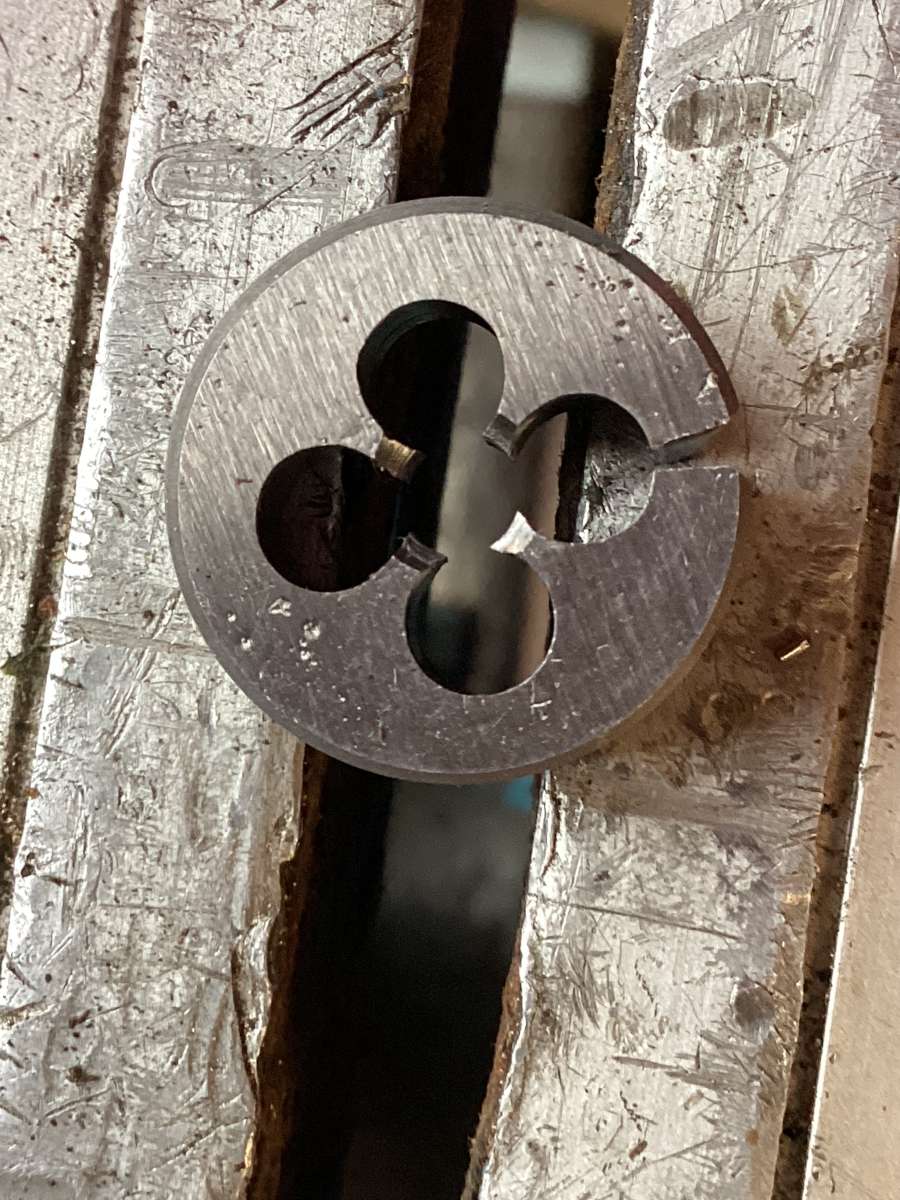
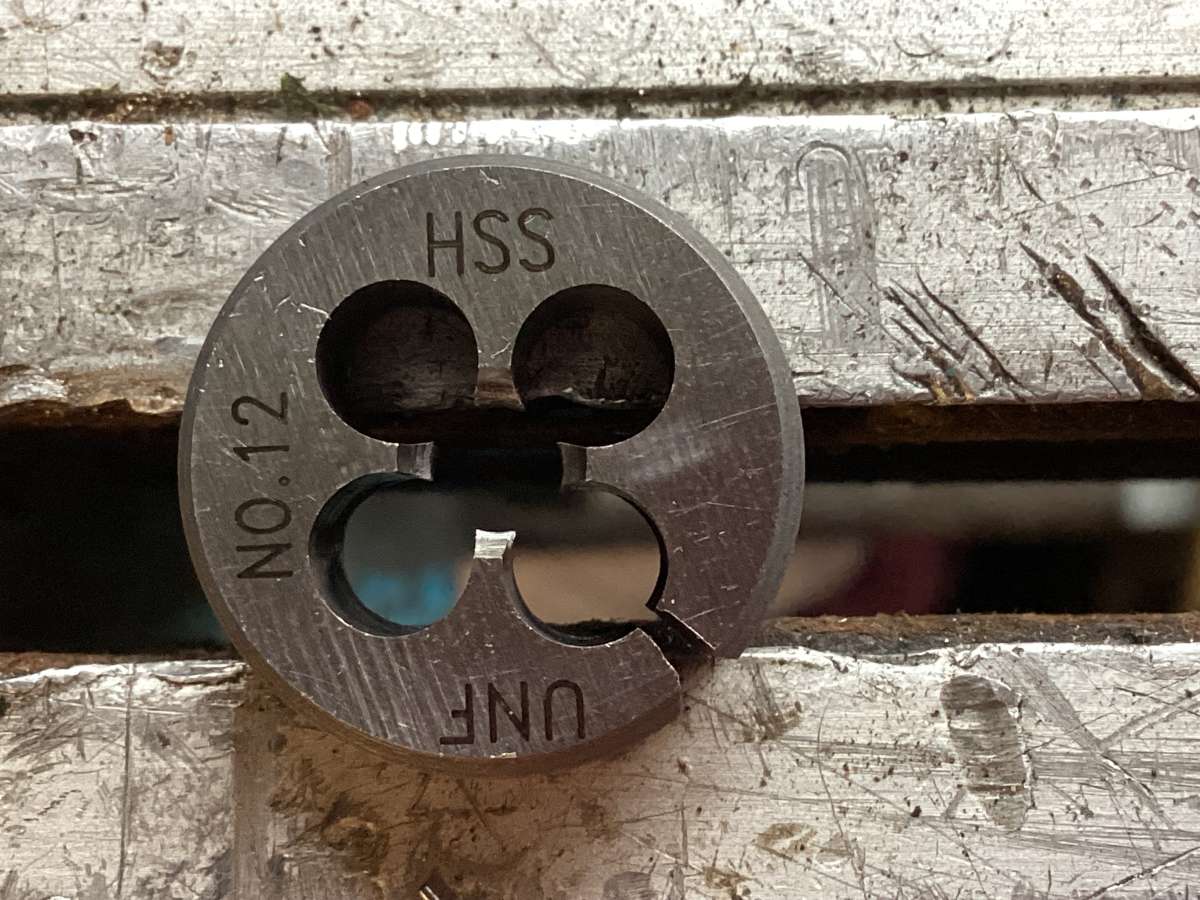 ETA: Jason, the silver steel was marked 5.5mm, not 7/32”.
 bernard towers
 Howard Lewis
 peak4
- Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.
Latest Replies
-
- Topic
- Voices
- Last Post
-
-
The lazy man’s fly cutter
Started by:
Sonic Escape
in: Workshop Tools and Tooling
- 4
-
9 October 2026 at 11:32
Dave Halford
-
Preview of whats coming in Freecad 26.3
Started by:
Russell Eberhardt
in: CAD – Technical drawing & design
- 8
-
9 October 2026 at 11:20
blowlamp
-
New Member
Started by:
starjump
in: Introduce Yourself – New members start here!
- 4
-
9 October 2026 at 10:55
starjump
-
Silver solder.
Started by:
Michael Callaghan
in: General Questions
- 9
-
9 October 2026 at 10:47
Dave S
-
Minnie Traction Engine – Damper Hinge Plate
Started by:
Dominic Bramley
in: Traction engines
- 6
-
9 October 2026 at 10:29
Andy Stopford
-
Moving Targets
Started by:
Michael Gilligan
in: The Tea Room
- 7
-
9 October 2026 at 10:25
noel shelley
-
Dore Boring Bar set
Started by:
Andrew Tinsley
in: General Questions
- 3
-
9 October 2026 at 09:56
Andrew Tinsley
-
Picomite Version 7 – better than Arduino?
Started by:
IanT
in: Electronics in the Workshop
- 7
-
9 October 2026 at 08:44
mike barrett 1
-
Myford ML4 Identification
Started by:
Steven Volz
in: Manual machine tools
- 4
-
9 October 2026 at 07:32
andrew998
-
Hemholtz coil positioning
Started by:
John Purdy
in: Clocks and Scientific Instruments
- 2
-
9 October 2026 at 04:40
John Purdy
-
Window weights as a source of cast iron.?
Started by:
File Handle
in: Materials
- 19
-
9 October 2026 at 00:49
Nigel Graham 2
-
Reverting An ML7 To Change-Wheels: Any Thoughts??
1
2
3
Started by:
Nigel Graham 2
in: Manual machine tools
- 20
-
9 October 2026 at 00:33
Nigel Graham 2
-
Triangular Insert Tool
Started by:
James A
in: Workshop Tools and Tooling
- 10
-
8 October 2026 at 22:48
Bill Phinn
-
Angled d-bit / machinist reamer?
Started by:
Fulmen
in: Workshop Tools and Tooling
- 6
-
8 October 2026 at 22:41
Bazyle
-
Locomotion No 1 – plans
Started by:
Bob Wild
in: Help and Assistance! (Offered or Wanted)
- 5
-
8 October 2026 at 20:04
Bazyle
-
Tom Senior small vertical head axial play
Started by:
chris1984
in: Manual machine tools
- 3
-
8 October 2026 at 19:34
not done it yet
-
Gears
Started by:
Franco Convertini
in: General Questions
- 8
-
8 October 2026 at 19:07
Howard Lewis
-
Liney RV-2 Rescue
Started by:
JasonB
in: Stationary engines
- 2
-
8 October 2026 at 18:56
JasonB
-
Hello Everyone (New Member Introduction)
Started by:
cedricvale
in: Introduce Yourself – New members start here!
- 5
-
8 October 2026 at 18:47
Howard Lewis
-
Hello everyone
Started by:
andrew998
in: Introduce Yourself – New members start here!
- 4
-
8 October 2026 at 18:43
Howard Lewis
-
Canterbury lamb
Started by:
Michael Callaghan
in: General Questions
- 3
-
8 October 2026 at 17:55
noel shelley
-
Fusion CAD / CAM Problem
Started by:
Shaun Churchill
in: CAD – Technical drawing & design
- 5
-
8 October 2026 at 17:00
andrew998
-
Parkside Electronics
Started by:
Clive Steer
in: General Questions
- 8
-
8 October 2026 at 13:12
shayodon
-
What Did You Do Today 2026
1
2
…
8
9
Started by:
JasonB
in: The Tea Room
- 53
-
8 October 2026 at 11:44
bernard towers
-
Tom Senior small vertical head axial play
Started by:
chris1984
in: Manual machine tools
- 1
-
7 October 2026 at 20:05
chris1984
-
The lazy man’s fly cutter
 Sonic Escape
 Dave Halford
 Russell Eberhardt
 blowlamp
 starjump
 Michael Callaghan
 Dave S
 Dominic Bramley
 Andy Stopford
 Michael Gilligan
 noel shelley
 Andrew Tinsley
 IanT
 mike barrett 1
 Steven Volz
 andrew998
 John Purdy
 File Handle
 Nigel Graham 2
 James A
 Bill Phinn
 Fulmen
 Bazyle
 Bob Wild
 chris1984
 not done it yet
 Franco Convertini
 Howard Lewis
 JasonB
 cedricvale
 Shaun Churchill
 Clive Steer
 shayodon
 bernard towers