
GRAVOGRAPH AF3

GRAVOGRAPH AF3

Home Forums Workshop Tools and Tooling GRAVOGRAPH AF3

Viewing 14 posts - 1 through 14 (of 14 total)
  • Author
    Posts
  • #861893
    Speedy Builder5
    Participant
      @speedybuilder5

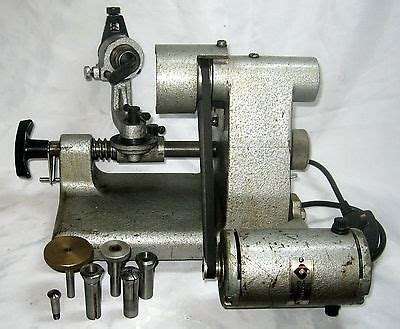
      A bit of an impulse buy at 20€ at local car boot sale.  It looked like a high end drill sharpener, but turns out to be an engraving tool bit sharpener. I only have a single 4mm collet for it, but max diameter through the head may be 9mm.

      Engraving bits don’t seem to have helixes, so perhaps not possible to grind drills on it.

      Any one have knowledge of this machine (Gravograph FRANCE model AF3)  company still in existence and making similar models under a slightly different name. Gravotech.com.

      Bob

      OIP-1186598538

      #861910
      Michael Gilligan
      Participant
        @michaelgilligan61133

        Nice find !!

        .

        Fear not …

        https://www.gravotech.co.uk/about-us/gravograph

        MichaelG.

        #861911
        Michael Gilligan
        Participant
          @michaelgilligan61133
          #862715
          Speedy Builder5
          Participant
            @speedybuilder5

            Thanks for the replies,  I am now continuing the discussion under the posting

            https://www.model-engineer.co.uk/forums/topic/gravograph-af3/

            Bob

            #862725
            Speedy Builder5
            Participant
              @speedybuilder5

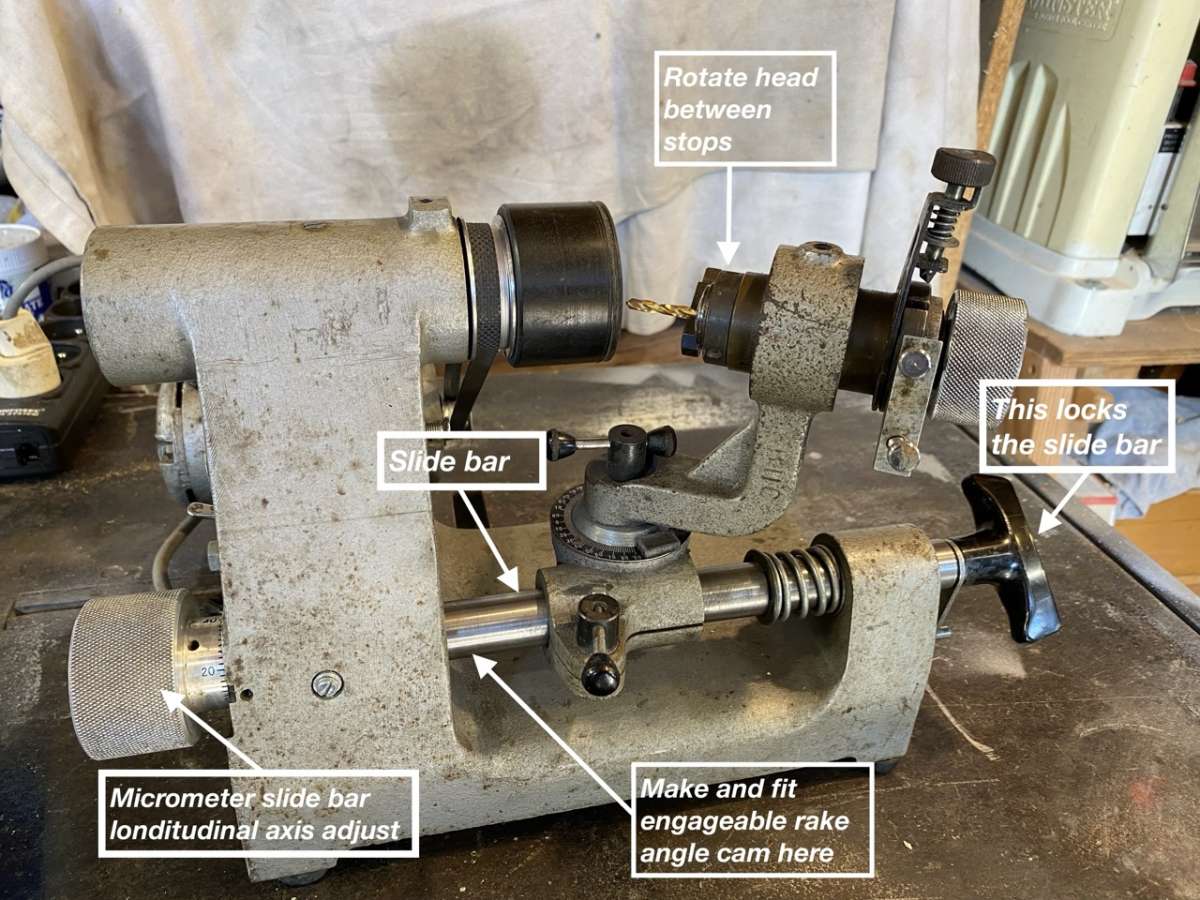
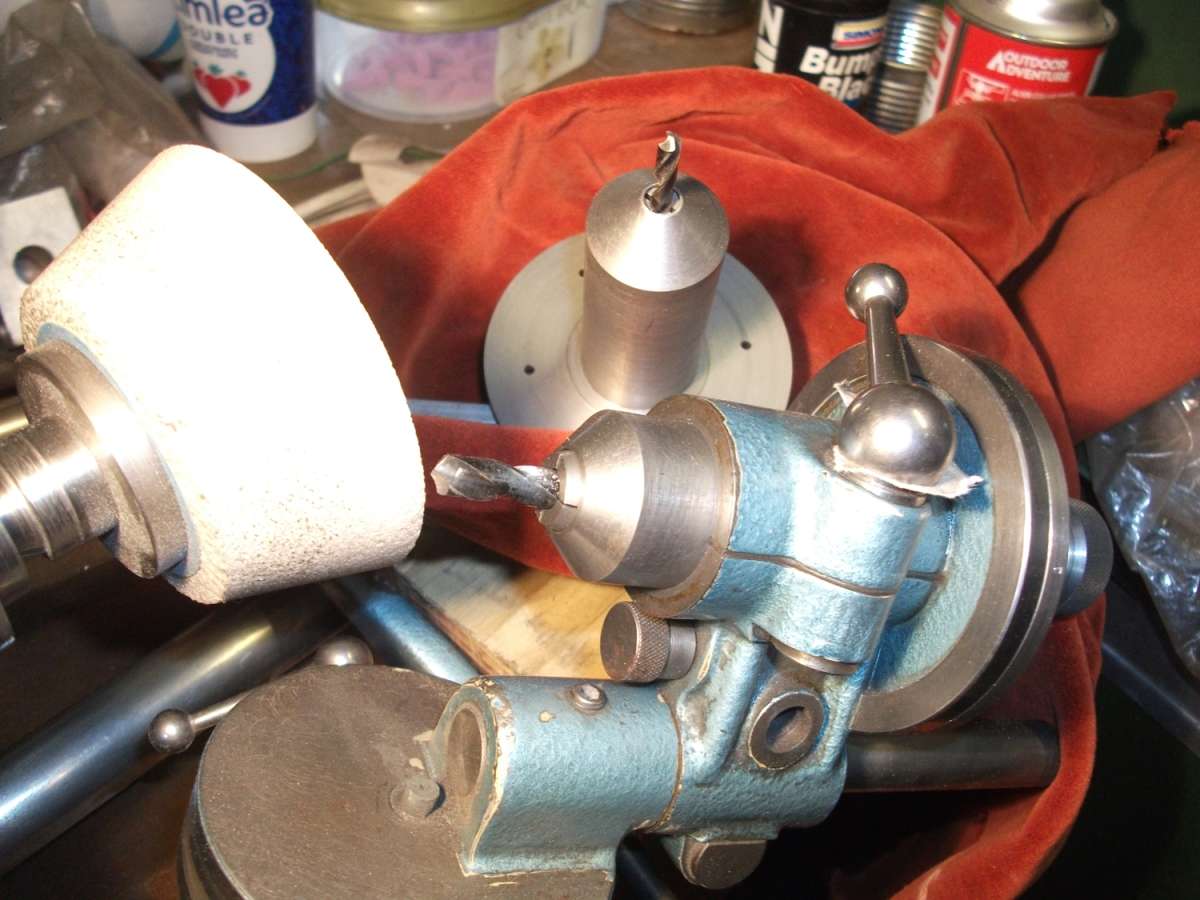
              They say a picture explains all. So my thinking is that the drill bit is brought up to the face of the grinding wheel, and the initial point angle is cut by setting the point angle 118/2 degree and rotating the head, first one flank and then the second.

              Once this is done, the cam would be engaged on the slide bar (Cam not shown in photo as I haven’t made it yet), the handle on the RHS released and the rake angle ground. Note the slide bar is spring loaded and the longitudinal adjustment made via the knob on LH end of slide bar.

              Howard Lewis mentioned a wedge of 31 degrees – would this be the slope of the face of the cam ??

              Open to questions, ideas

              Further explanations

              Bob

              Grinder Mod 1

              #862742
              Bizibilder
              Participant
                @bizibilder

                Have a look at articles and the book (by Professor Chaddock) about the “Quorn Tool and Cutter Grinder”. Your machine is far less complex than a Quorn but drill sharpening would follow the same process.

                #862778
                Paul Lousick
                Participant
                  @paullousick59116

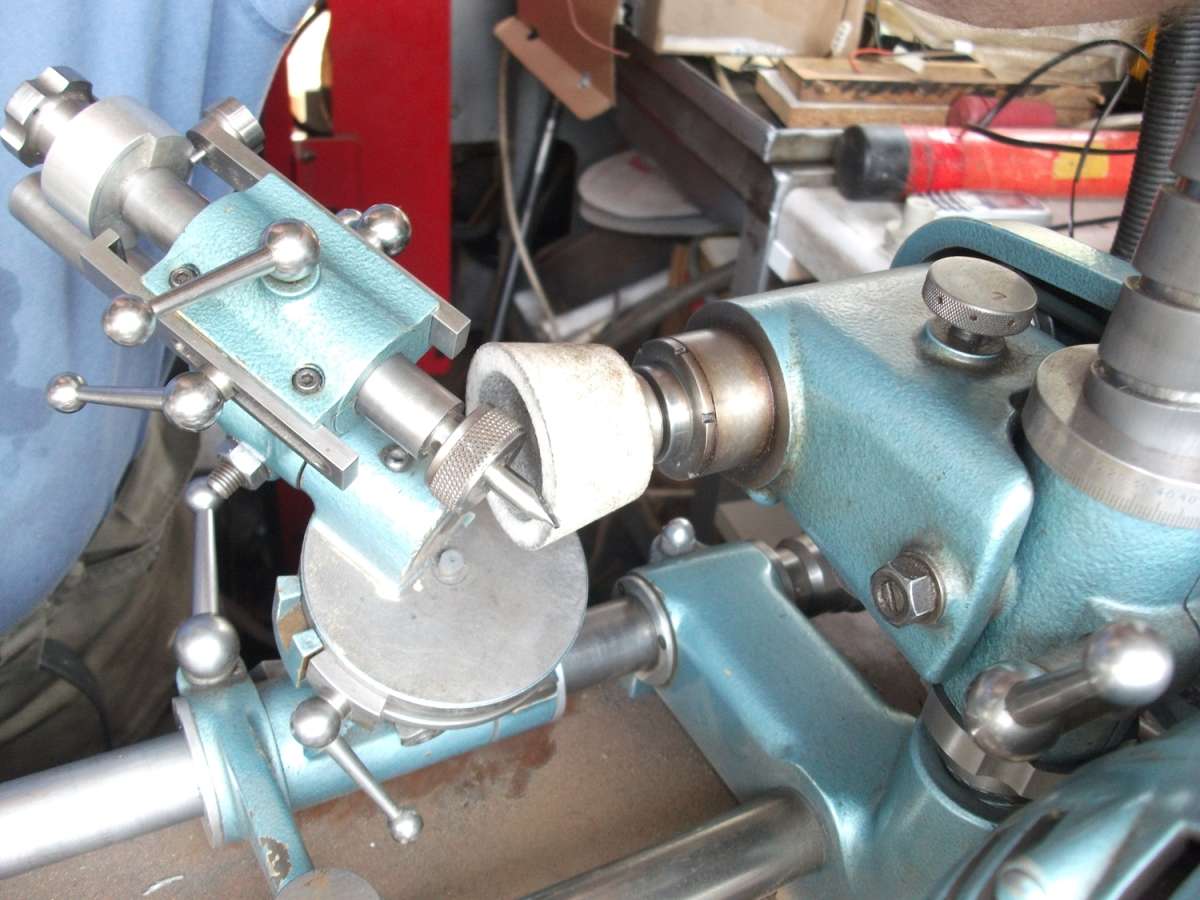
                  Your machine is like a small Deckel, D-bit grinder. Lots of information on Youtube, like this one by Stefan Gotteswinter explaining 4 facet drill grinding..

                  https://www.youtube.com/watch?v=I5b6h1Vddes

                  #862783
                  renardiere7
                  Participant
                    @renardiere7

                    You can’t use that Gravograph grinder for 4 facet grinding. The angle of the toolholder to the upright is fixed, it needs to be adjustable.

                    #862793
                    Howard Lewis
                    Participant
                      @howardlewis46836

                      Bob,

                      You have PMs.

                      On your machine, you would set the drill with the lip horizontal, and then swivel the holder by 59 degrees to the wheel, to produce the 118 degree point angle.

                      The problem is going to be to raise the drill by 30 degrees for the secondary clearance, and then for the 10 primary clearance angle.

                      To do this the collet holding the drill needs to be set at those angles.  Maybe, by setting the rotational stops  some form of clearance can be set..

                      This will produce clearance angles, but I am not sure that they would be parallel to the cutting edge of the lip. So possibly not a four facet grind as we normally know it.

                      To produce equal length lips the in feed will need to set carefully each time, to the same micrometer setting, to ensure that the drill will give a hole that is accurately sized.

                      I can only suggest a “suck it and see” approach.

                      You may end up with a drill which has clearance, and cuts, but not a four facet ground one.

                      Howard

                      e


                      #862934
                      Howard Lewis
                      Participant
                        @howardlewis46836

                        Got that wrong!

                        Set at 31 degrees to the wheel, for a 118 degree point angle. 59 is the angle of metal left to grind.

                        Howard

                        #862964
                        John P
                        Participant
                          @johnp77052

                          cone relief


                          Looking at the picture diagram of your intended drill grinding, the
                          drill is set up relative to the grinding wheel the cam that you
                          propose on the slide bar would just advance
                          the drill towards the grinding wheel and just make it shorter.

                          There is some provision made on the Quorn to regrind
                          broken centre drills and is refered to in his book on the Quorn
                          on page 117 ,the photo seen here is almost identical the the
                          photo in the book in fig 92 and only works because the grinding
                          is not all the way to the centre of the work.The new tip is not
                          ground but emerges as the larger cone is ground back to form
                          a new cutting edge ,the new tip needs to be re ground i use a
                          4 facet form. As you can see in the photo the cam is on the
                          work shaft as the drill rotates it moves forward into the grinding
                          wheel

                          D H Chaddock in his book on the Quorn states the normal
                          drill grinding can not be done and recommends using the
                          4 facet method .Seen here in the photo the base is set to
                          31 deg ,the drill is pointing up at 10 deg for the initial grind
                          and set at 25 deg up and ground until the lines intersect
                          at the point.

                          I think you would have to make similar type of work holding
                          base to the Quorn to be able to do what you want.

                          John

                          4f (1)

                          #863030
                          Howard Lewis
                          Participant
                            @howardlewis46836

                            I suspect that the Gravograph AF3 may be a high precision machine version of the Reliance or Picador attachments for bench grinders, and would grind drills with an arctuate clearance , rather than four facets. (Possibly predating four facet drill grinding), like jobber drills.

                            Without having the machine in front of us, it is impossible to know (unless someone tells / shows us)  just what movements are possible, and therefore just how to set it up.

                            Another problem is the few collets that came with it, so the solution may be to make up a adptor to use ER 20 collets for drill holding.

                            This would allow drills of almost any size from 1mm to 13 mm to be held for grinding.

                            It will be intersting to see what Bob comes up with eventually.

                            Howard

                            e

                            #863041
                            Speedy Builder5
                            Participant
                              @speedybuilder5

                              Problem with collets is that standard collets for the machine only go up to 9mm in diameter.  I could make an attachment like the one shown in this link-

                              https://www.hobby-machinist.com/threads/twist-drill-sharpening-on-a-deckel-s0-dbit-grinder.107486/

                              I have a copy of a similar design (Luc Wybo)

                              https://www.youtube.com/watch?v=BU8r43QoMms

                              However the project is stalling for a bit as something else has cropped up – as it always does!  I will still follow this link and thanks to all who have contributed.

                              Bob


                              #864093
                              John P
                              Participant
                                @johnp77052

                                Further to the references about conical drill grinding on the Quorn
                                grinder .
                                This may be of interest and you will most likely have to register
                                to be able to view these files on

                                https://groups.io/g/Quorn-Owners

                                Select Files

                                scroll down to Analytical methods by J. Hugel

                                scroll down again to Six Step CF -23 PDF
                                conical drill grind

                                and this explains how to grind drills.

                                John

                              Viewing 14 posts - 1 through 14 (of 14 total)
                              • Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.

                              Latest Replies

                              Viewing 25 topics - 1 through 25 (of 25 total)
                              Viewing 25 topics - 1 through 25 (of 25 total)

                              View full reply list.