
Cross Drilling Jigs

Cross Drilling Jigs

Home › Forums › Workshop Tools and Tooling › Cross Drilling Jigs

Viewing 15 posts - 1 through 15 (of 15 total)
  • Author
    Posts
  • #867806
    peak4
    Participant
      @peak4

      I was originally going to add these photos to a different thread, but thought they might be better on their own for future reference and searches.

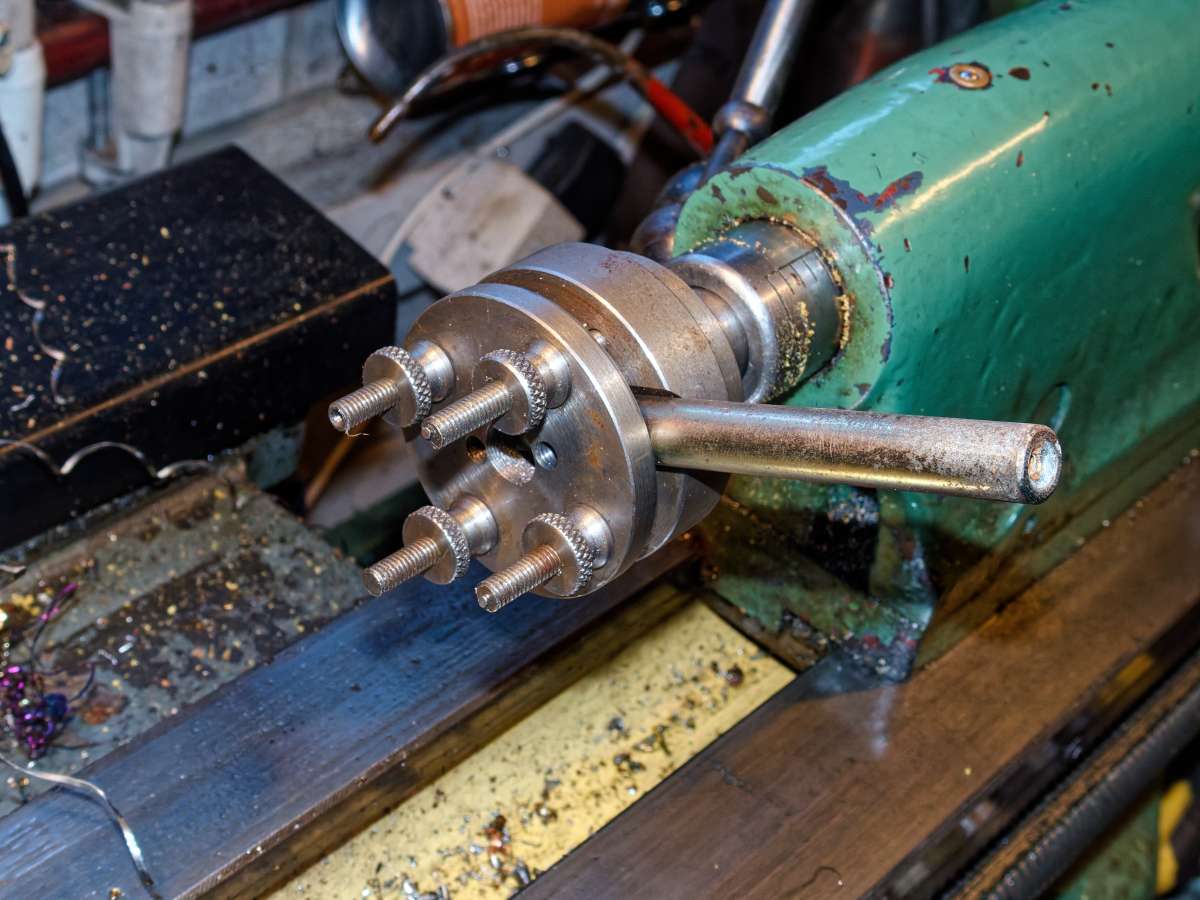
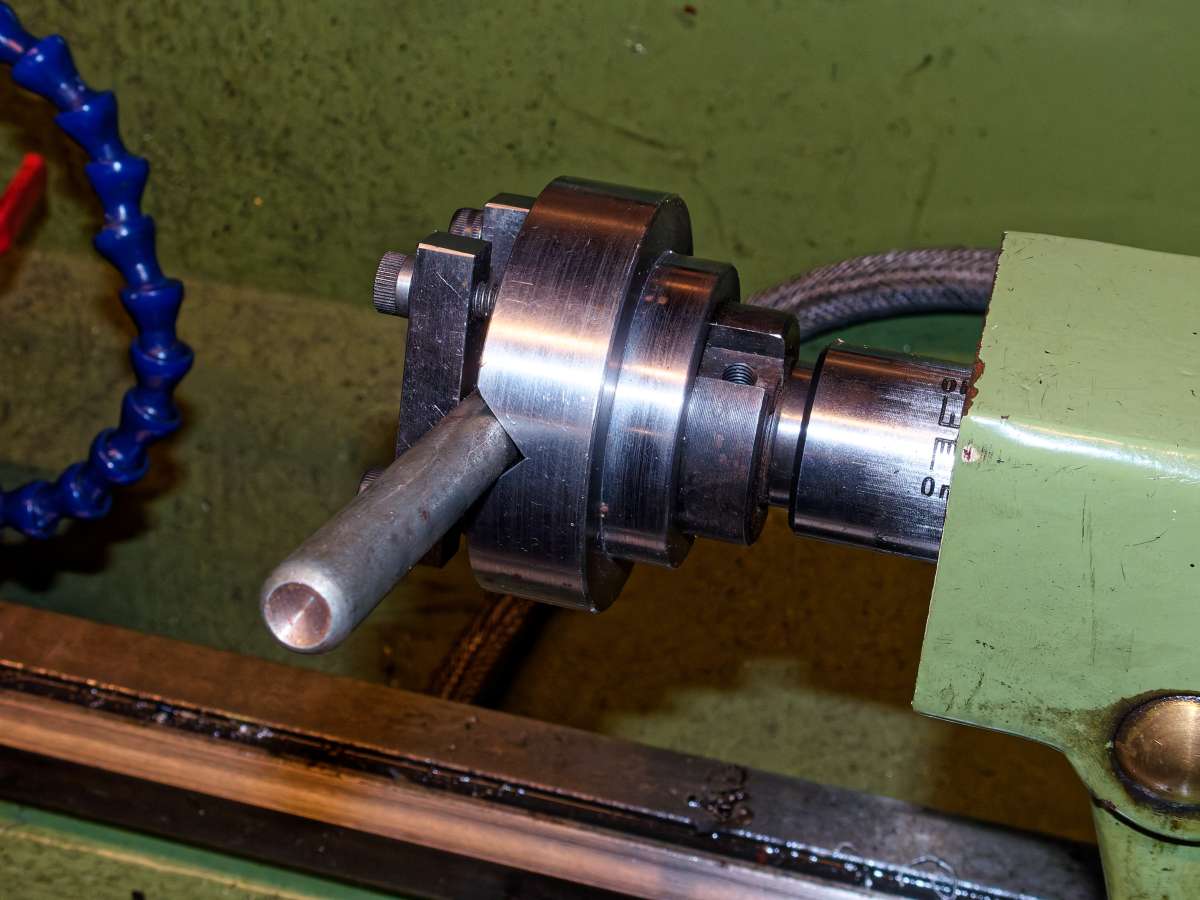
      These are a couple of examples of tailstock cross drilling jigs; they both appear to be home workshop made, and were bought second hand by me some time ago.
      I’ve never seen any commercial ones in the UK, though there are a few designs floating around; I believe someone does sell them; I think in Australia.

      An MT2 one in the Warco 720 (Myford S7B clone)
      SA030017_DxO-Small

      And its larger MT3 cousin inn the Warco GH1330
      SA030016_DxO-Small

      Their use is largely self explanatory.

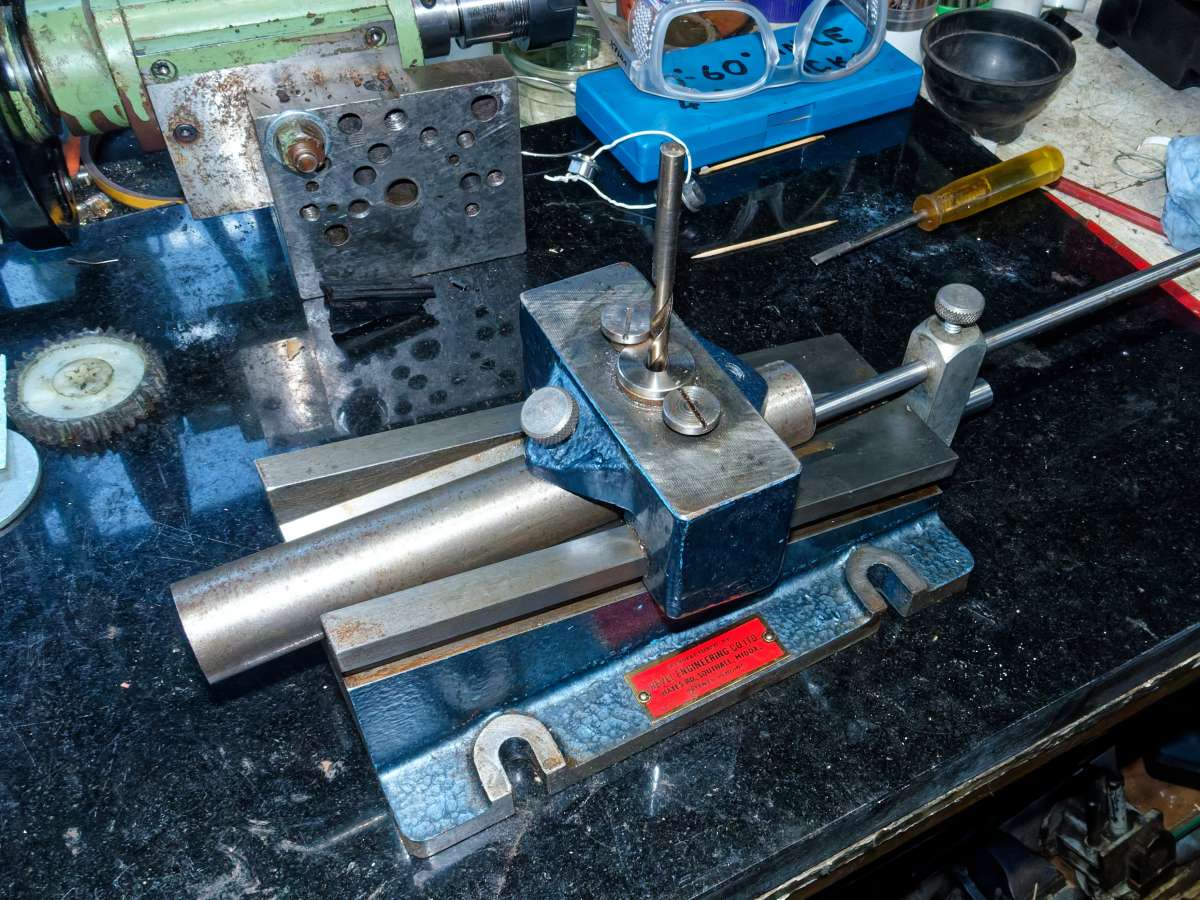
      This one is a bit more oddball, and very nicely made.
      I’ve never seen one similar.

      SA030020_DxO-Small

      The rising saddle holds a guide bush and also clamps the workpiece down; there’s a hidden thumbscrew on the back side to clamp the saddle onto the base.
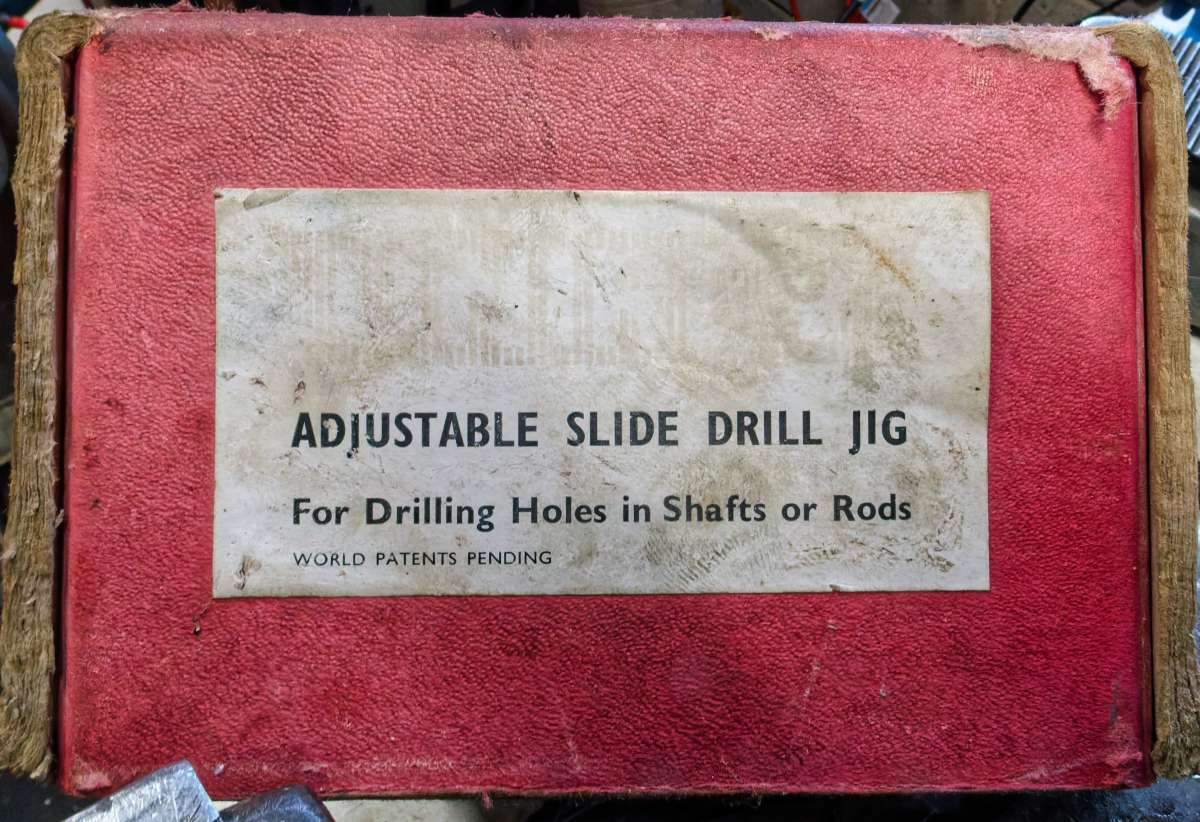
      It came in a box, as below;

      SA030023_DxO-Small

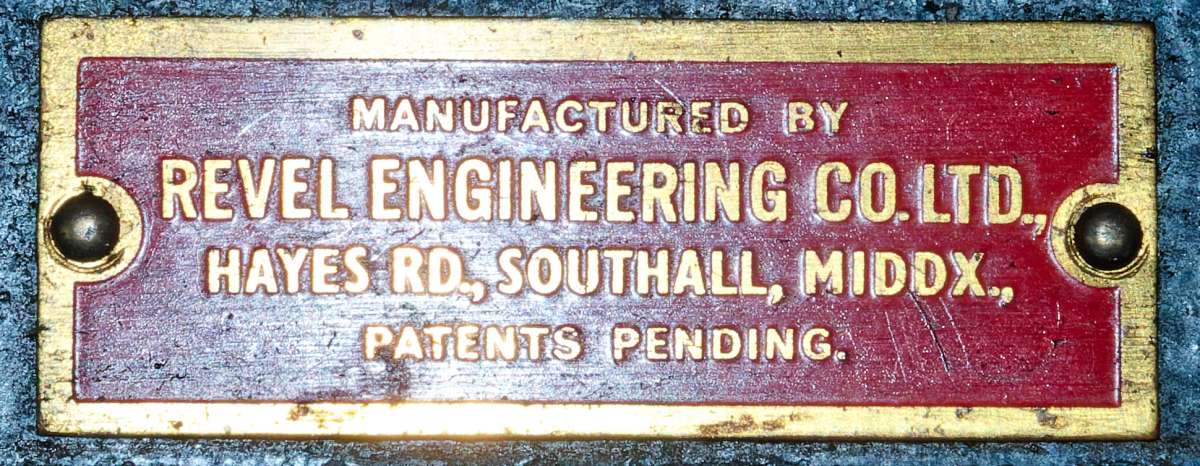
      with a nameplate on the jig

      SA030021_DxO-Small

      Bill

      #867831
      Pete
      Participant
        @pete41194

        I wouldn’t know about the UK or even the rest of the world Bill. But there were a few North American lathe brands who offered them as tail stock accessories, and at least a few tool manufacturer’s who commercially manufactured what seem to be called Crotch Centers for cross drilling shafts here in North America. South Bend I know for sure were offering them. I may have not noticed, but any old catalog engravings or pictures I’ve seen didn’t seem to have any method of clamping the shaft as your first and second pictures show. An error in design ? For all I know, those Crotch Centers may still even be available somewhere.

        That Revel Engineering jig is not one I’ve ever seen. I’m suitably envious. 🙂

        For the size of work most of us might need an accurate cross drilling jig for use with a hand or pillar drill, Hemingway seem to no longer offer the Machinist’s Finger Plate jig G. Thomas shows in his M.E. Workshop book that they once did. I recall Mr. Thomas did give credit for the original design to an older article in the M.E. magazine by a Commander W. T. Barker. Google says his finger plate design is in the 1951, issue 2596, page 268 M.E. magazine for anyone who might have access to it. Fwiw, Cdr. Barker was also quite a famous M.E. who built beautifully detailed and highly complex marine engine scale models.

        If it might help anyone here, Clickspring I thought did a very good two part video series of basically making the same as Mr. Thomas did.

        Part 1 https://www.youtube.com/watch?v=FgBM-JVRWgU&t=85s

        Part 2 https://www.youtube.com/watch?v=F5T0WenjIwA

        The same was detailed in Guy Lautard’s first Machinist Bedside Reader book that’s now out of print. However the main base plate overall dimensions seem to be hard to find without his book. 1″ x 3″ x 3″. The rest should be easy enough to scale from that should anyone want to build their own version.


        #867841
        Michael Gilligan
        Participant
          @michaelgilligan61133

          The Canadian version of Mr Revel’s patent is nicely formatted for legibility.

          MichaelG.

          .

          https://worldwide.espacenet.com/patent/search?q=pn%3DCA661633A

          #867844
          Pete
          Participant
            @pete41194

            Thanks for the link Michael. 👍

            #867845
            DC31k
            Participant
              @dc31k
              #867852
              JasonB
              Moderator
                @jasonb

                A few things that have put me off such tailstock jigs, maybe those who use them can show how their jig will do the things that put me off.

                1. Drilling holes in short small diameter items, lets say 1/2″ long x 1/8″ dia though I often have a need for 1/4 long”

                2. How do you position the hole a set distance from the end or even see to locate as scribed mark on th eclampe equiped ones, again on small items but could apply to large.

                3. What do you do with the tailstock ones if you need more than one hole as the work is likely to rotate as you reposition it after drilling the first.

                4 Related to the first these short items often take the form of a headed pin so won’t lay in a Vee.

                With so many more people having mills these days I see less need for them than maybe 50yrs ago when the lathe may have been the only machine in the workshop.

                Typical use, hole for 0.5mm split pin though 0.8mm hole is more common.


                #867856
                Bo’sun
                Participant
                  @bosun58570

                  I bought one from ARC a few years ago to do a specific job before I bought a milling machine.  It worked perfectly, but I’ve only used it a couple of times since.  I echo Jason’s sentiments about it’s limitations, and go to the mill for such jobs now.

                  #867871
                  peak4
                  Participant
                    @peak4
                    #867874
                    peak4
                    Participant
                      @peak4

                      Another long post gone; I give up
                      I made the mistake of submitting before copying the content once again.


                      #867877
                      Andrew Tinsley
                      Participant
                        @andrewtinsley63637

                        I too, have the Arc Euro version. I use it in preference to the mill as it is simply quick and handy. I don’t do very small stuff or multiple holes, so Jason’s objections don’t apply.

                        Andrew.

                        #867880
                        Michael Gilligan
                        Participant
                          @michaelgilligan61133
                          #867887
                          Michael Gilligan
                          Participant
                            @michaelgilligan61133

                            IMG_2114

                            #867894
                            Michael Gilligan
                            Participant
                              @michaelgilligan61133

                              See #867492

                              #867922
                              DC31k
                              Participant
                                @dc31k

                                Glad it is not just me whose posts are disappearing.

                                Above, I wished to say that Guy Lautard’s first bedside reader is back in print as of this date.

                                This is verifiable by going to the author’s own website or to Amazon thorugh which the book is available.

                                #867959
                                Nigel Graham 2
                                Participant
                                  @nigelgraham2

                                  Jason –

                                  Your Question(1)…

                                  Having recently carried out something similar albeit not needing high accuracy, and doing the drilling on the bench-drill with a table slot as “Vee-block”, I made the cross-hole while the material was still a length of rod.

                                  So no need to try to cross-drill something hard to hold such as a thin slice or (as with your pins and with the pipe plugs I made) a part with two diameters.

                                  I was making a pair of plugs resembling stocky clevis pins, so for efficiency faced both ends of the stock bar (‘Nylon’, about a foot long), cross-drilled both ends spaced from a simple stop-block, then completed the turning.


                                  A couple of other ideas:

                                  On Q.2: assuming the distance between the axis and the end of the Vee is known, measure to the end of the part from the latter. Perhaps worth making a basic end-stop for the holder, the stop part itself being a screw and lock-nut.

                                  On Q.3, a pin with a faced end through the first hole might give that parallel alignment to sufficient truth, if of a close sliding fit in the hole and a diameter allowing it to contact both walls of the valley.


                                Viewing 15 posts - 1 through 15 (of 15 total)
                                • Please log in to reply to this topic. Registering is free and easy using the links on the menu at the top of this page.

                                Latest Replies

                                Viewing 25 topics - 1 through 25 (of 25 total)
                                Viewing 25 topics - 1 through 25 (of 25 total)

                                View full reply list.